

Deburring
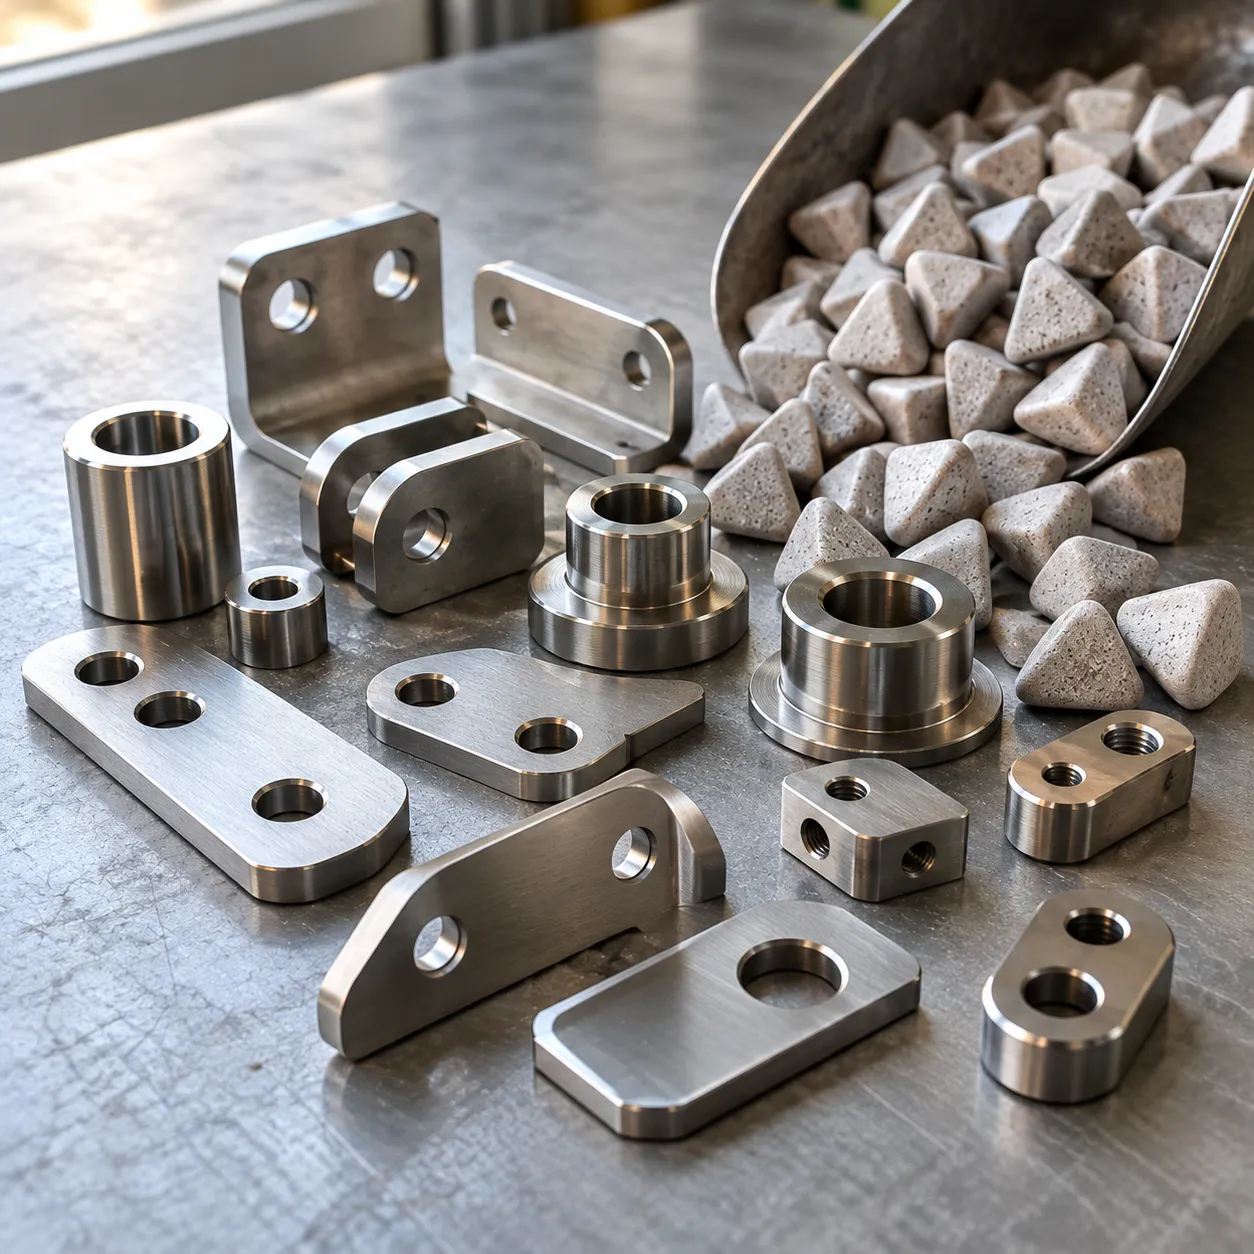
Burrs and sharp slivers left by machining, stamping or casting are worn away evenly, so parts are safe to handle and ready for assembly or plating.
Burrs and rough edges on production runs of small parts don't have to stay that way. Our Oceanside shop smooths them by the batch, and production parts from Stanton reach us by mail after a free written quote.
Production runs of small parts deserve a careful finish
Burrs are small, sharp and annoying. They scratch mating parts, snag gloves and cause problems at assembly. Tumbling wears them away evenly across a whole batch, so parts from Stanton or Garden Grove arrive on your bench ready to use.
We pick media that suits the metal and the size of any holes, run the load, then rinse and dry it so there are no water spots. Steel gets dried fast so it doesn't flash rust, and every batch is checked for stuck media before packing.
If your production runs of small parts have tight fits, tell us before we quote. Tumbling takes off very little metal, but it does round corners a bit, and we want to plan around anything that has to stay exact.
Not sure which finish your parts need? Send photos, a part count and what the parts are used for. We will suggest a finish, run a few samples if needed, and send back a written quote.
Pick one finish or combine a few. We often smooth first, then burnish or age the piece, and we plan the steps around the production runs of small parts you ship from Stanton.
Burrs and sharp slivers left by machining, stamping or casting are worn away evenly, so parts are safe to handle and ready for assembly or plating.
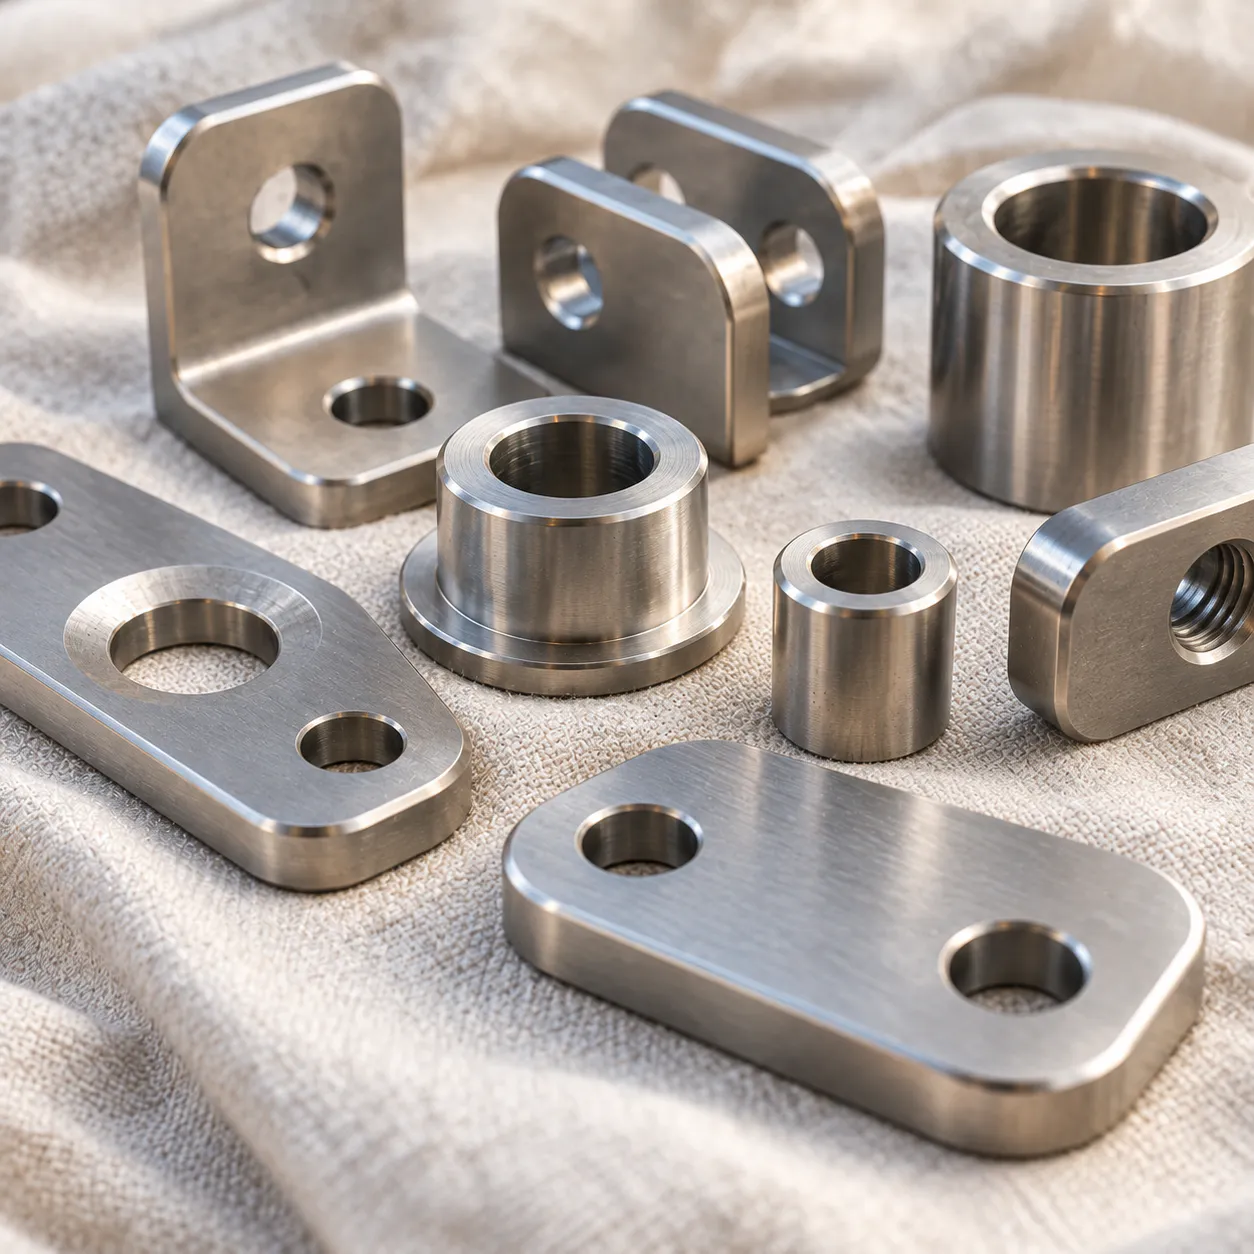
Sharp corners are gently rounded and tool marks are softened. Parts feel better in the hand and plating covers edges more evenly.
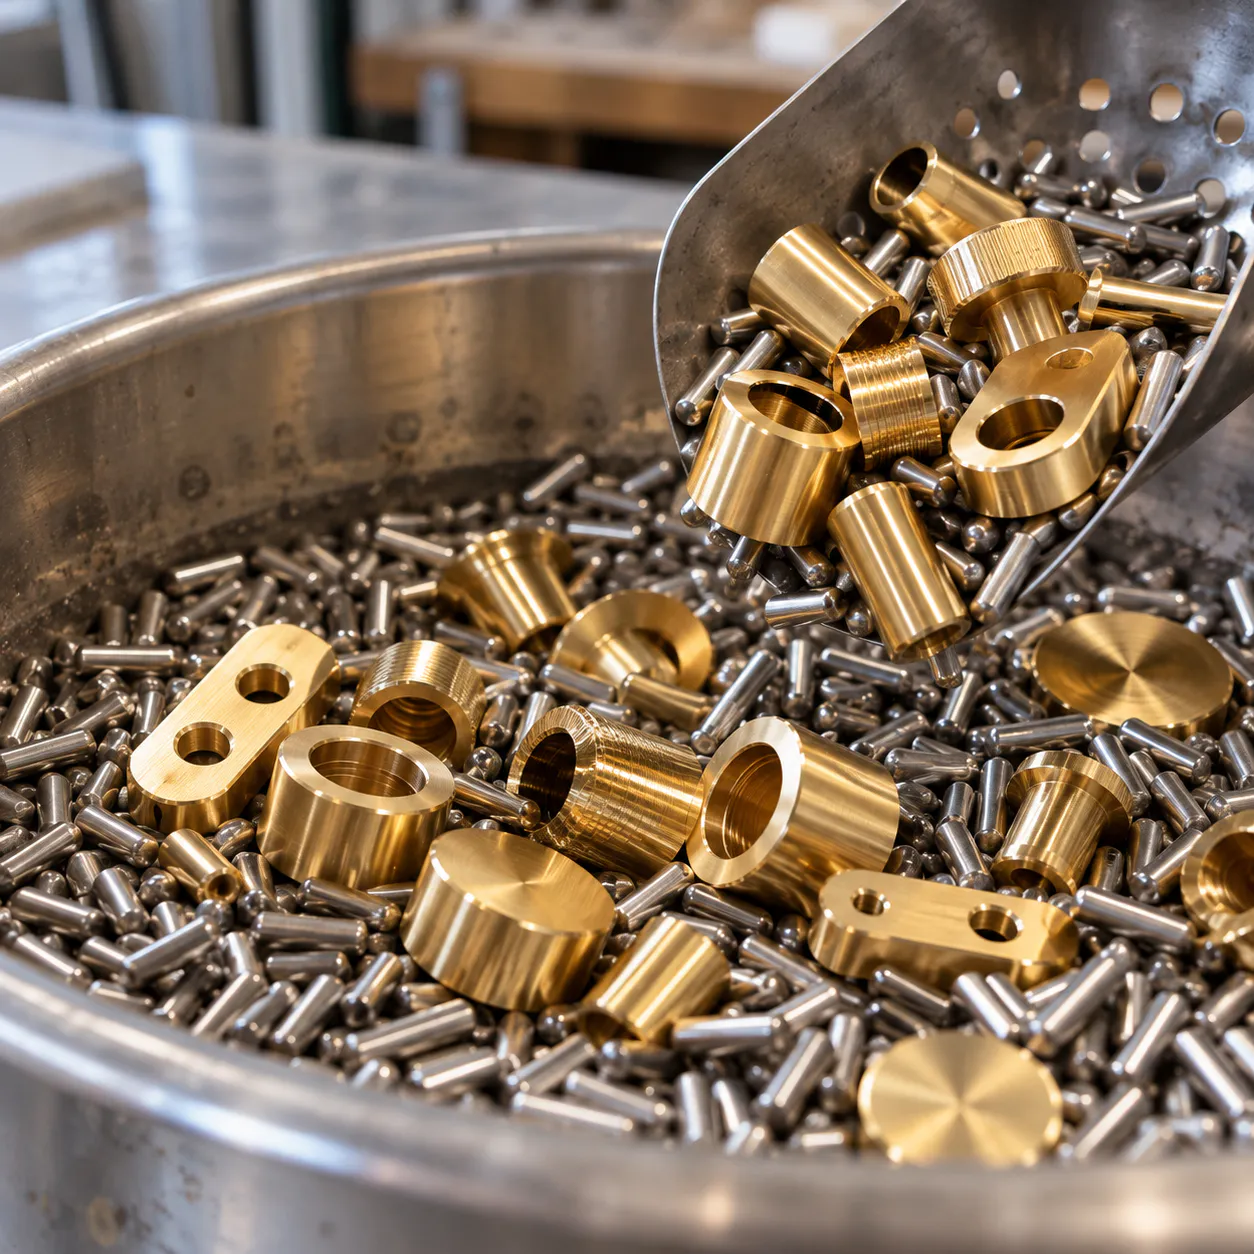
Steel media presses the surface smooth instead of cutting it, bringing up a bright, clean shine on brass, copper and steel without buffing each piece.
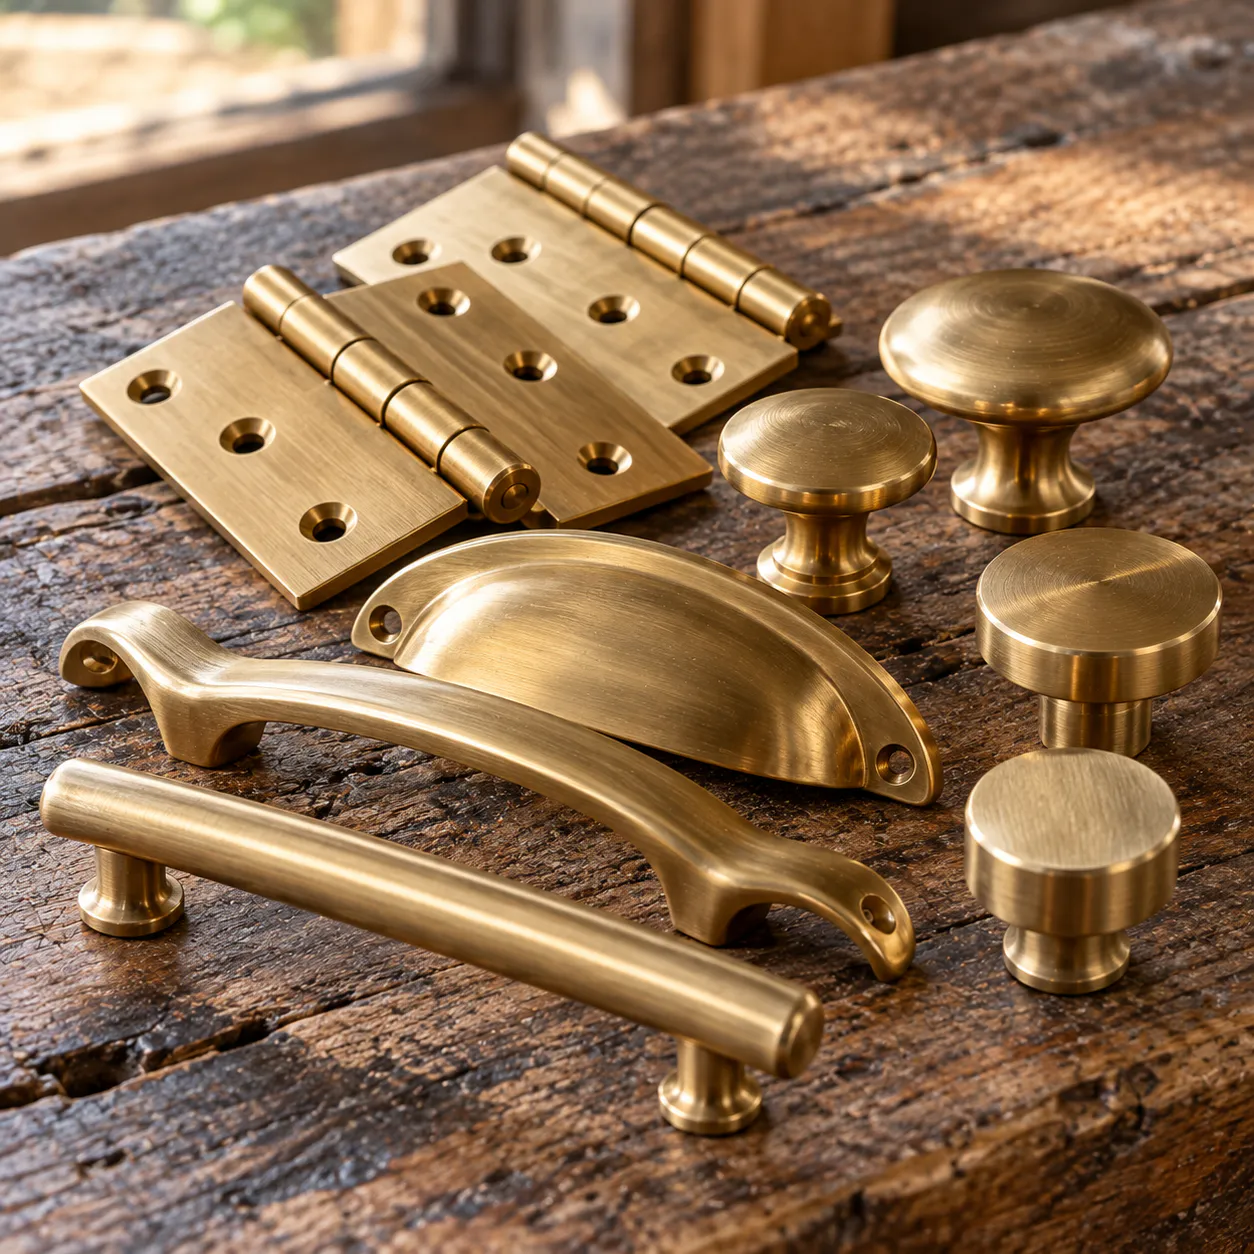
A soft satin surface with worn, rounded edges that looks naturally aged. Popular on brass hinges, pulls, knobs and small decorative castings.
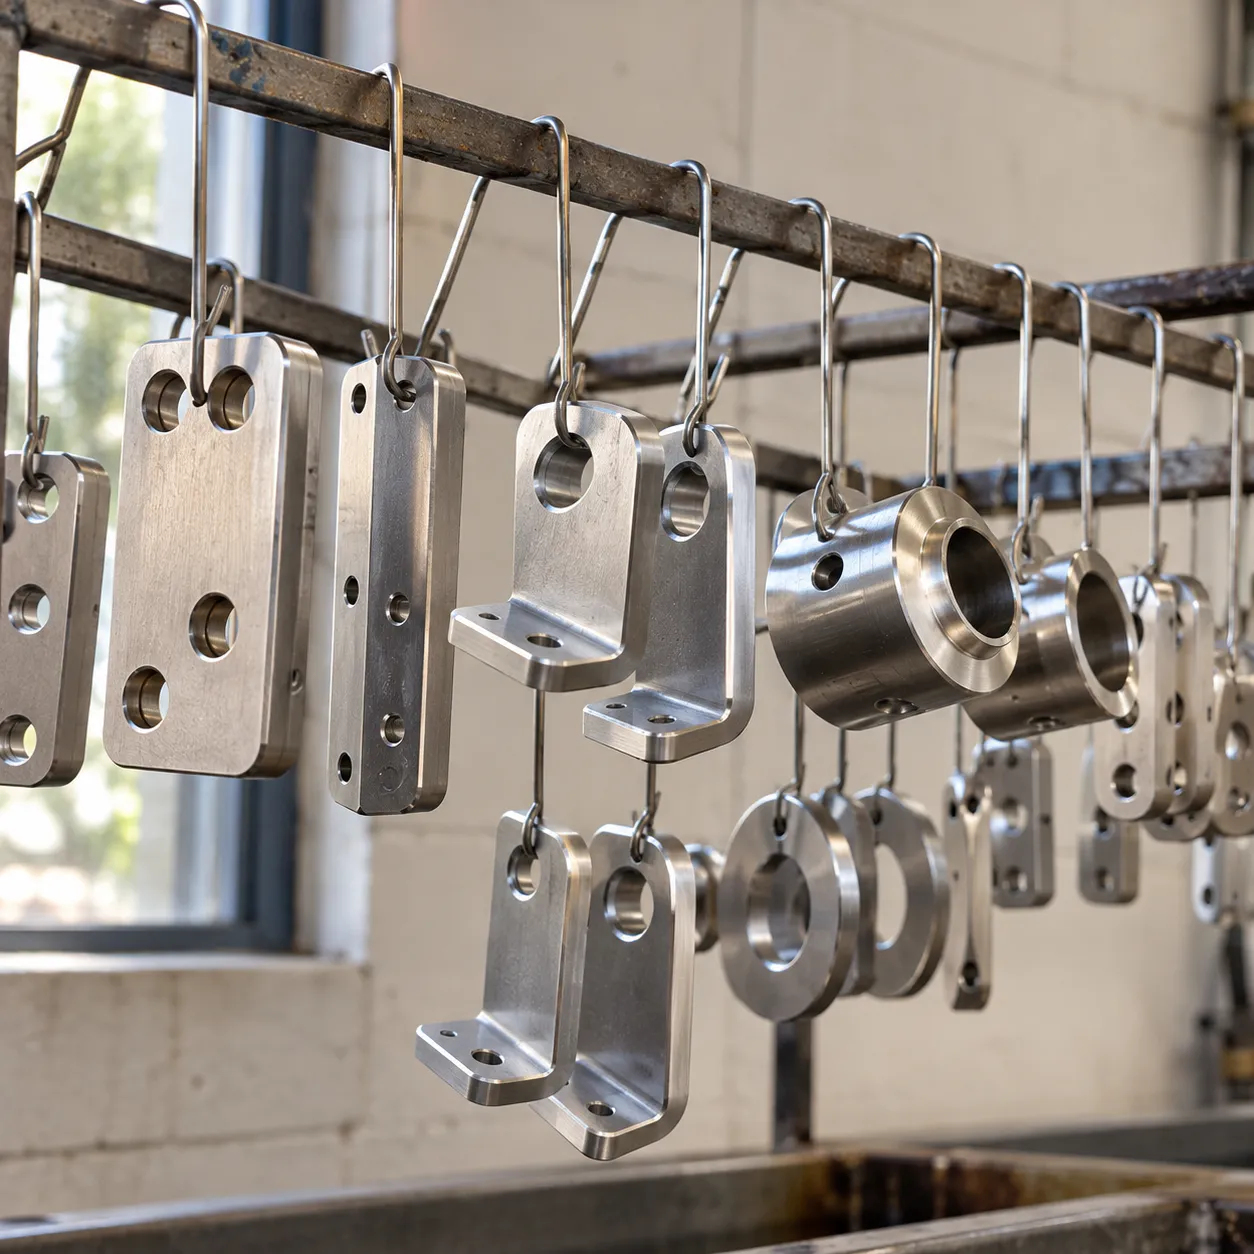
Tumbling first removes scale, light rust and surface marks, so copper, nickel or chrome goes on smoother and the finish looks better for less cost.
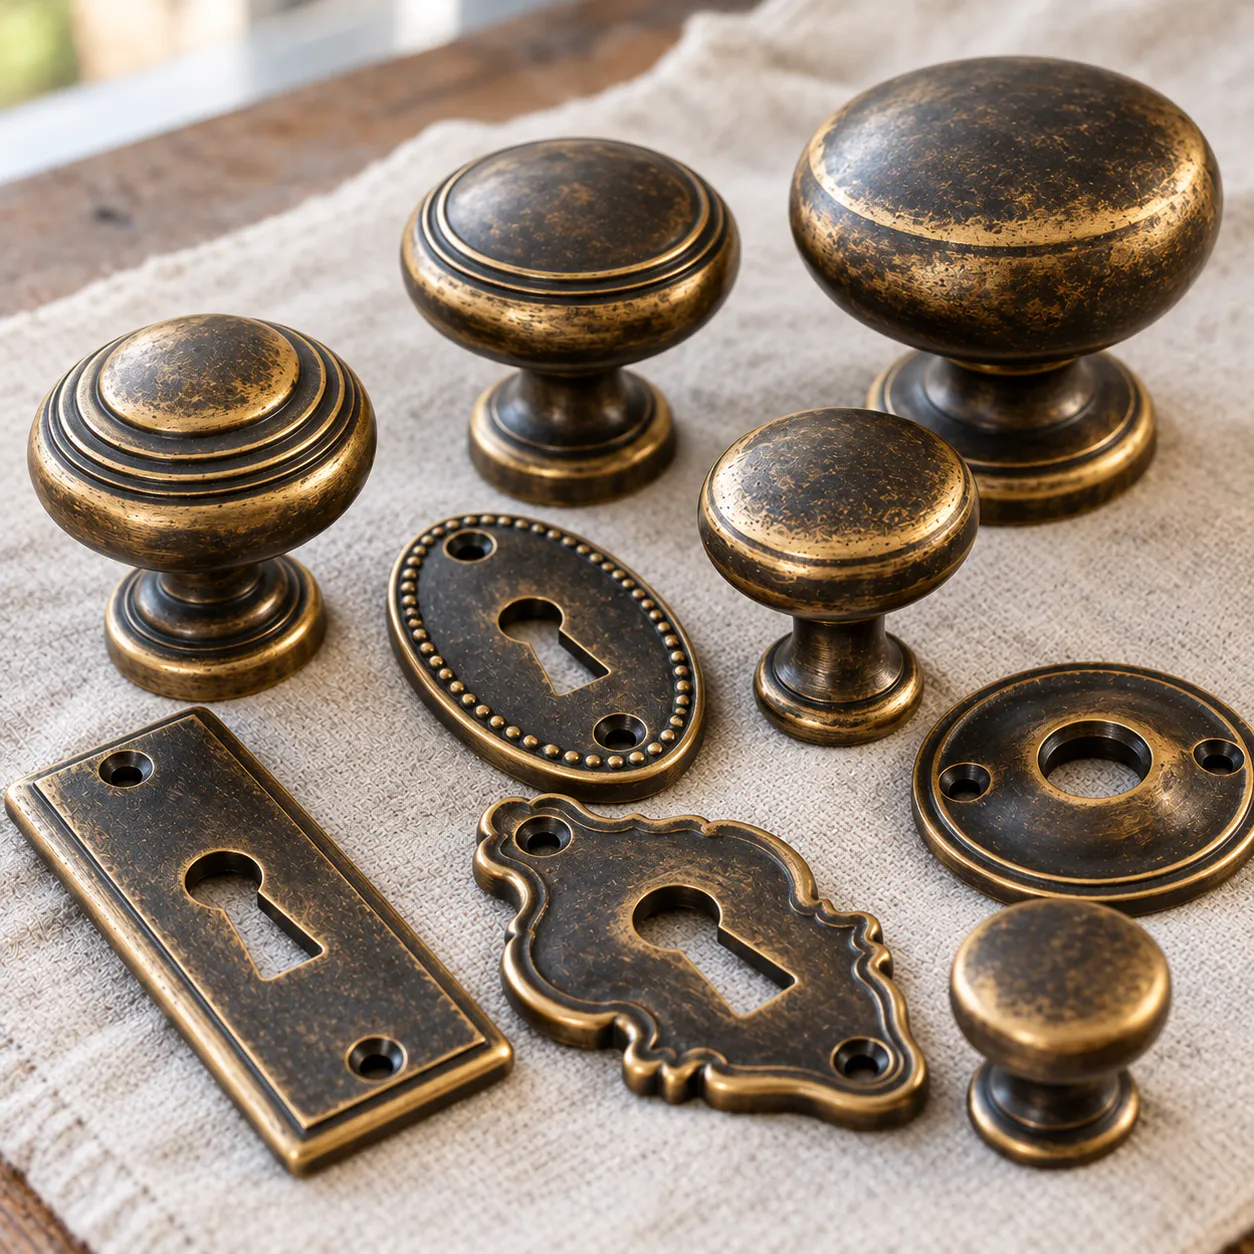
Plated or darkened parts are tumbled lightly so the high points wear through and glow, giving hardware a used, lived in character.
Drag the handle across each photo to see parts as they went into the tumbler and as they came out.
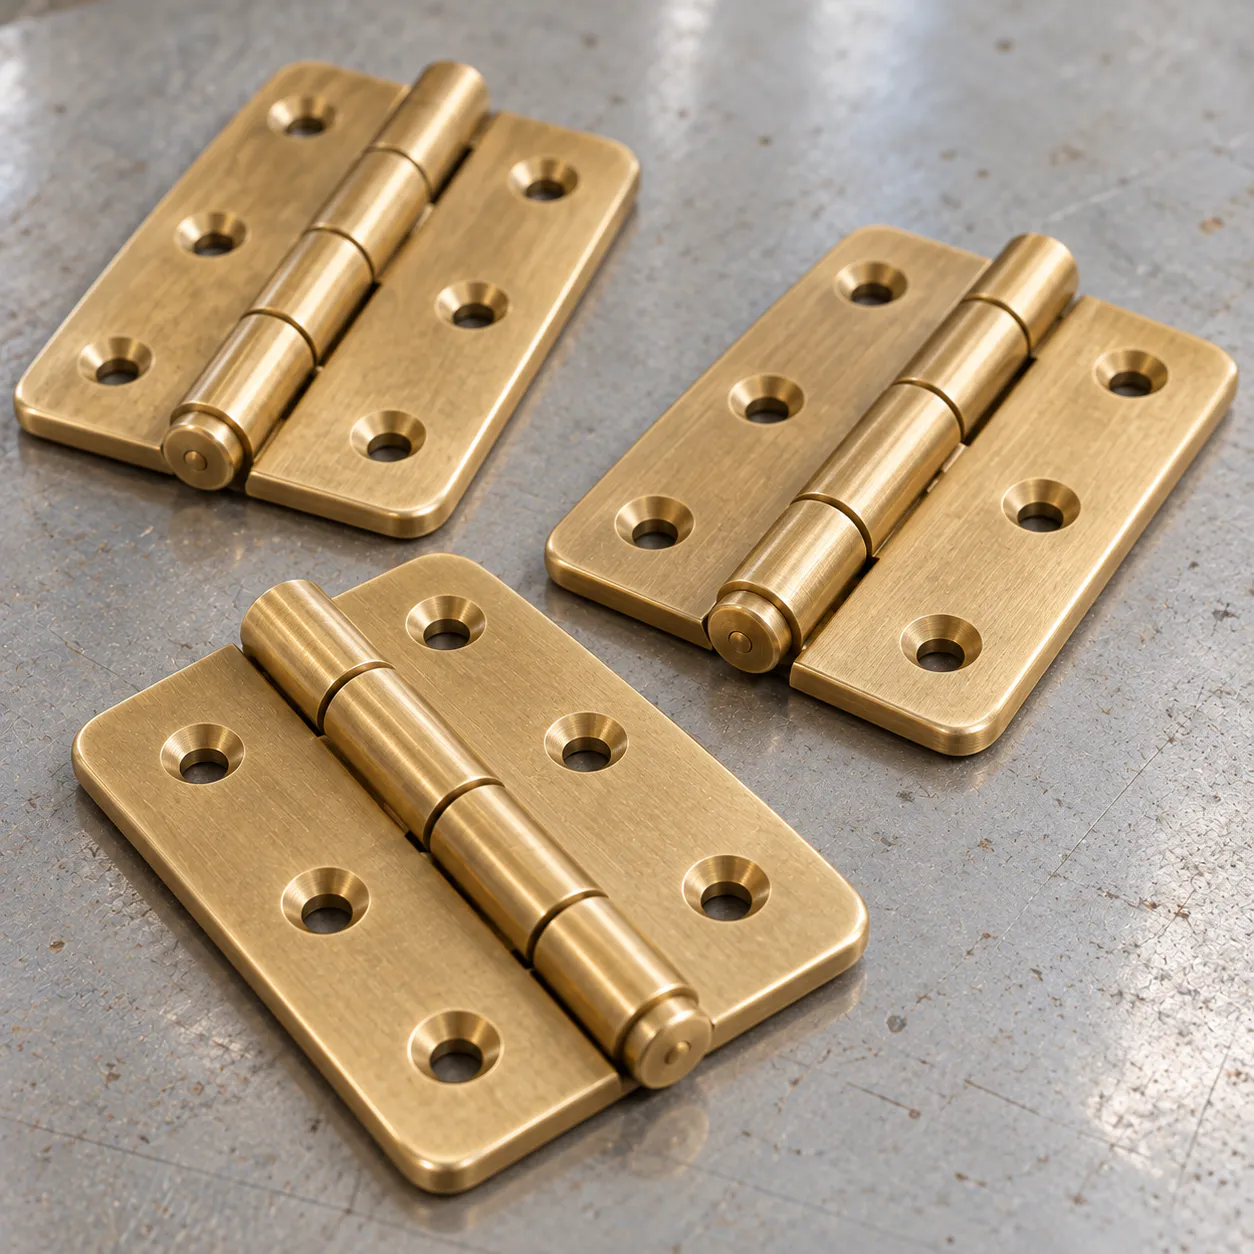
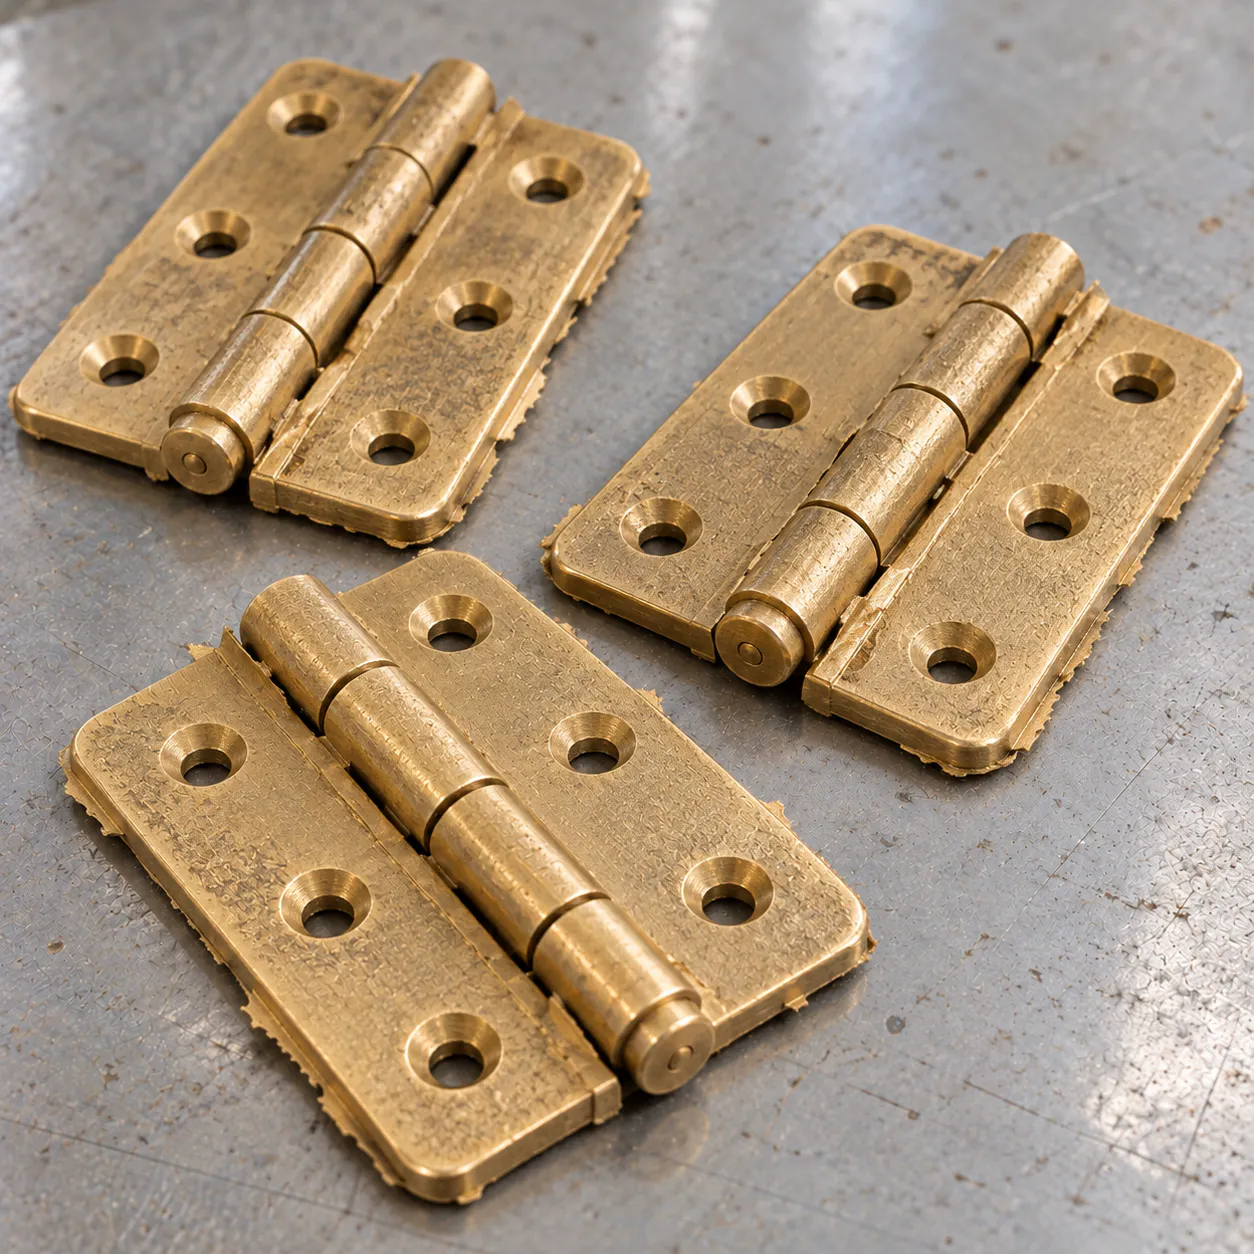 Before
Rough castings with parting lines and a dull, uneven skin. Tumbled in stages to smooth the surface and soften the edges into an even satin glow.
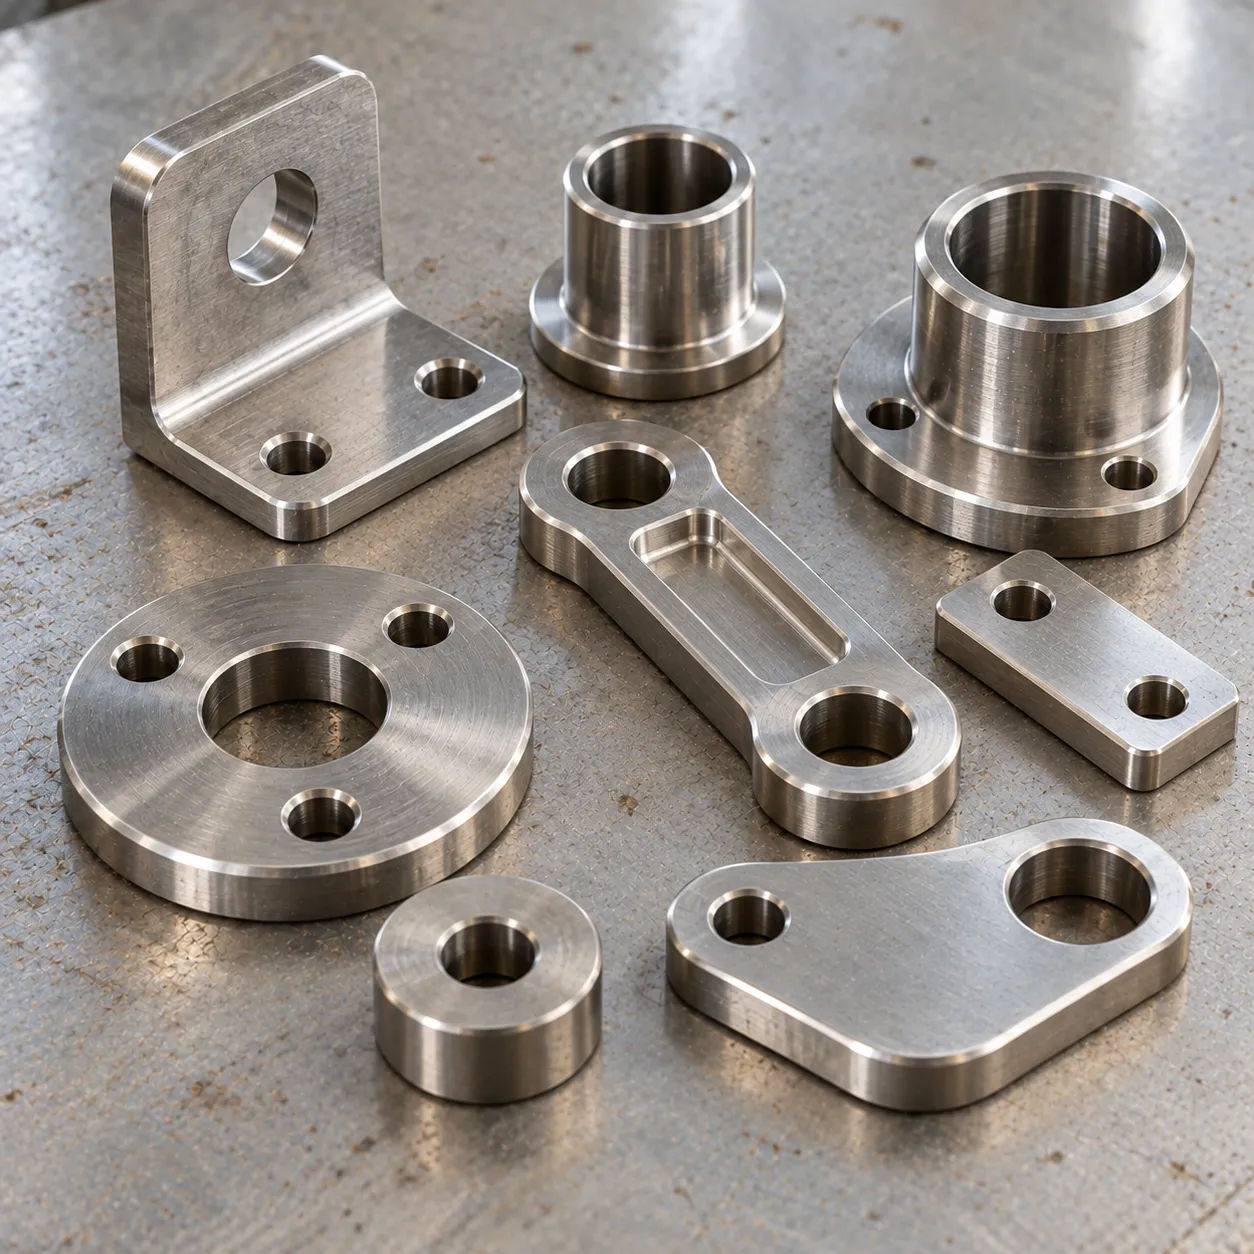
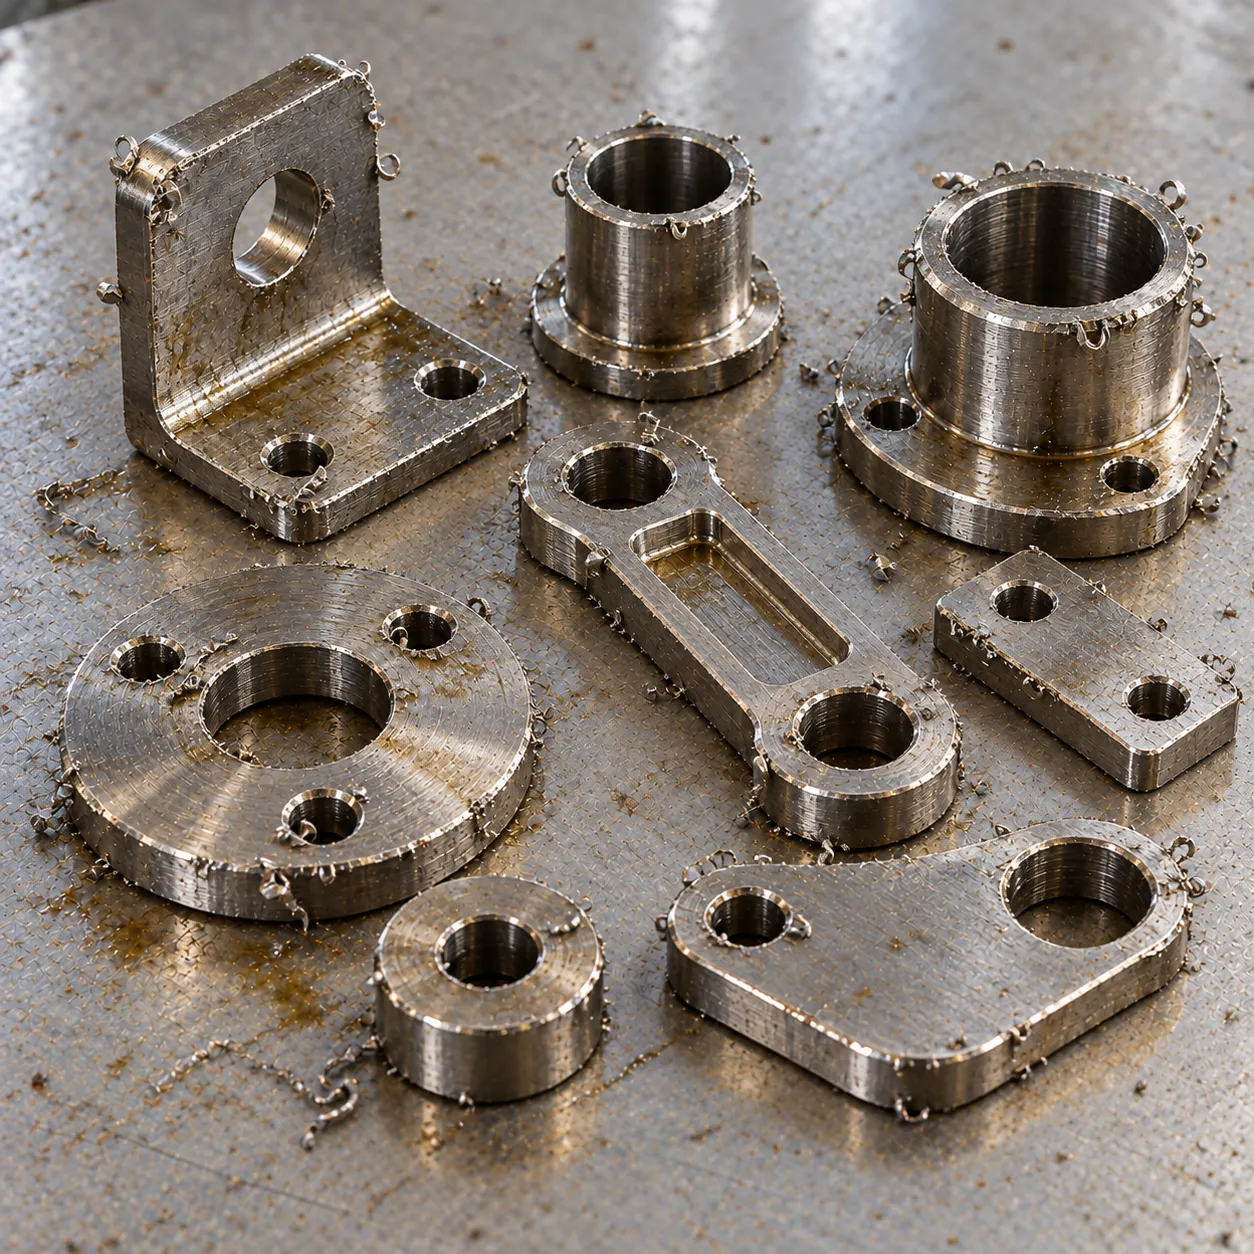 Before
Fresh off the machine with burrs, sharp corners and cutting oil. Deburred, edge smoothed and dried spot free, ready to go straight to plating.
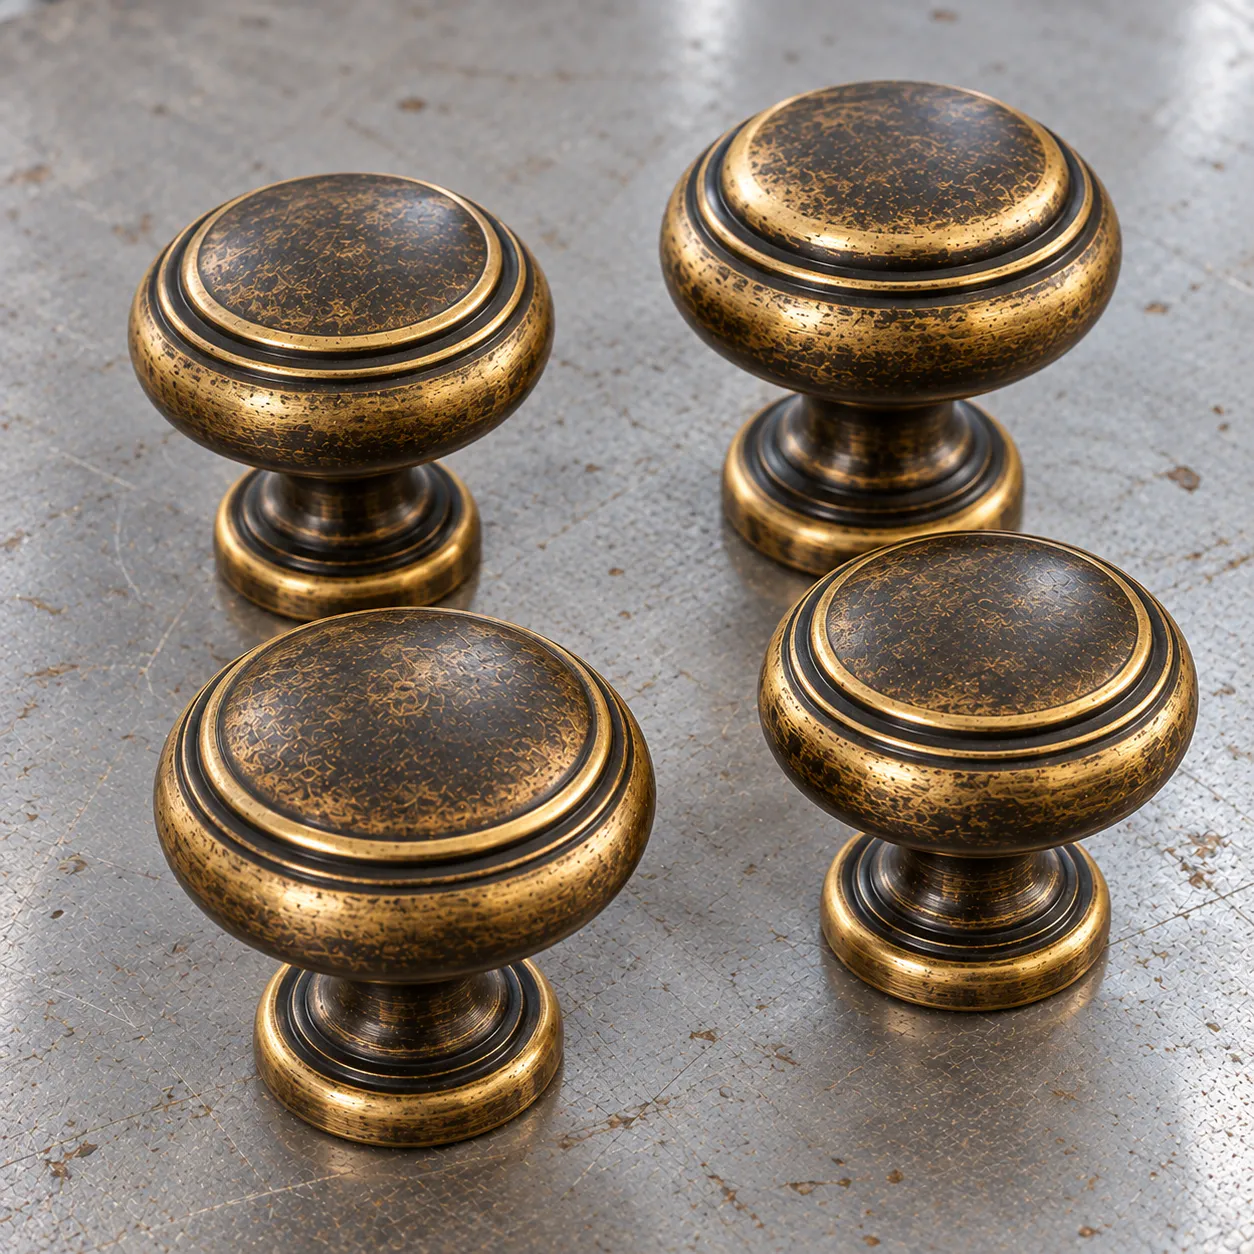
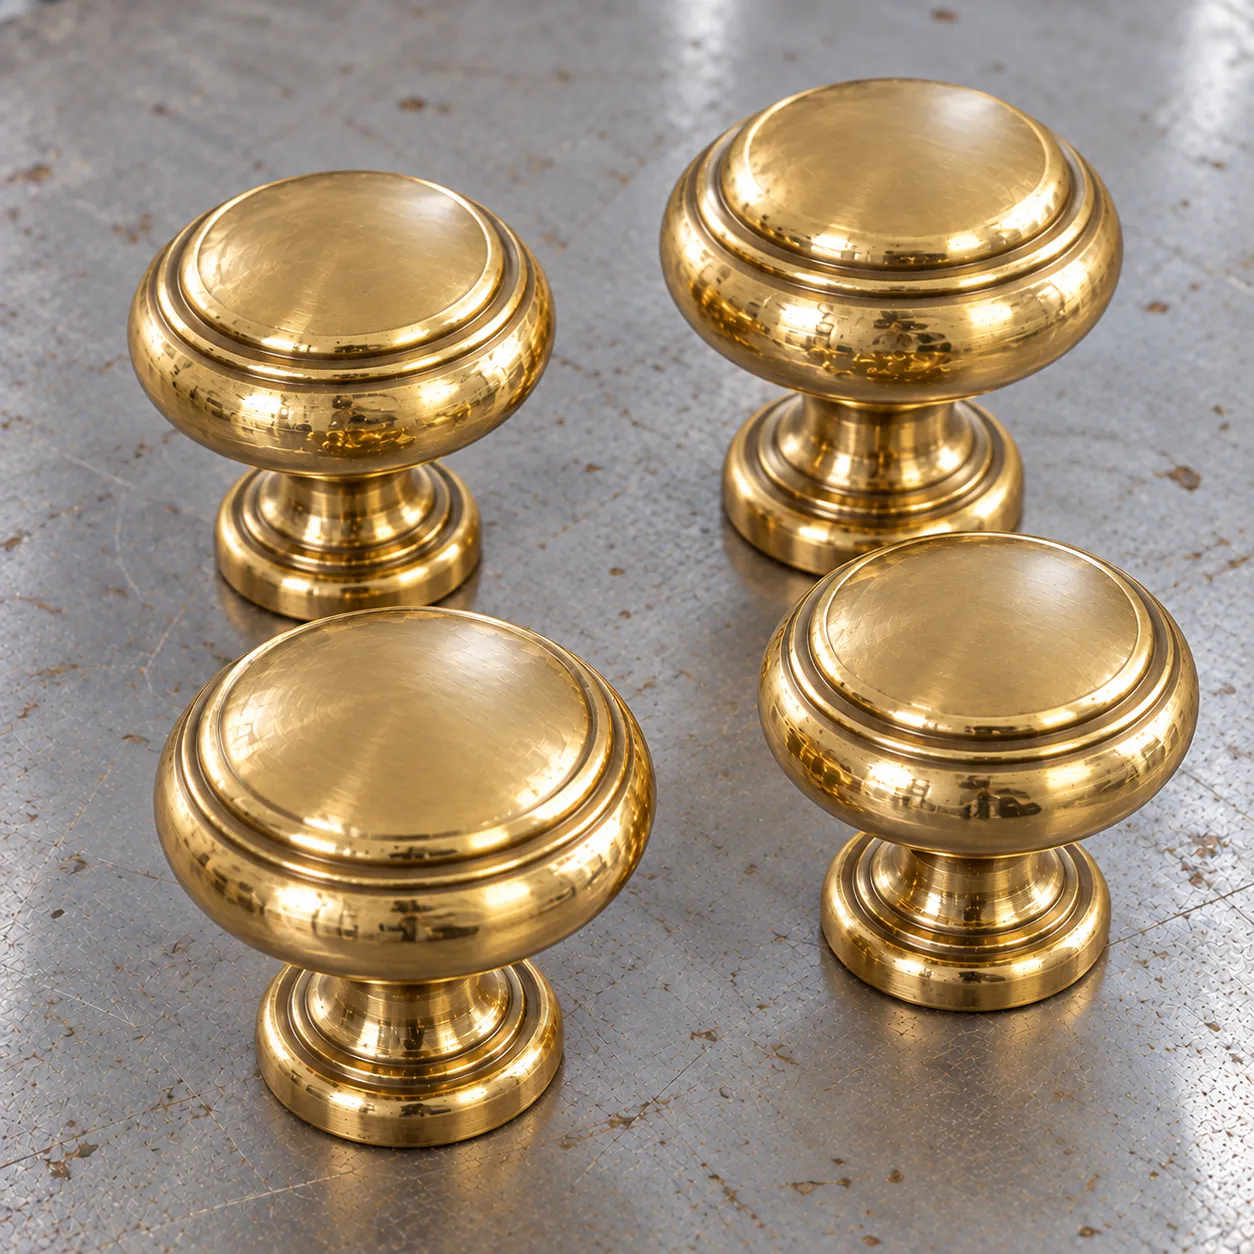 Before
Bright, brand new brass that looked out of place in an old home. Darkened and tumbled so the edges wear back to brass, like decades of use.
See the price before you ship a thing.
Snap a few photos from different angles and tell us the finish you have in mind. You'll get a written quote and a realistic lead time. Standard work takes 3 to 5 weeks, and expedited orders are possible when the schedule allows.
From custom builders to industrial manufacturers, our clients trust us to deliver the same result every time.
Each method has its place. The right one depends on how many parts you have, their shape and the look you want.
The small pieces that tumble with your parts decide how much metal is removed and how the surface looks. We choose them part by part.
Heavy and abrasive. Used to take down burrs, casting skin and tool marks on steel, stainless and other hard metals.
Lighter and gentler, so it smooths brass, aluminum and zinc without cutting too deep or rounding details away.
Fine and dense. It cuts very little and leaves a smooth, bright surface ready for plating or a final polish.
Pins, balls and small shapes that press the surface smooth rather than wearing it away, bringing up a bright shine.
Dry natural media used with polishing compound for a soft luster, and to dry parts without water spots.
The liquid in the tumbler cleans, protects parts from tarnish while they run and helps control how bright the finish turns out.
Here's what happens from the first photo of your production runs of small parts to the day the finished parts ship back to Stanton.
Tell us what the parts are, how many you have and the finish you are after.
Wrap anything fragile, fill the gaps around your production runs of small parts and seal the box well. Your production parts travel to Oceanside insured, and we need the tracking number by email as soon as it's on its way.
We tumble a few pieces first so you can see and approve the finish before the full batch.
Parts run with the media and cycle time dialed in from the sample, in stages when needed.
Every batch is rinsed, dried spot free and checked for lodged media and missed burrs.
Parts move on to plating or patina, or are packed by part number and shipped back insured.
Hard metals and soft metals behave very differently in a tumbler. Each gets its own media and cycle time.
Take a beautiful satin or burnished finish and are the go to metals for the decorative tumbled look on hardware and castings.
Deburred and smoothed with cutting media, then rinsed and dried quickly so the bare steel does not flash rust before plating.
Tough enough for aggressive media. Tumbling gives stainless an even satin or bright burnished look without hand polishing.
Soft and easy to over process, so it runs with lighter media and shorter cycles to protect details and dimensions.
Soft castings with fine detail. Gentle media removes parting lines and flash without rounding off the design.
Light tumbling over plating creates a worn antique look. We review these first, since too much time cuts through the finish.
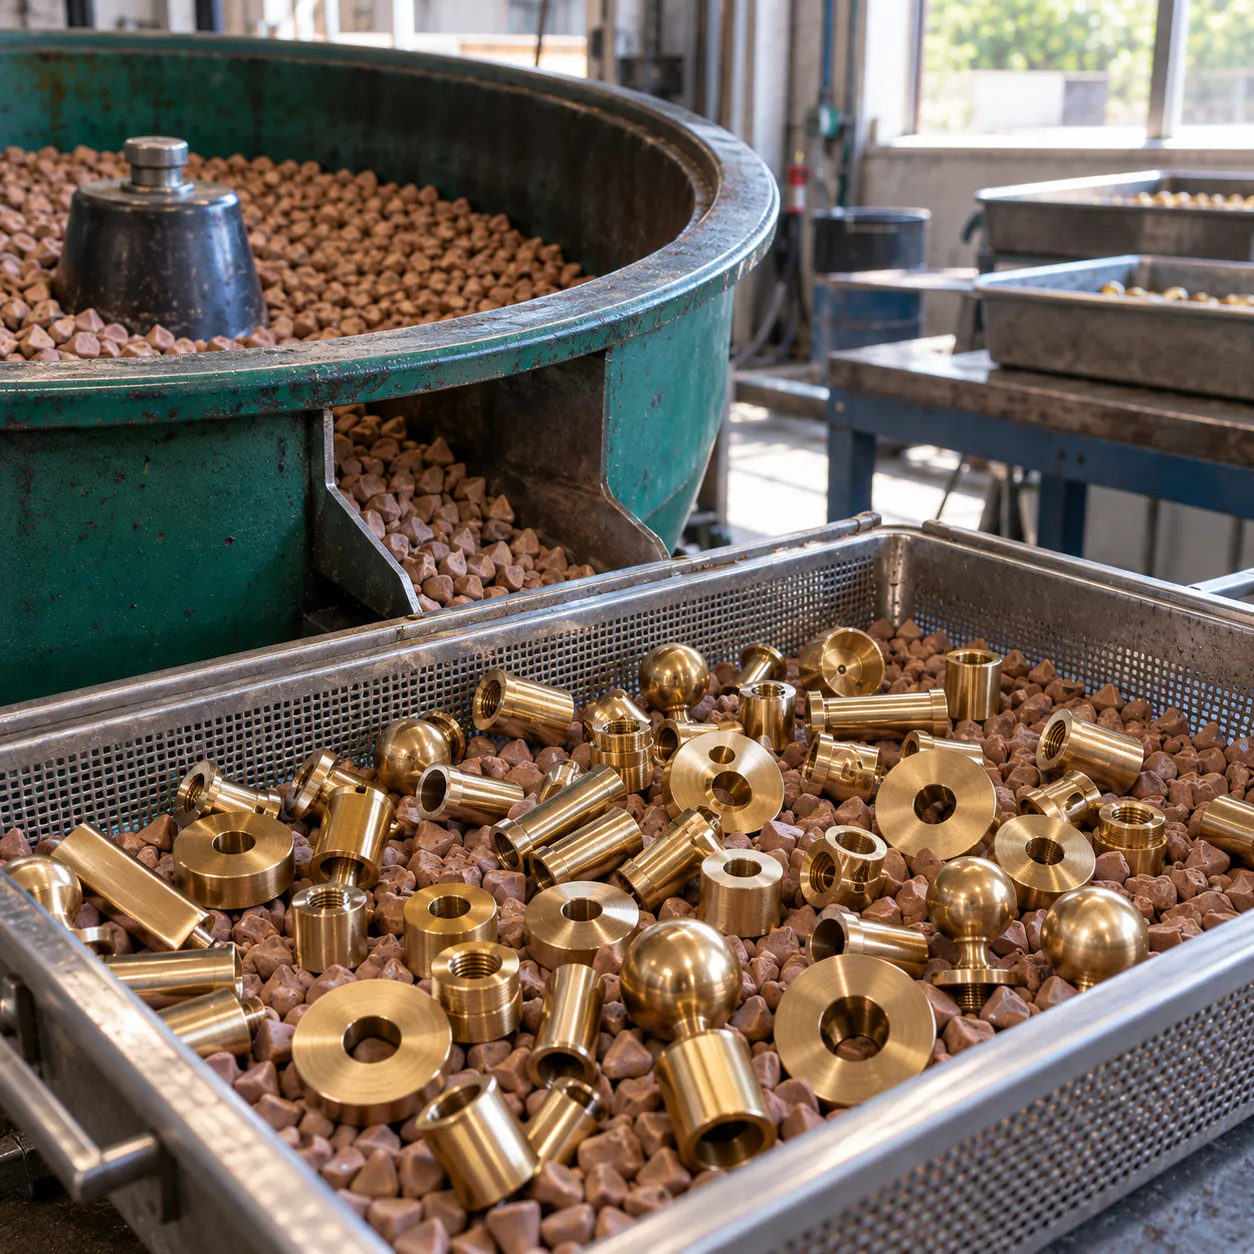
Since 1989 we have finished metal for manufacturers, designers and restorers. Tumbling, plating and patina all happen under one roof, so your parts go from rough to finished without changing hands.
Send photos and a part count and receive a no obligation quote within 24 hours.
Every batch leaves our shop backed by our craftsmanship guarantee. If you are not satisfied, we make it right.
Small parts in bulk ship easily and affordably. Send a box from any state and get it back insured.
Most projects are completed within 3 to 5 weeks. Expedited Orders: 5 to 7 business days. Contact us for availability.
Everything we do in the tumbler, the finishes it creates and the services that often follow.
Tumbling looks easy from the outside. Getting the same result on hundreds of parts without damaging a single one takes care.
A few parts are run and approved before the full batch, so there are no surprises when the rest come out.
Media size and type are matched to the metal and the holes in each part, to avoid lodging and over cutting.
Finished parts are checked for leftover burrs, stuck media and water spots before they are packed.
Different parts are run and packed separately and labeled the way you sent them, ready for your stock shelf.
Tumbling serves a wide mix of businesses. These are the kinds of work we finish most, and production runs of small parts from Stanton can fit any of them.
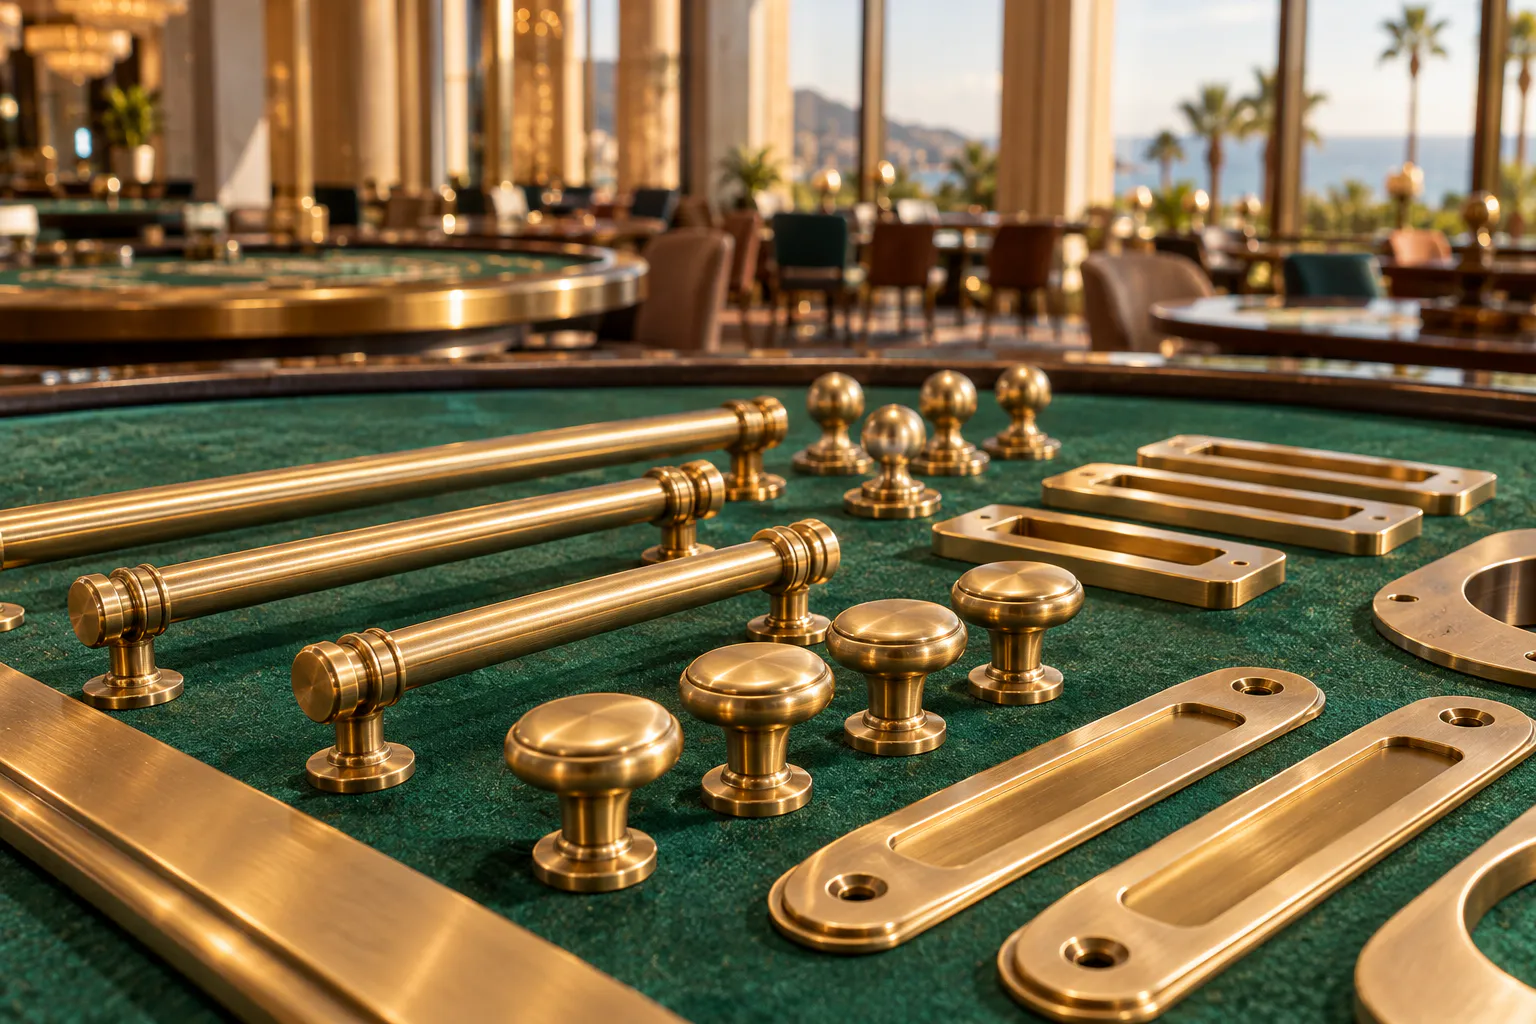
Small brass trim, table hardware, rail fittings and decorative accents finished in matching batches, so replacement pieces blend in with the rest. Trusted by casino resorts across North County San Diego.
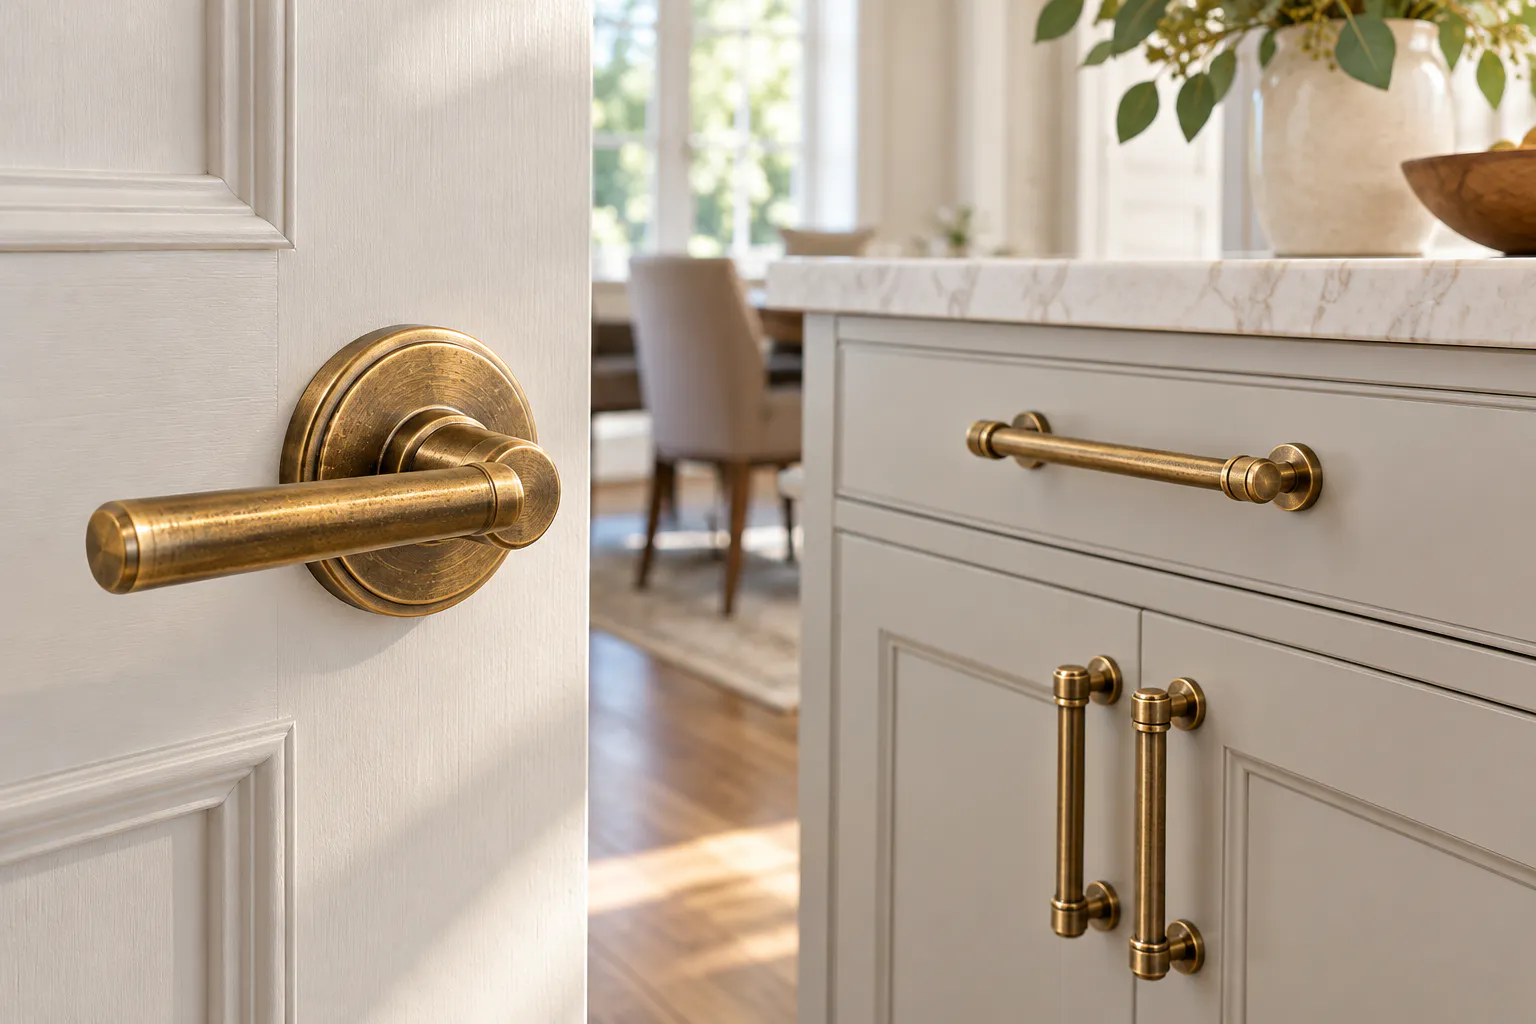
Hinges, pulls, knobs and escutcheons with a soft tumbled finish that matches across an entire home or project.
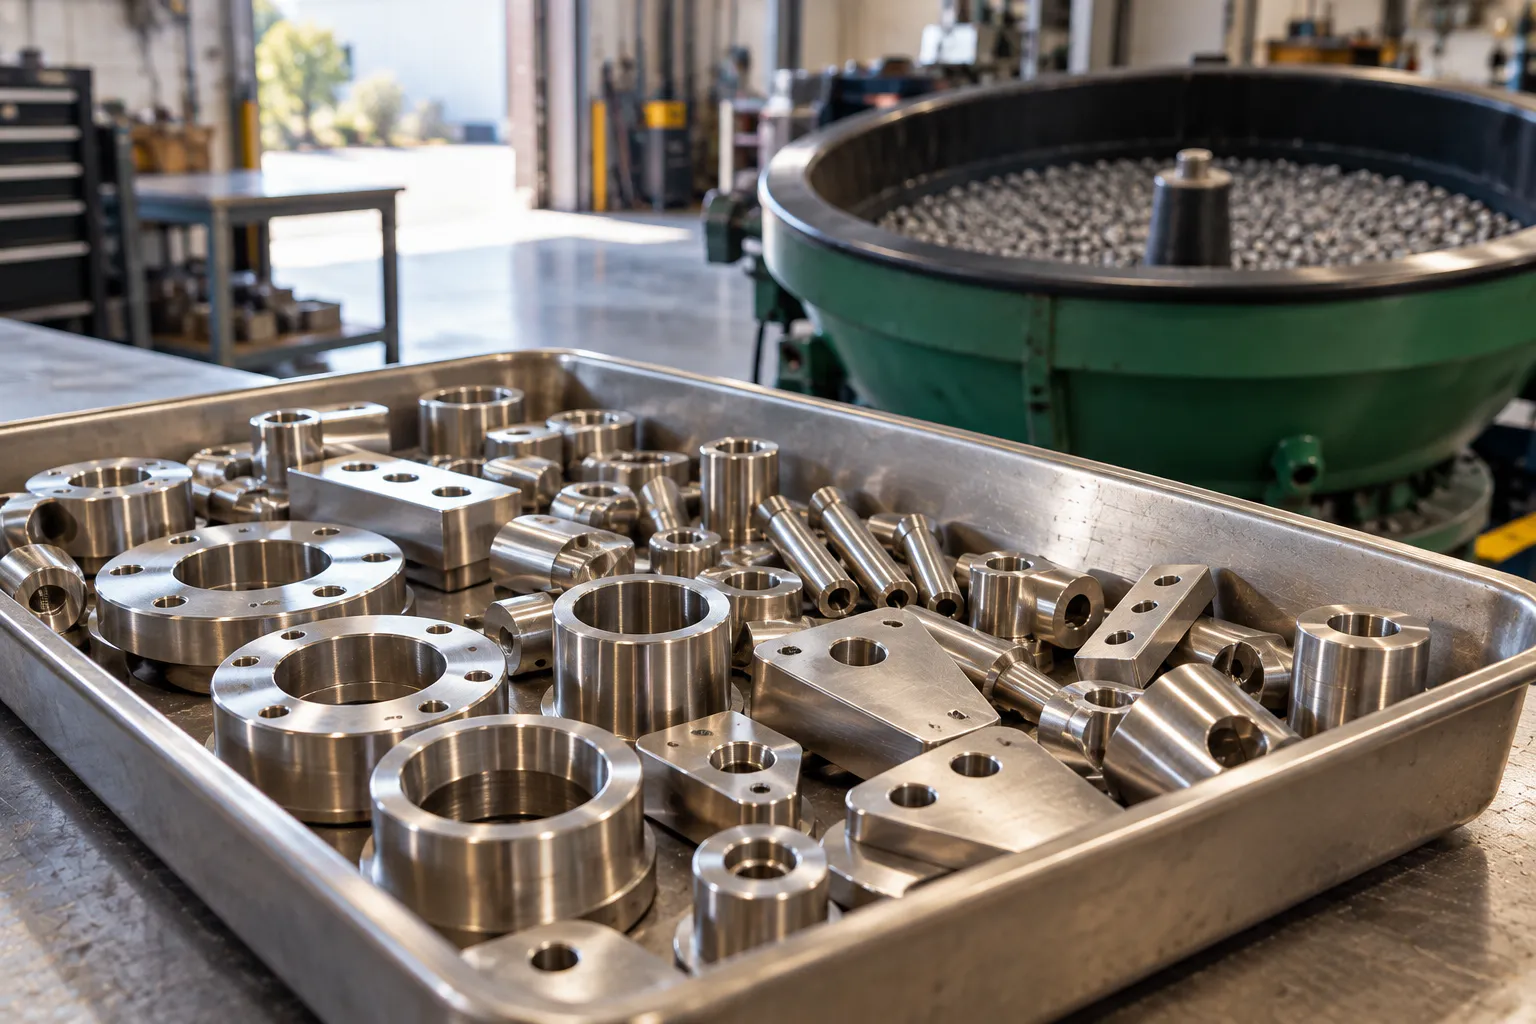
Production parts deburred and smoothed in volume, ready for plating, coating or assembly.
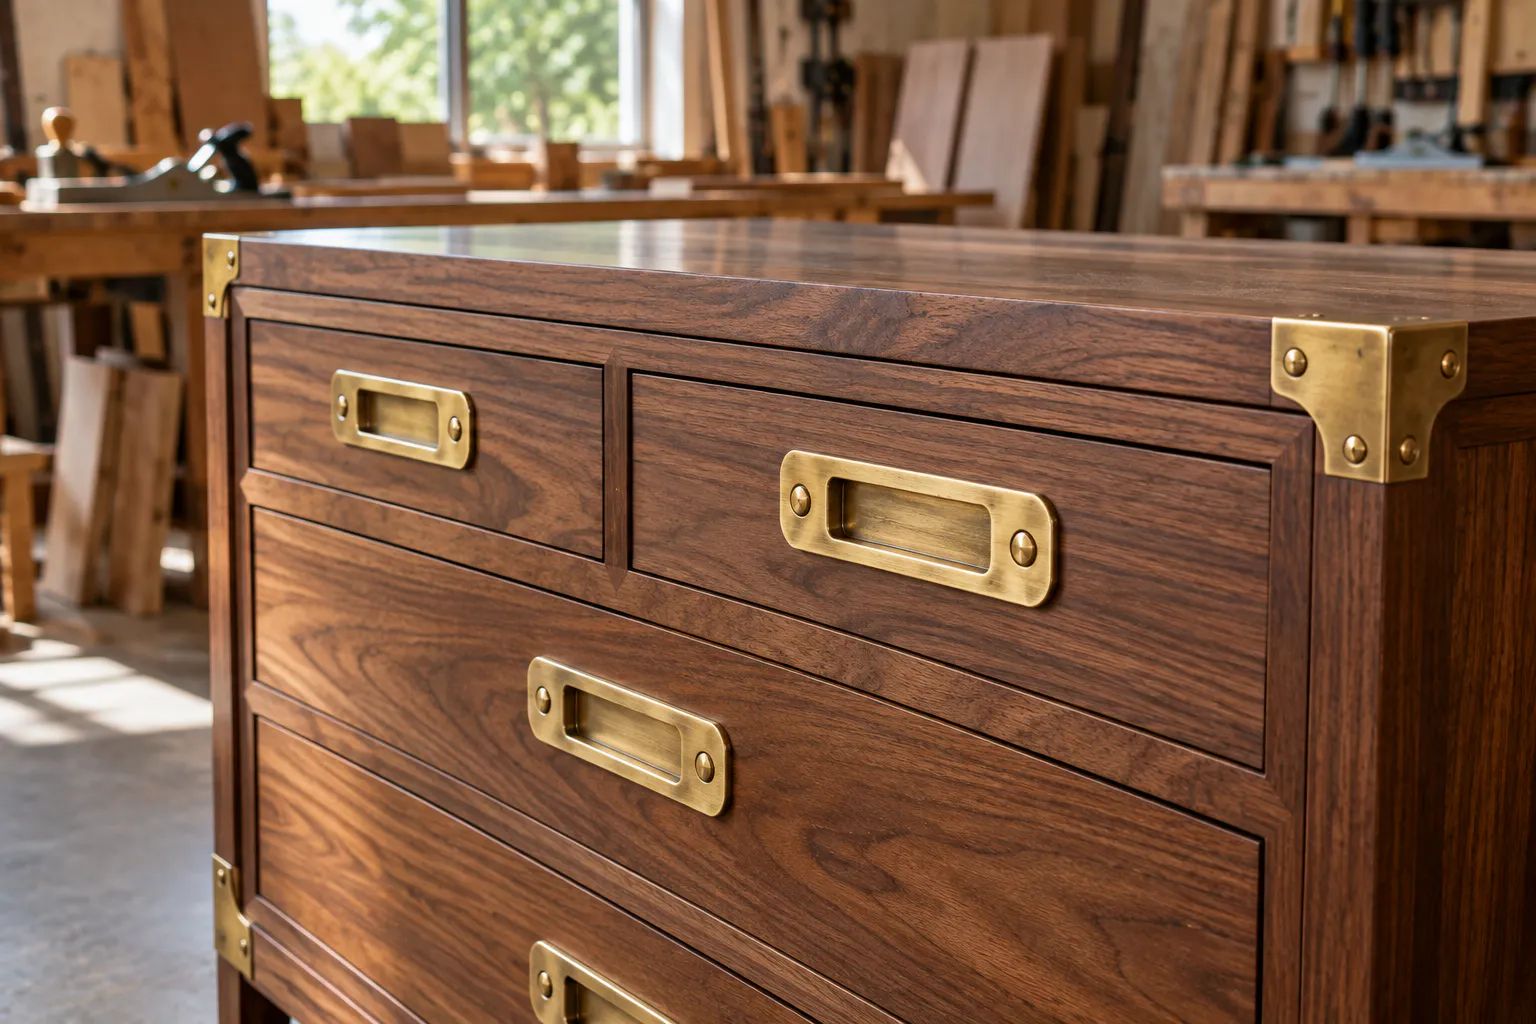
Furniture makers use tumbled hardware for a warm, hand finished look on cabinets, chests and tables.
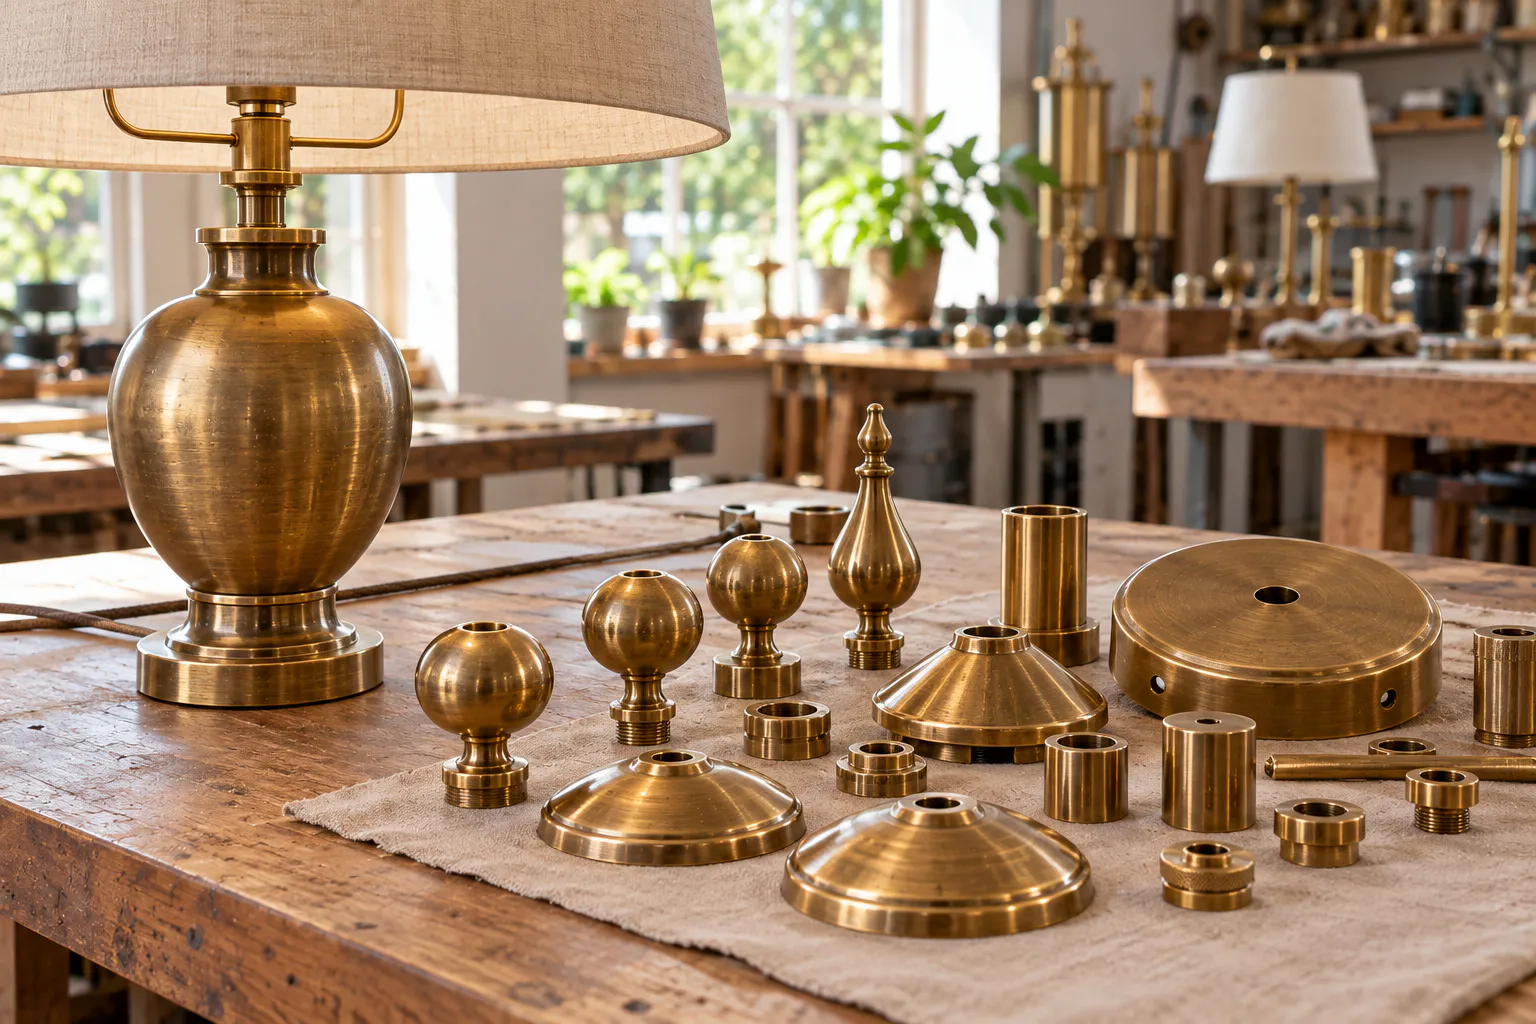
Small lamp parts, finials, canopies and fittings given an even finish before plating or patina.
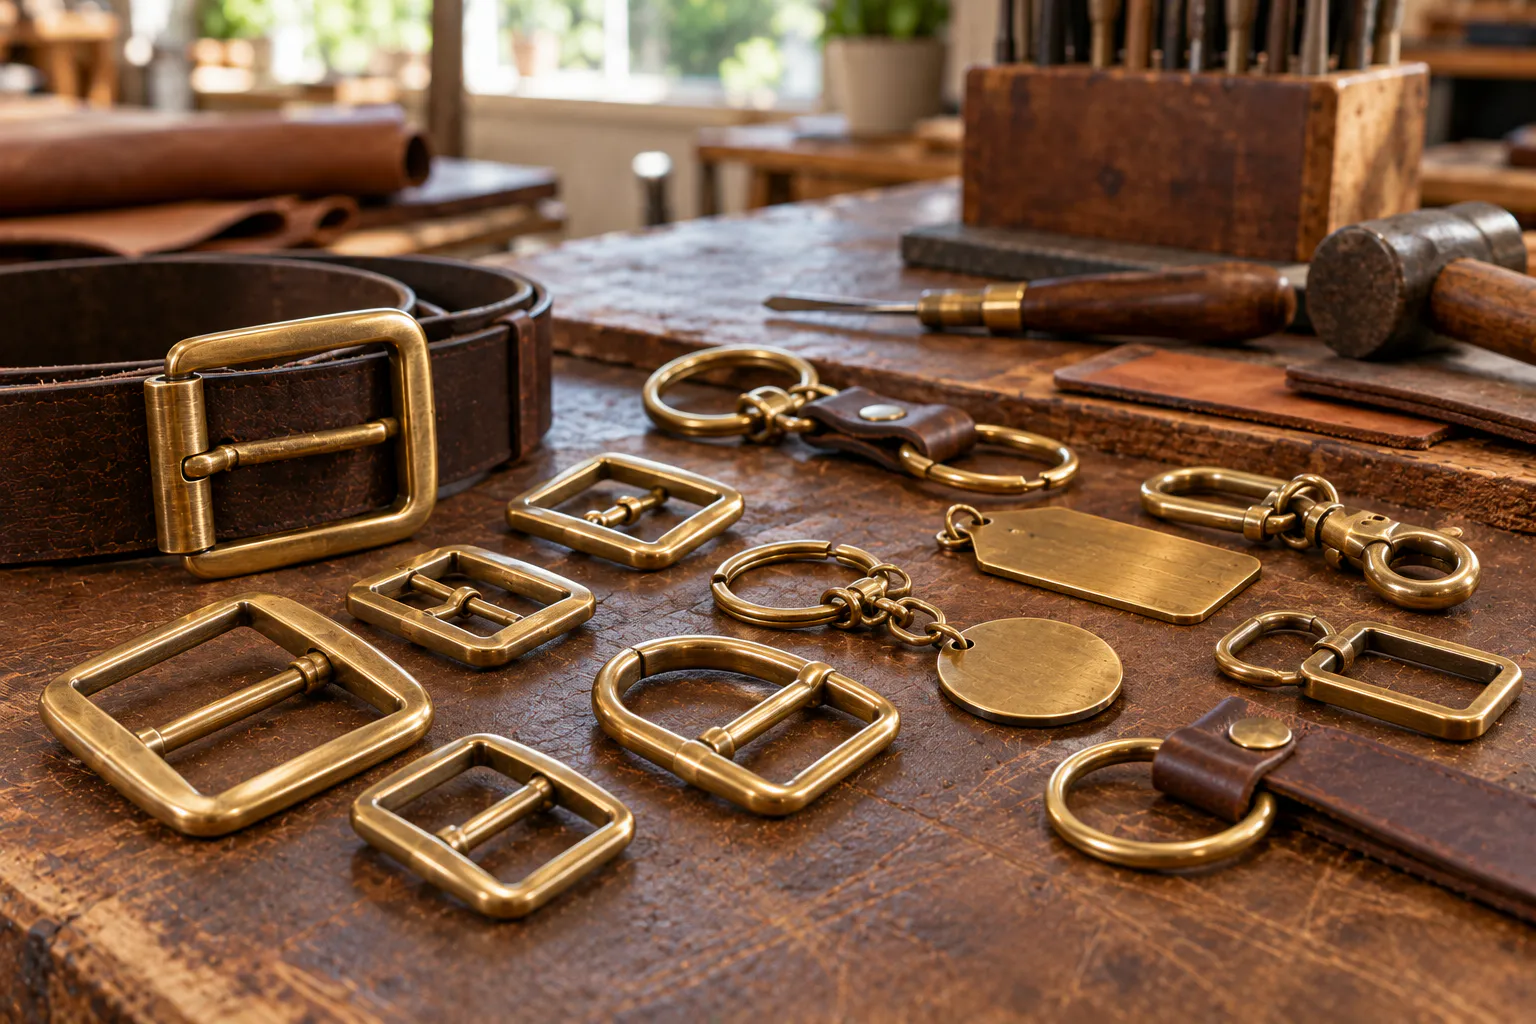
Buckles, keychains, tags and other small metal goods finished in batches for makers and growing brands.
Help us help you, tell us about the production runs of small parts
Think about condition before you pack. Production runs of small parts that are oily, painted or heavily rusted can still be tumbled, but we need to know ahead of time. Cutting oil comes off in the tumbler, while thick coatings on production parts might need another step first.
It also helps to know where the production runs of small parts go next. Anything headed for plating from Stanton gets a smoother, brighter surface than something meant to stay bare, and we plan the media and cycle time around the same finish on every piece.
Point out holes, slots and threads. Media can wedge into openings that are close to its size, so we pick a media shape and size that stays clear of them. Telling us the hole sizes up front saves time for everyone.
Finally, let us know what happens next. Parts that will be plated get a different finish than parts that will be lacquered or left bare, and parts headed for an assembly line can be packed the way your team needs them.
Tumble Finishing Gallery
Hardware, castings and production parts deburred, smoothed and tumbled in our Oceanside shop.
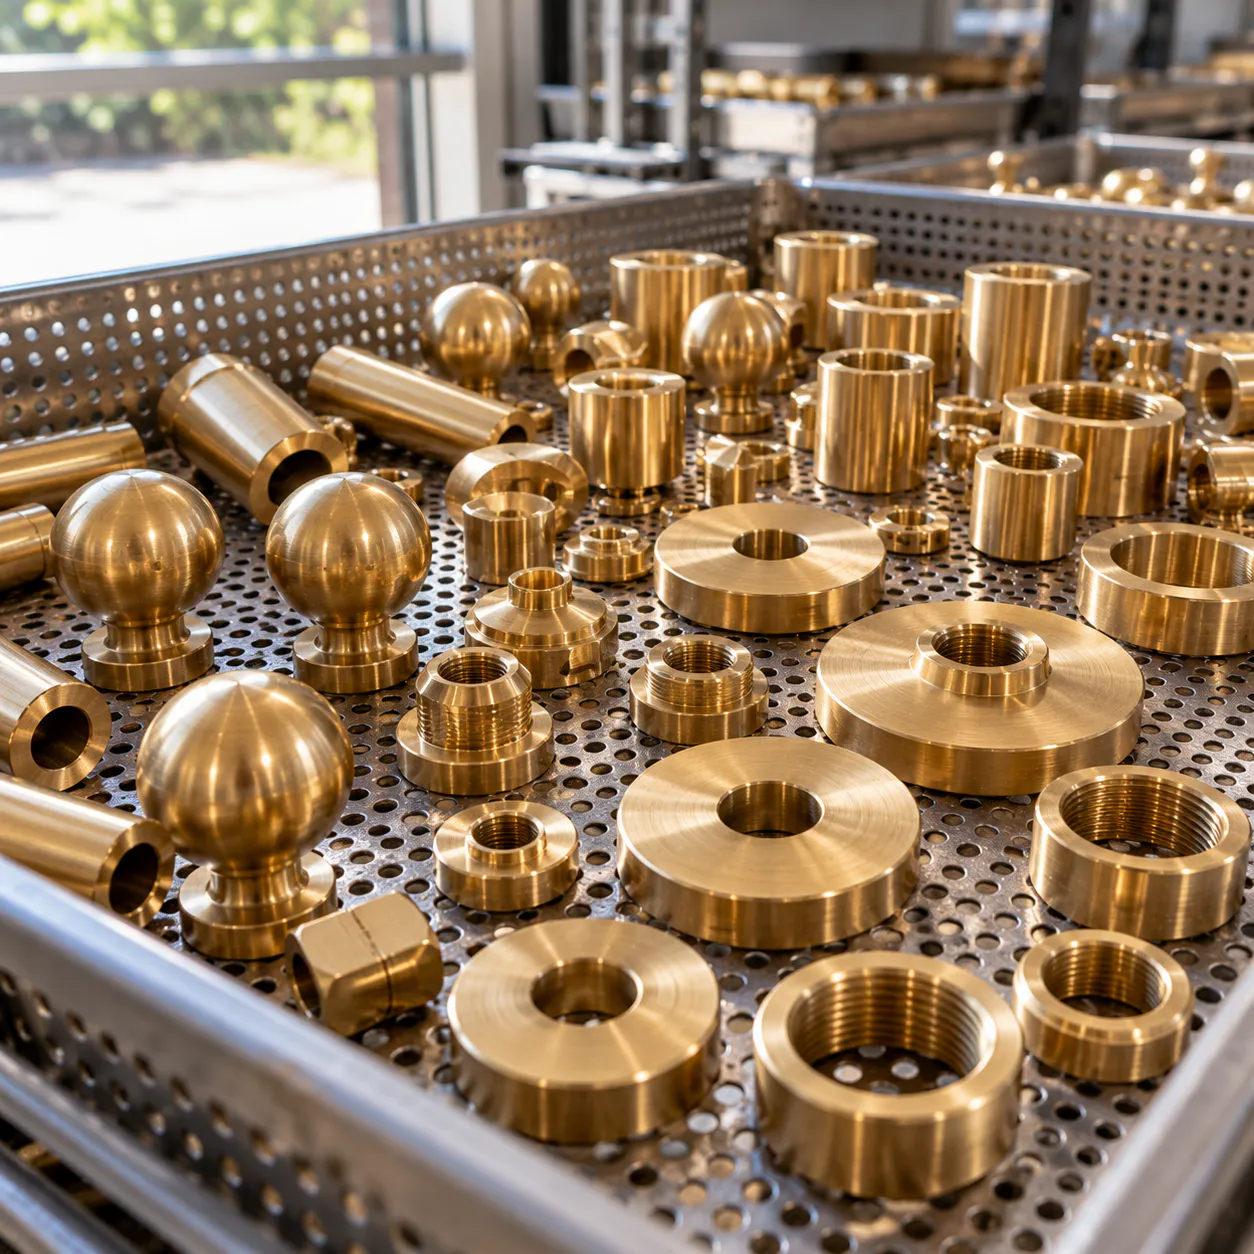
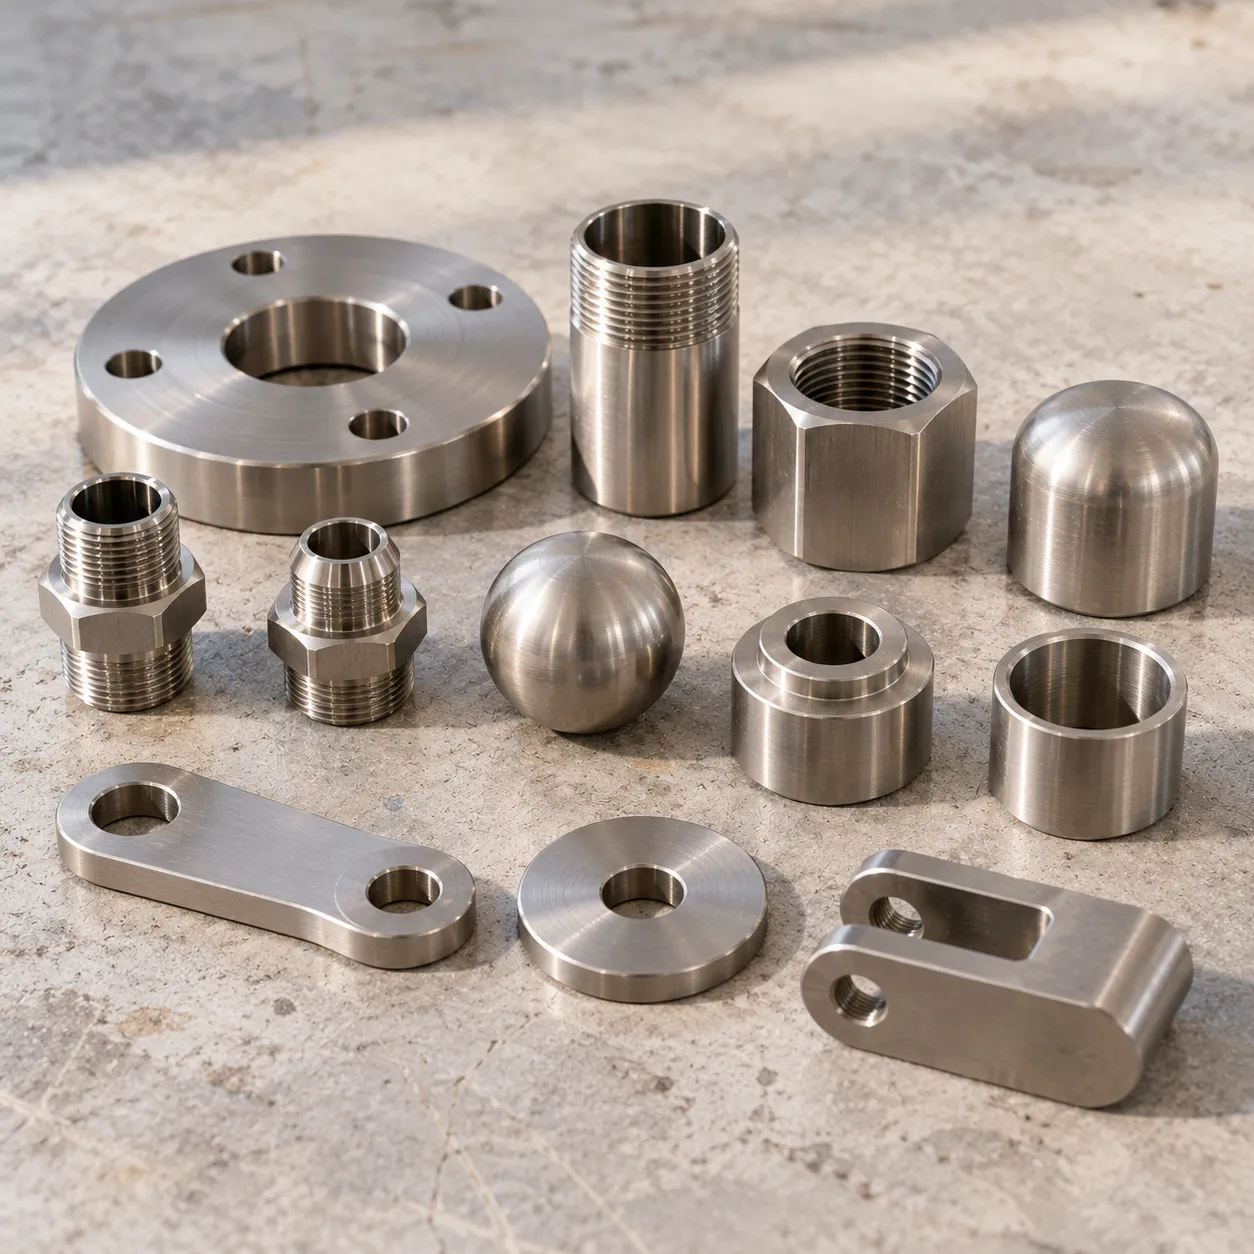
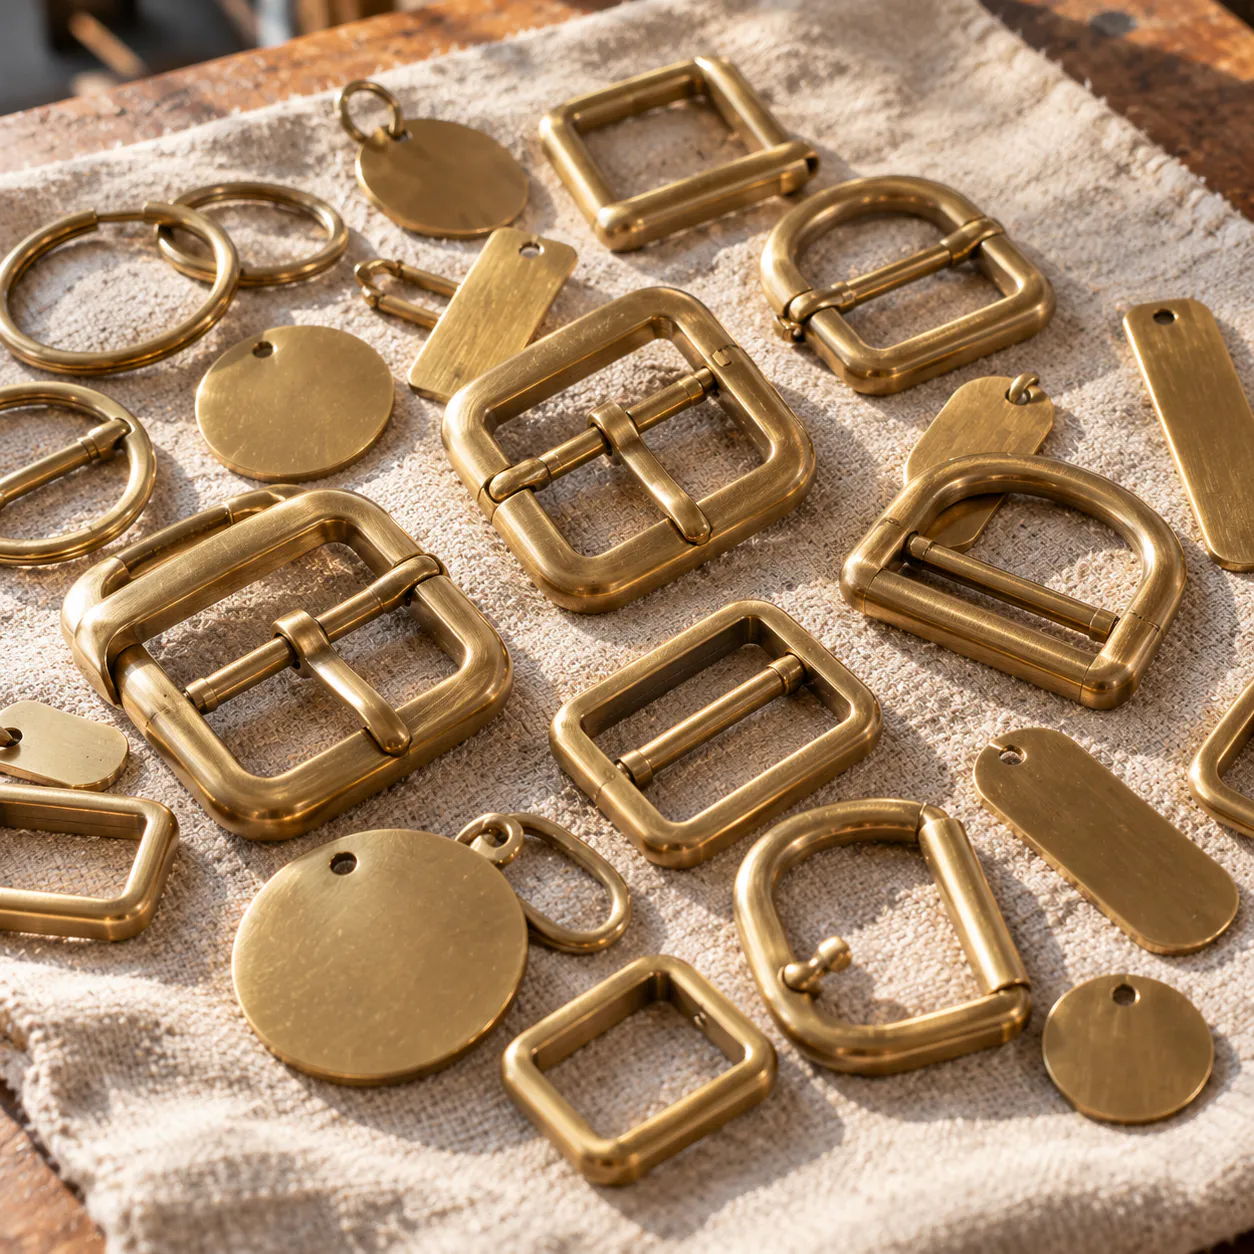
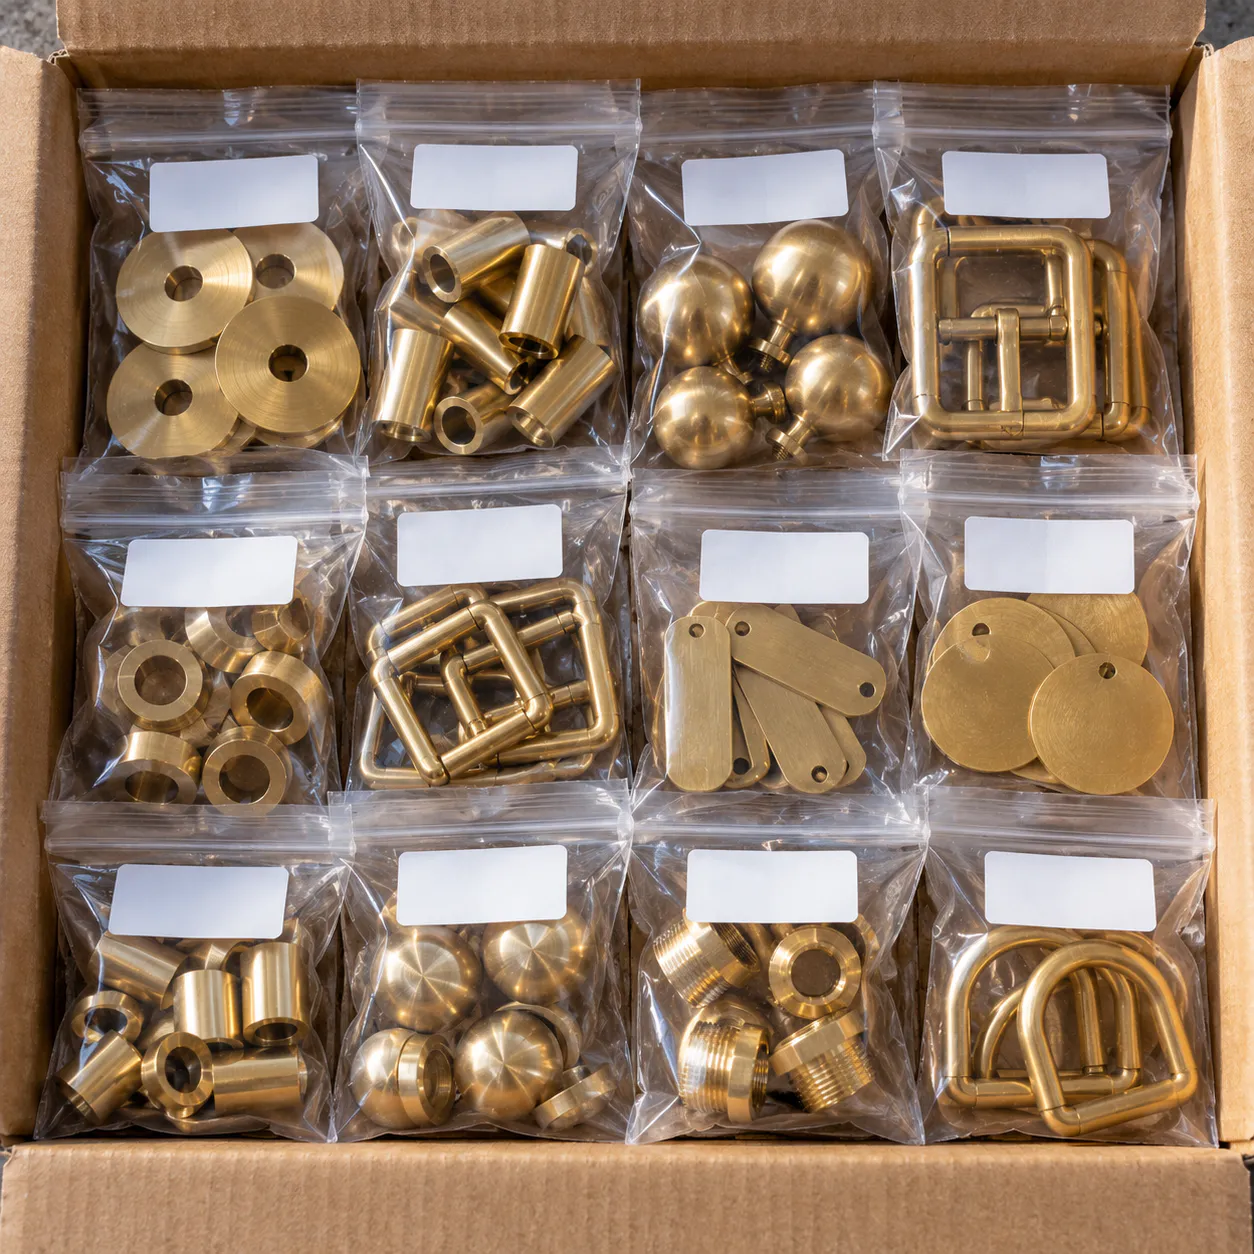
From quote to return shipping, here's the whole mail in process for production runs of small parts leaving Stanton. It only takes a few minutes to get your production parts ready.
Send photos, the metal type and a part count. You will get a written price and lead time, usually the same business day. Please wait for your quote number before shipping.
Keep each part type in its own labeled bag. Mixed parts take longer to sort and hard pieces can mark softer ones on the way here.
Small parts are heavy, so use a strong box and fill the empty space. Insure the box for its real value and email us the tracking number.
We send photos of the sample or finished batch when needed, then pack everything by part number and ship it back insured.
Local shops and makers are welcome to drop off parts for tumbling at our facility in North County San Diego.
Tumble finishing, plating and patina under one roof since 1989.
Wherever you are around Garden Grove, Anaheim or Stanton, the process is the same. Stanton is in northern Orange County, so parts travel by mail and come back insured and packed by part number.
If you're closer to Garden Grove than Stanton, one of these nearby pages may fit better.
Frequently Asked Questions
Here are straight answers to the questions people ask before sending production runs of small parts from Stanton. Don't see yours? Call us or send a message.
Yes. Ask for a quote first with photos of your production runs of small parts and a part count, and wait for your quote number before you ship. It lets us match the box to your order and plan the finish for your production parts ahead of time.
Yes. Shops, makers and homeowners anywhere can mail production runs of small parts to us. Production parts from near Garden Grove, Anaheim or Stanton follow the same path: photos, a written quote, a sample, then the full batch.
Yes, but tell us about them first. Media can wedge into openings close to its own size, so we pick a shape and size that stays clear of the openings on your production runs of small parts. Send the hole sizes of your production parts with your photos, and every finished batch is checked for lodged media.
We choose by metal. Ceramic cuts fast on hard metals, plastic is gentler on brass, aluminum and zinc, porcelain leaves a fine smooth surface, and stainless steel shapes burnish, so we match the media to your production runs of small parts. For production parts, walnut shell and corn cob handle dry finishing and drying when it's needed.
Yes. Hard and soft parts never share a load, and each part number of production runs of small parts is run, bagged and labeled on its own. When the batch is done, your production parts are packed by part number and shipped back insured.
Yes, and most of our work starts that way. We strip the old plating down to the base metal, repair what needs repair, then plate it fresh. New plating over a failing layer never lasts, so we don't do it.
We do. Along with single pieces for homeowners, we run batches of hundreds or thousands of parts for companies in California and other states. Send a photo of a sample, the quantity and the finish, and we'll quote the whole run.
Steel, stainless steel, aluminum, brass, bronze, copper, pot metal and zamak. Some of them need extra prep so the plating bonds well, and we'll tell you up front if your part does.