

High Phosphorus
Roughly 10 to 13 percent phosphorus. The most corrosion resistant option and essentially nonmagnetic, chosen for parts exposed to moisture, salt and chemicals.
An autocatalytic bath deposits nickel-phosphorus on activated metal surfaces. This makes solution access and substrate preparation central to the process review, particularly when the component includes internal channels or multiple alloy types.
Keep critical dimensions in the first project review.
Electroless nickel is not applied by electrical current, so the review focuses on the chemical reaction, the substrate and bath access. This distinction can be useful for components with complex external profiles.
A PTFE-containing composite is an optional route for certain friction-related needs. It should not be requested solely as an upgrade; describe the functional reason so suitability can be considered.
Parts with blind holes or narrow passages should include section views. These details help determine whether the plating solution can reach and drain from the surfaces that need coating.
Send us the drawing or a few photos, the material, and what the part does in service. If your print calls out a coating specification or a finished dimension, include it. We will recommend a phosphorus range and a thickness, tell you whether masking or heat treatment makes sense, and send back a written quote.
Include any request for masking, special thickness control or a composite deposit in the original quote package. Late changes may affect technical review and scheduling.
Roughly 10 to 13 percent phosphorus. The most corrosion resistant option and essentially nonmagnetic, chosen for parts exposed to moisture, salt and chemicals.
Roughly 5 to 9 percent phosphorus. The general purpose workhorse, with a bright appearance and a balance of hardness, wear and corrosion protection that suits most industrial parts.
Roughly 1 to 5 percent phosphorus. The hardest deposit as plated, selected for sliding surfaces, tooling and components where wear resistance matters more than chemical exposure.
A bake after plating can raise hardness to a level that competes with hard chrome, or relieve hydrogen in high strength steel. The cycle is matched to the chemistry and the base metal.
Fine PTFE particles locked into the nickel matrix create a dry lubricating surface. Used on molds, fasteners, sliding mechanisms and anything that needs low friction or easy release.
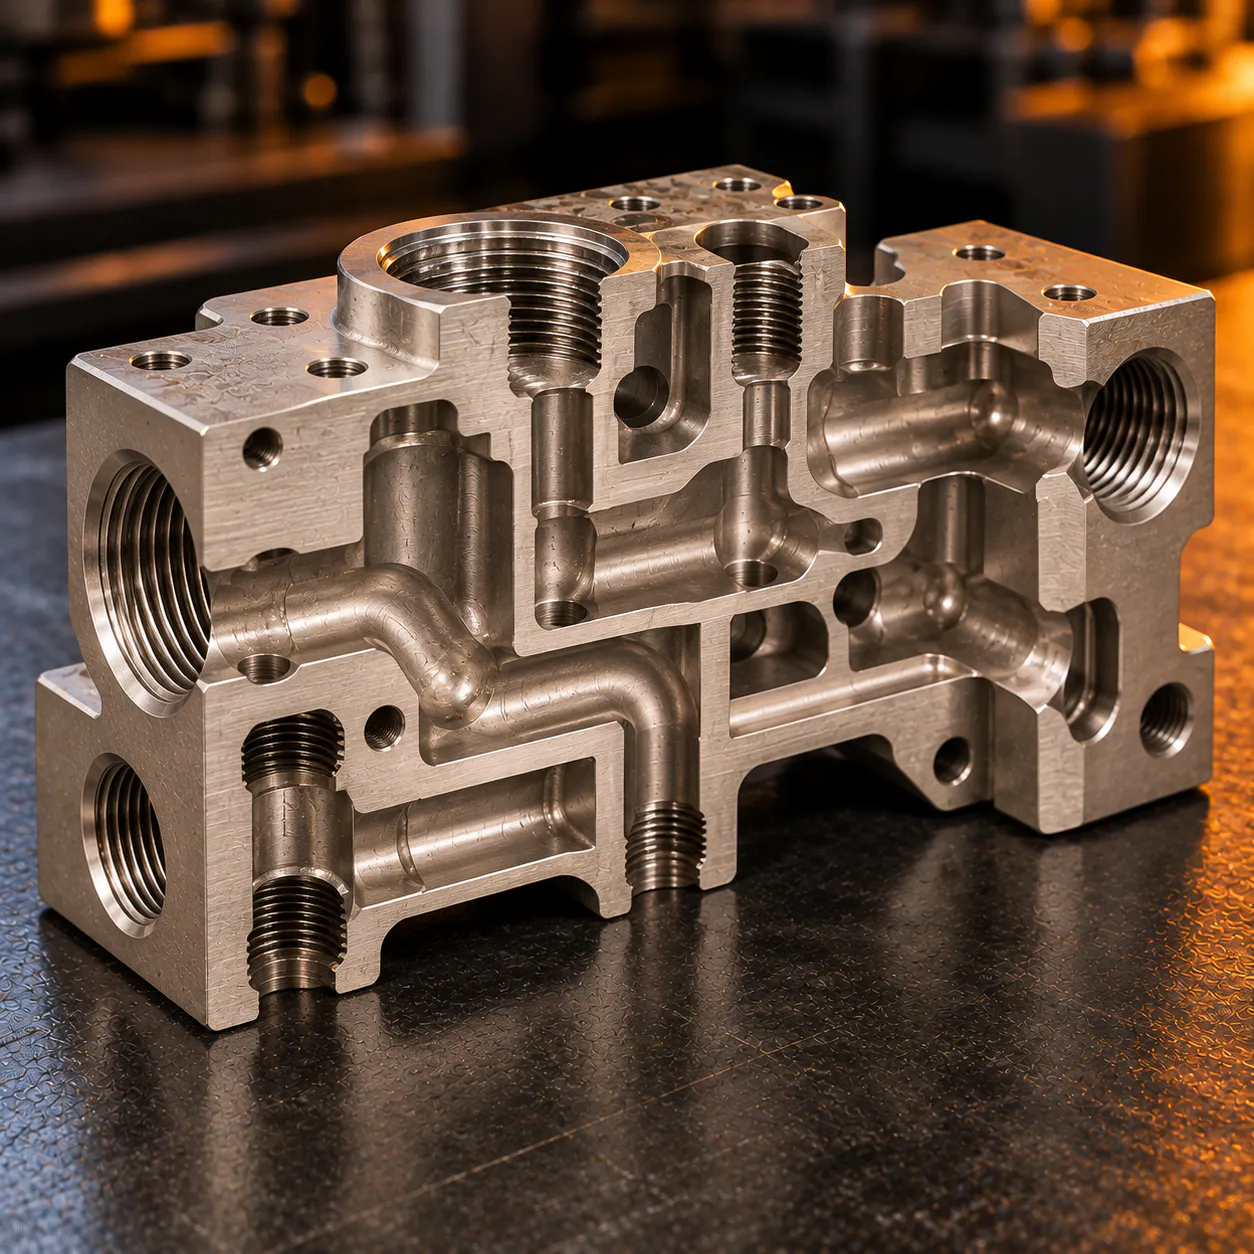
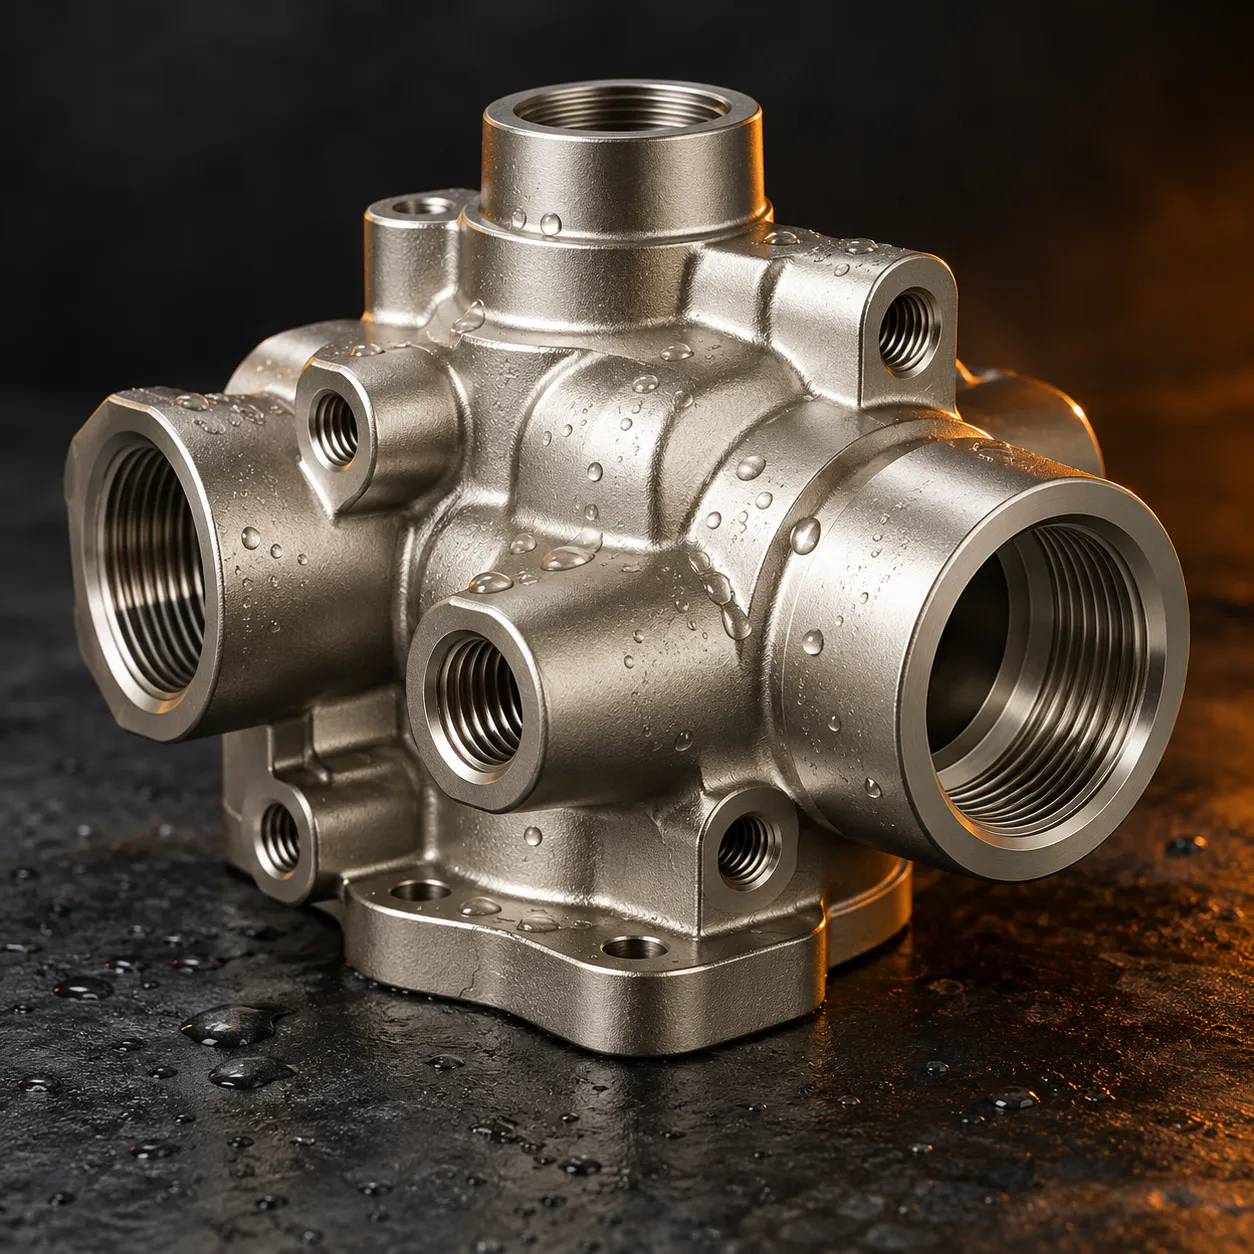
Internal passages, blind holes, fine threads and deep pockets get the same coating as the outside of the part. Often the only practical choice when conventional plating cannot reach.
We run all three of these processes in house, so we have no reason to push one over another. Here is how they differ and when each one is the right call.
The plating bath is the same for every part. The preparation is not. Each substrate has its own cleaning and activation sequence, and getting it right is what keeps the coating attached.
The most common substrate we coat. After degreasing and acid activation, steel accepts every phosphorus range. High strength steels can receive a hydrogen relief bake after plating.
Its passive oxide film blocks adhesion, so it gets a nickel strike before the electroless bath. Often coated to stop galling on threads or to add surface hardness.
Aluminum oxidizes within seconds, so it receives a zincate treatment that protects the surface until the nickel takes over. The alloy matters, so tell us the grade if you know it.
Copper does not start the reaction on its own, so it is activated before plating. Electroless nickel then acts as a durable barrier against tarnish and diffusion.
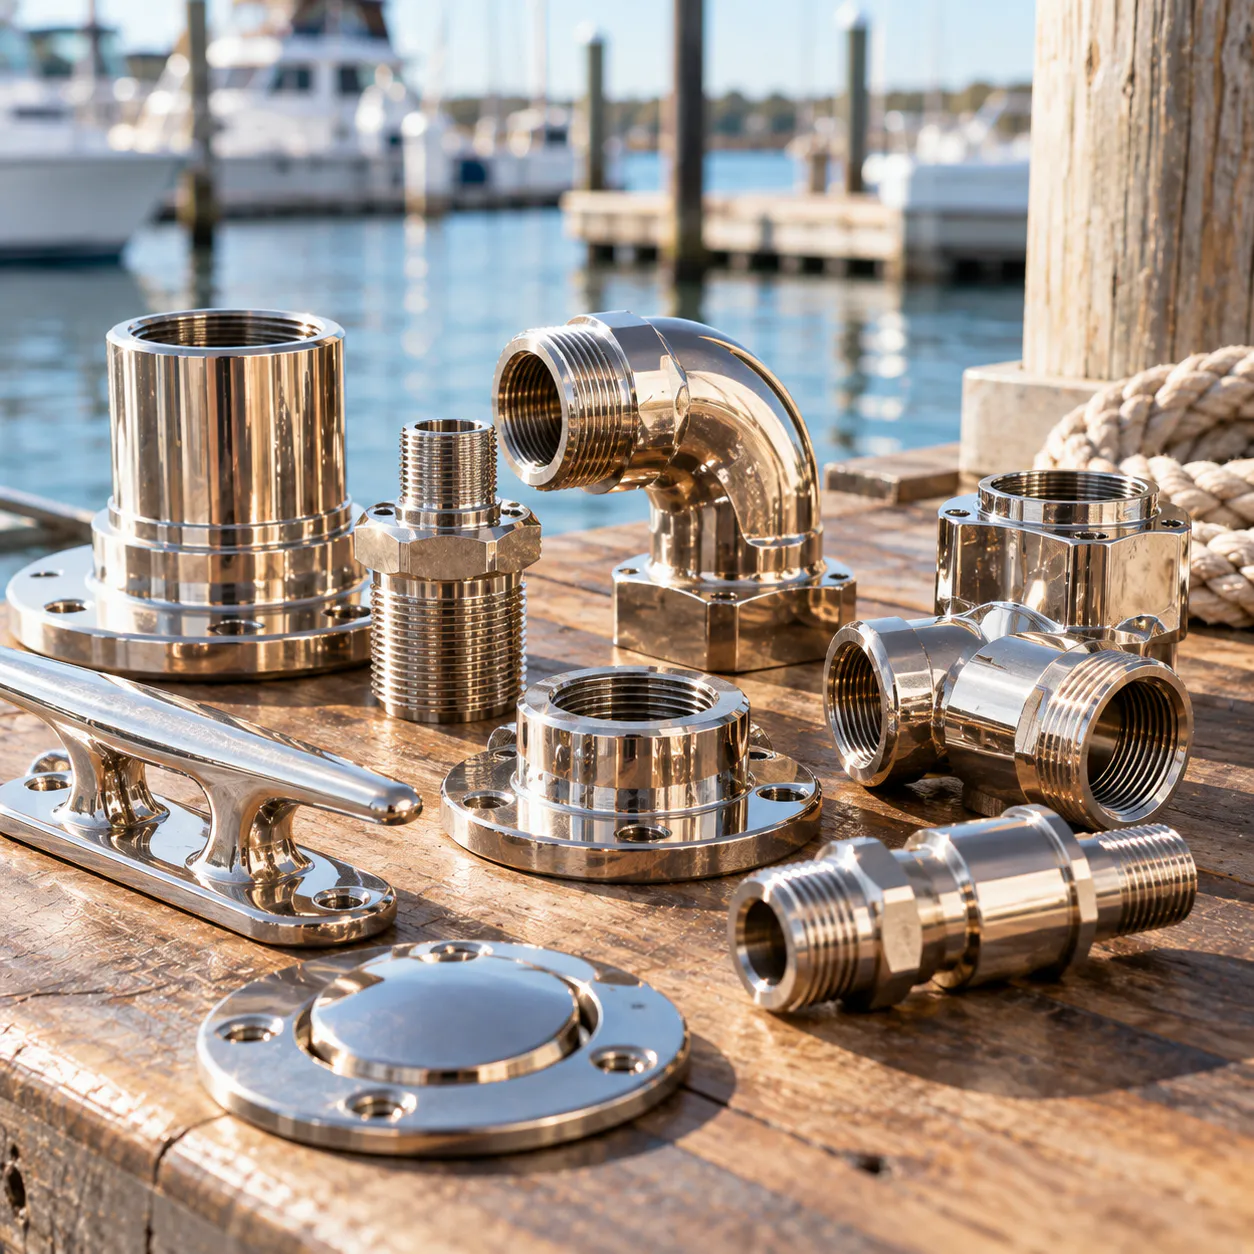
Valve bodies, fittings and marine components plate cleanly once activated. The nickel layer protects against dezincification and adds a harder working surface.
Nickel alloys, tool steels and cast parts can be coated case by case. Send the exact alloy designation so we can confirm the activation sequence before you ship.
Everything we offer around electroless nickel, from the chemistry itself to masking, stripping and post plate treatment.
Where internal passages are involved, the shop evaluates whether solution access is practical. Section views and passage dimensions help clarify the geometry.
Send photos or a drawing, the material, the quantity and any coating callout on your print.
We suggest a phosphorus range and thickness and send a written quote within 24 business hours.
Once the project is scheduled, pack components to avoid impact and abrasion in transit. Include the approved quote reference and identify any separate containers by part number. Protect heavy steel parts from contacting lighter components during transit.
Parts are degreased, masked where needed, activated for their alloy and plated in a controlled bath.
Coverage and thickness are checked, any heat treatment is completed, and parts ship back insured.
From custom builders to industrial manufacturers, our clients trust us to deliver the same result every time.
Maintenance replacements, new production hardware and custom-machined parts can share a coating process while requiring different specifications. Explain whether steel and stainless-steel assemblies are new, refurbished or part of a repeat order. Steel assemblies may have hardness or heat-history requirements that affect post-plating decisions.
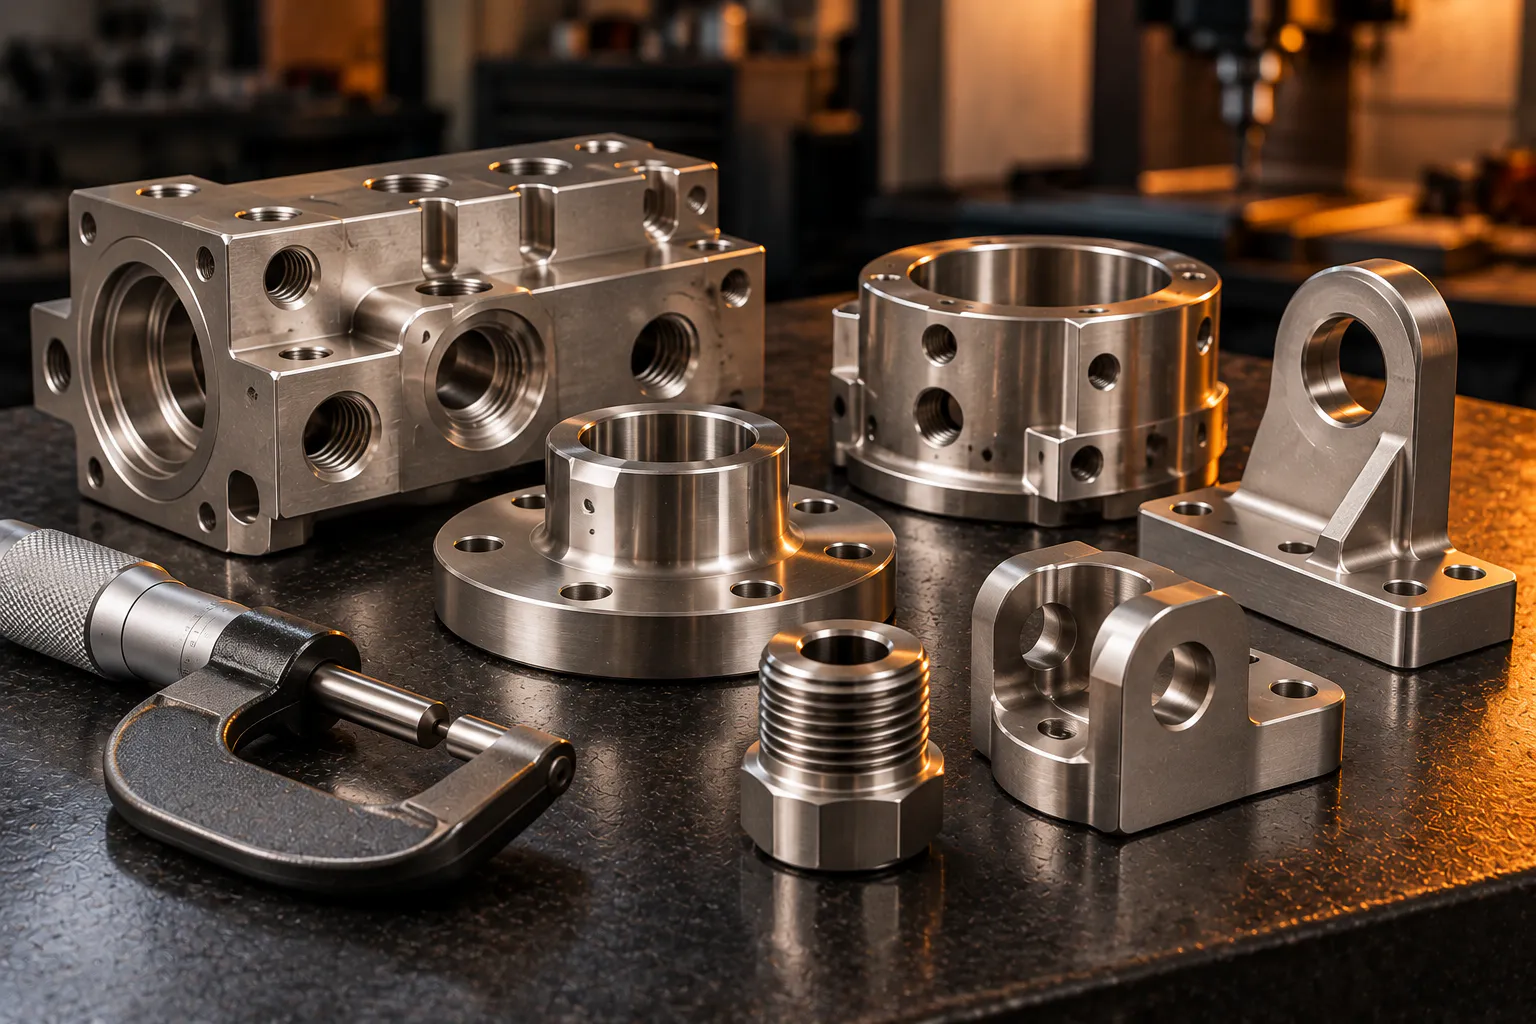
CNC parts with tight tolerances, where the coating has to go on evenly so the part still fits after plating.
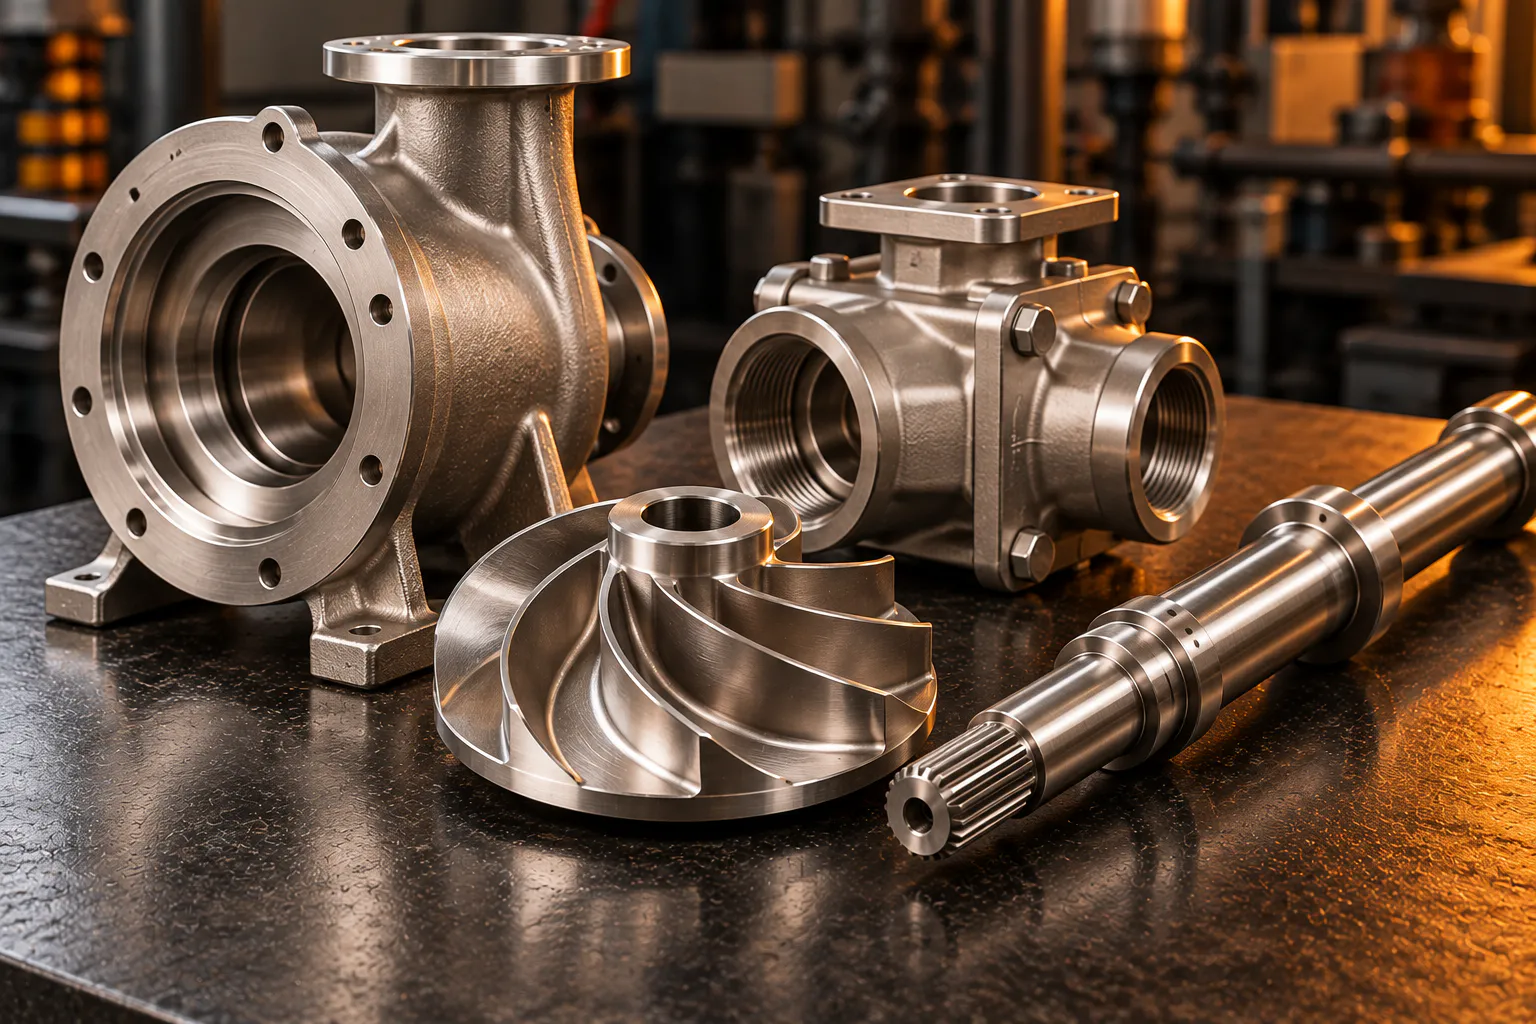
Valves, pump housings, shafts and fixtures that need corrosion protection inside passages as well as outside.
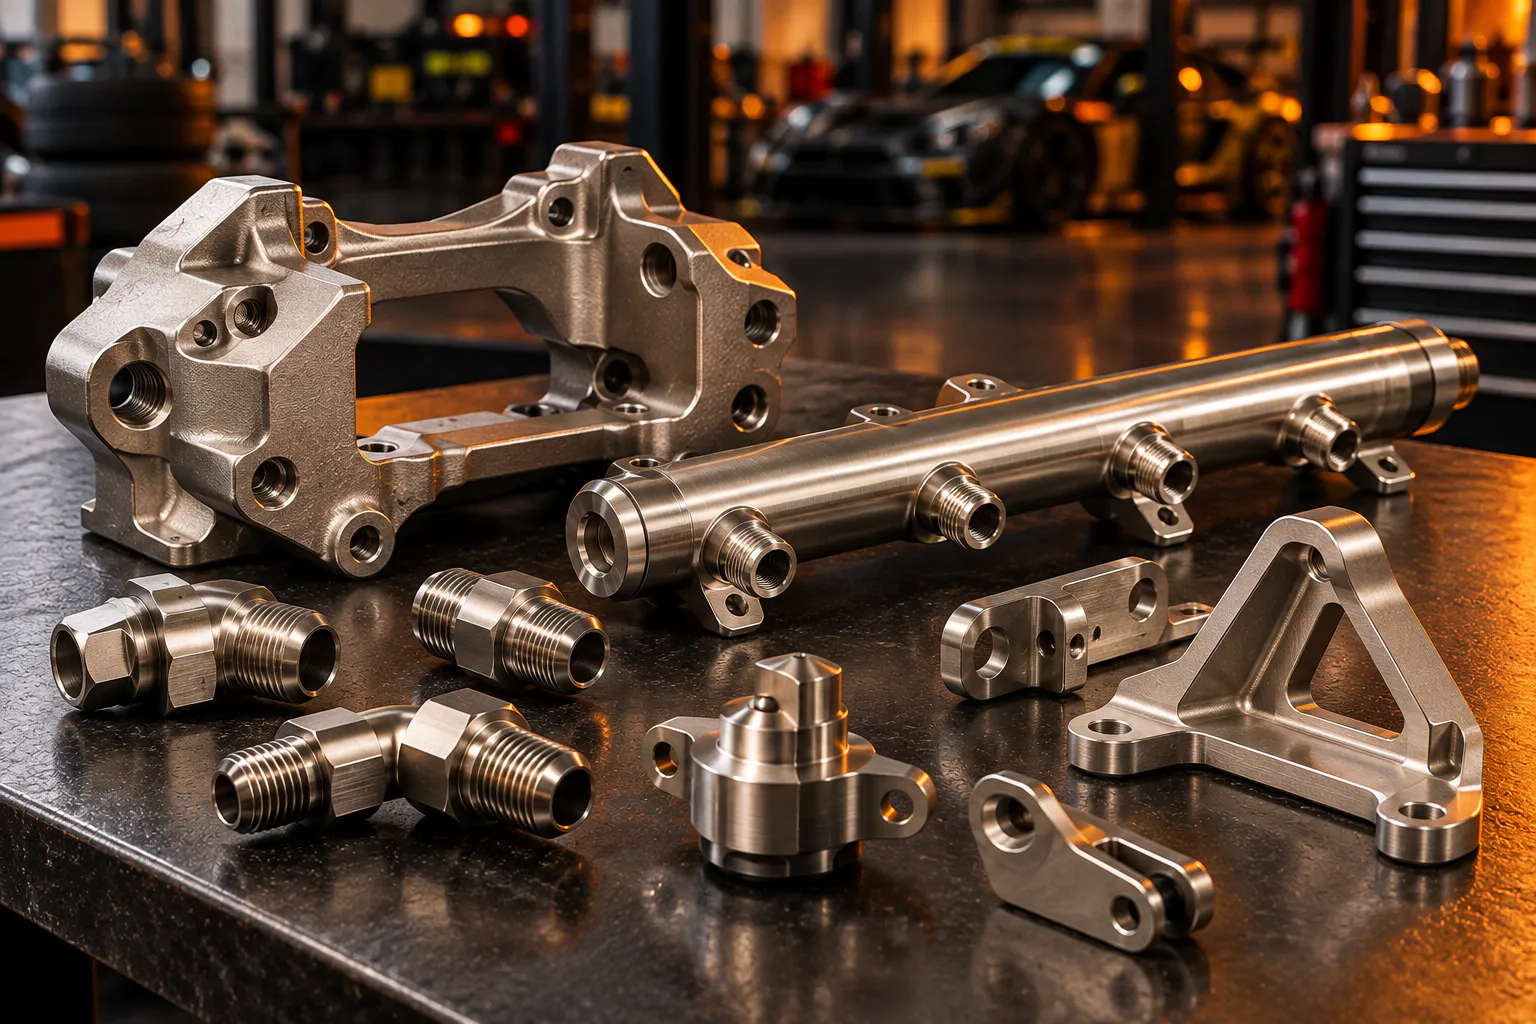
Brackets, fuel system fittings, brake parts and engine components protected from heat, fluids and road salt.
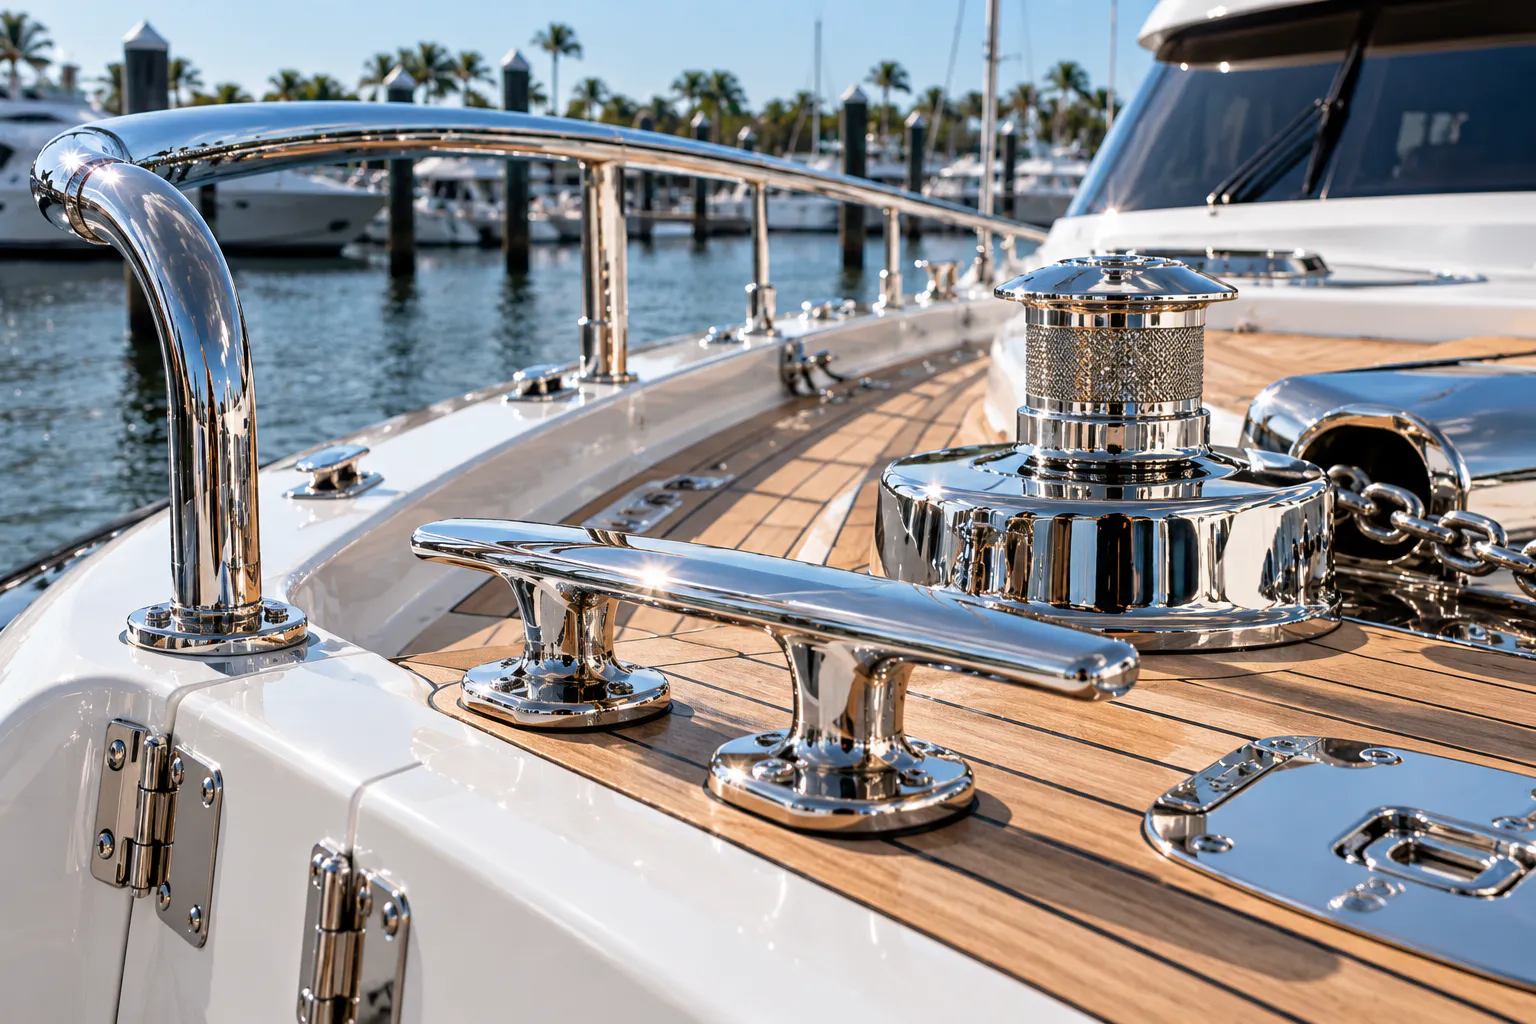
Fittings, pump parts and deck components where high phosphorus nickel stands up to constant salt exposure.
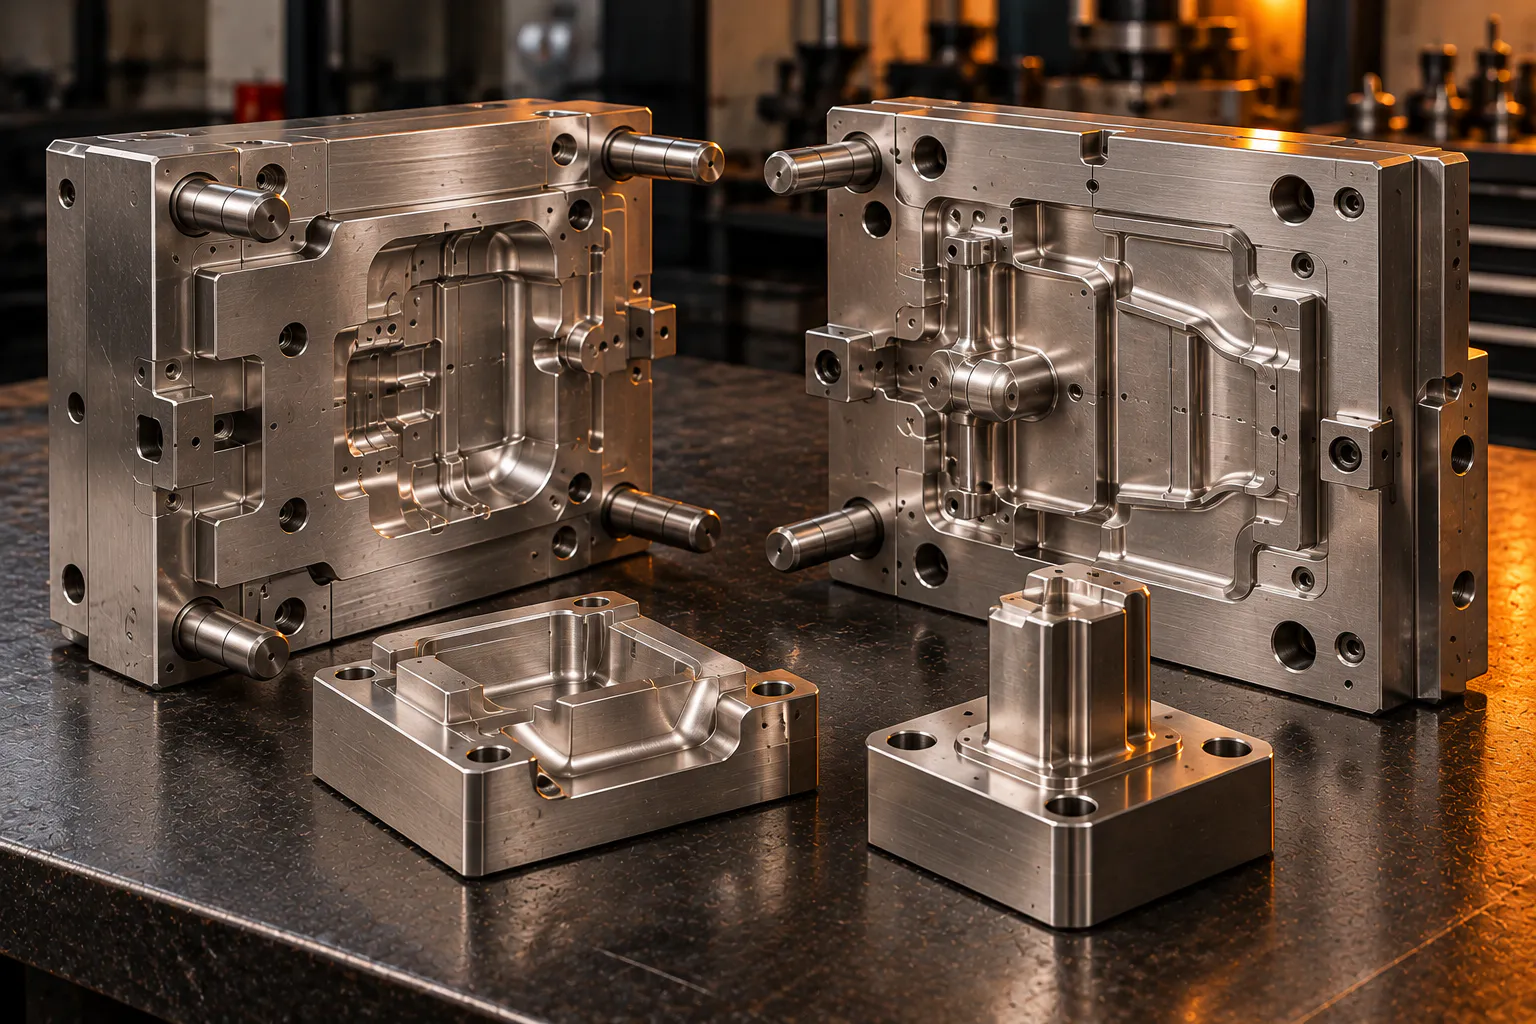
Plastic injection molds, dies and fixtures that need a hard surface, clean release and protection from corrosion.
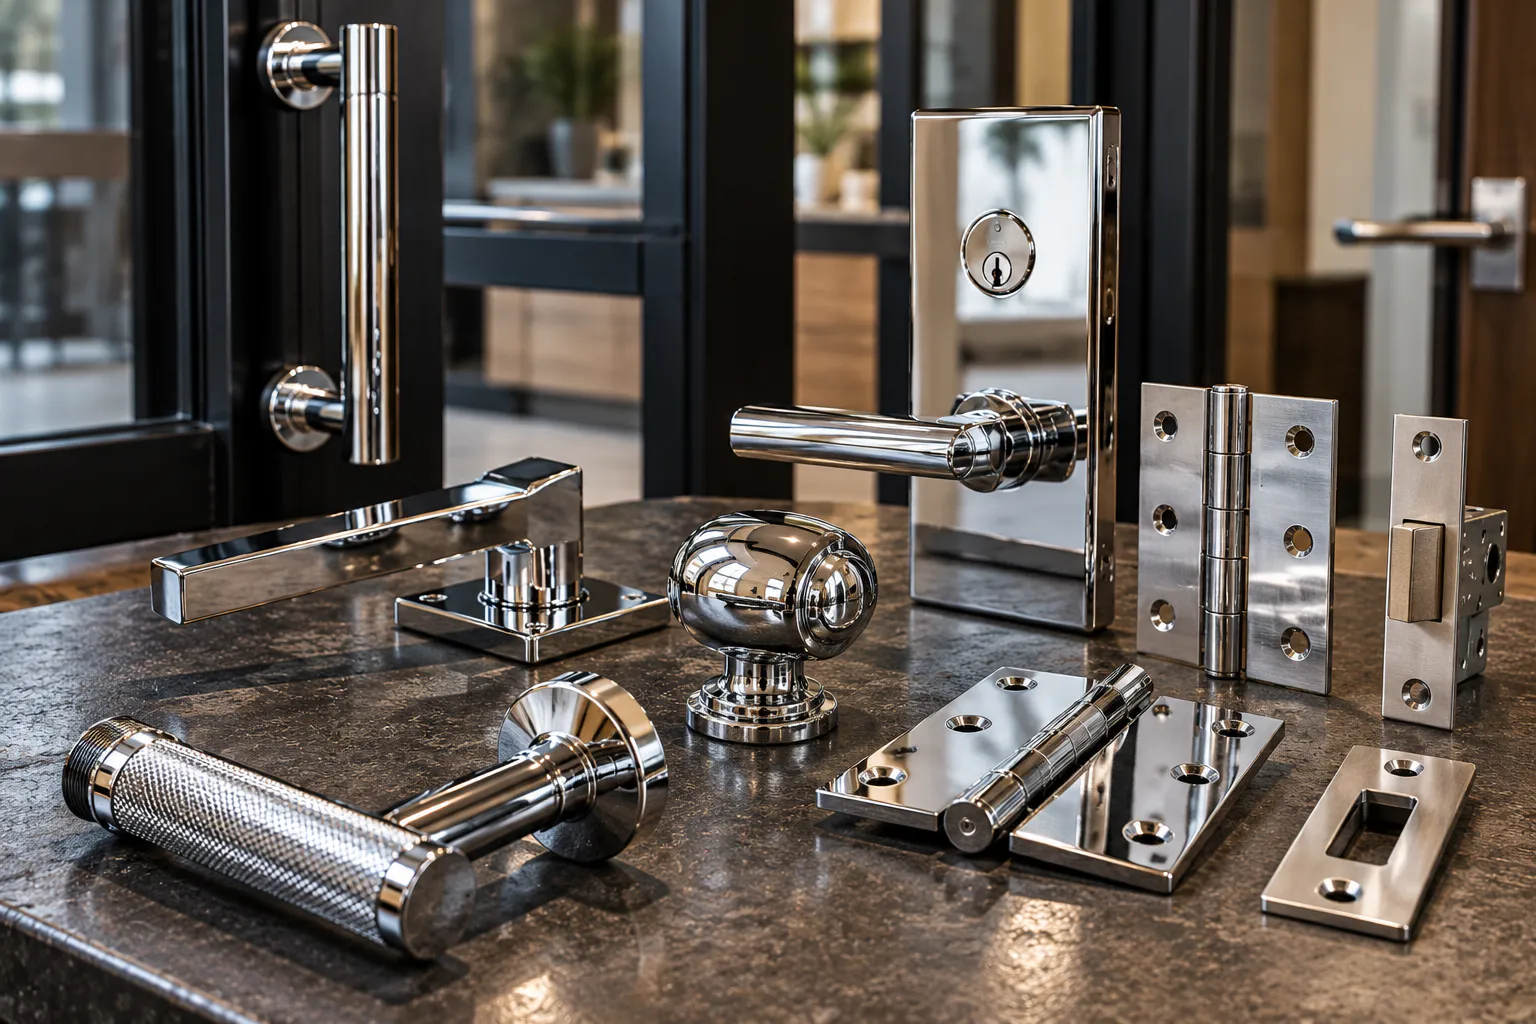
Threaded parts, hinges and fittings coated all the way into the threads for smooth assembly and lasting protection.
Drag the handle on any photo to compare the part as it arrived with the finished electroless nickel surface.
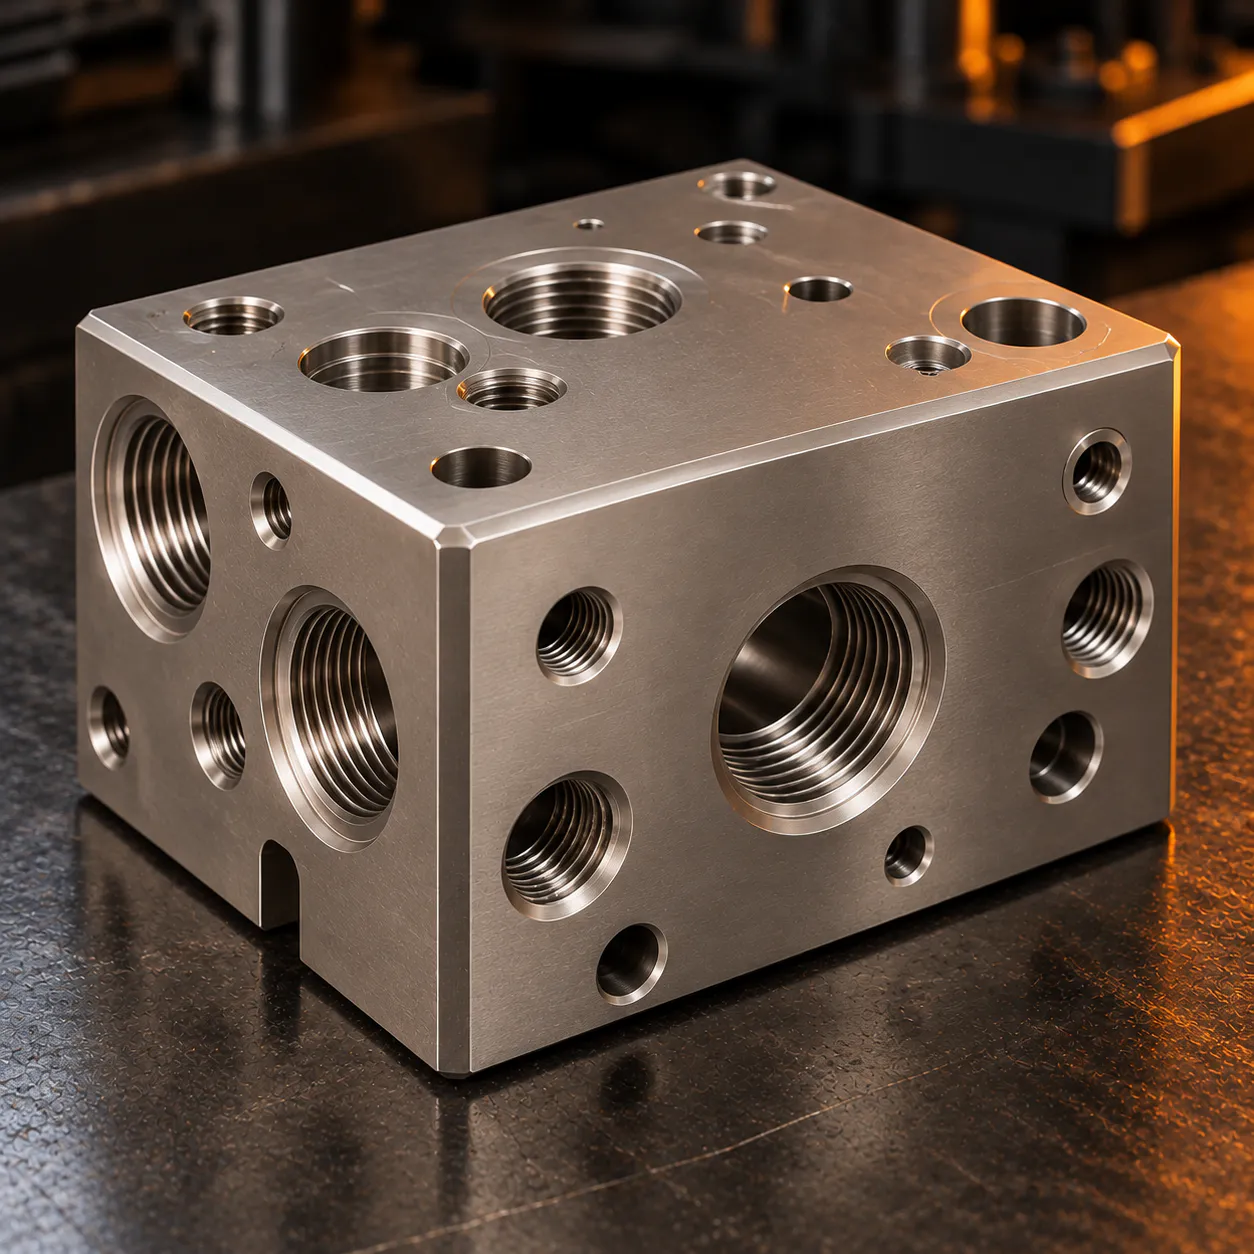
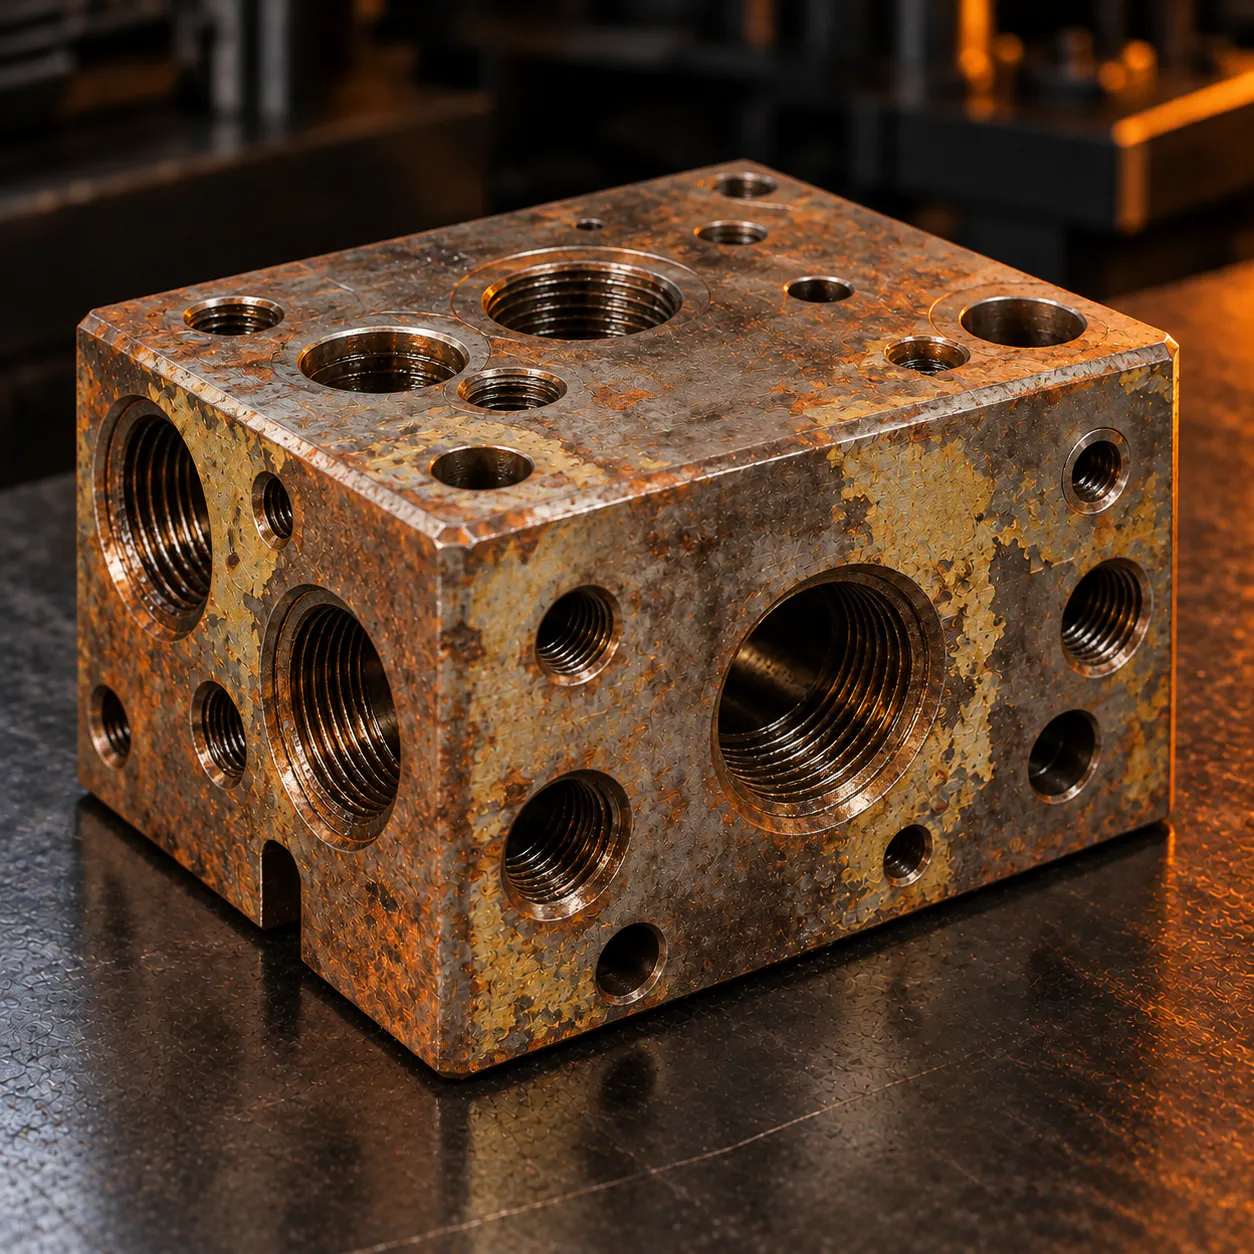 Before
Arrived with surface rust and a failed zinc finish. Stripped, cleaned and activated, then coated with medium phosphorus nickel for an even, corrosion resistant surface that kept the part within its fit.
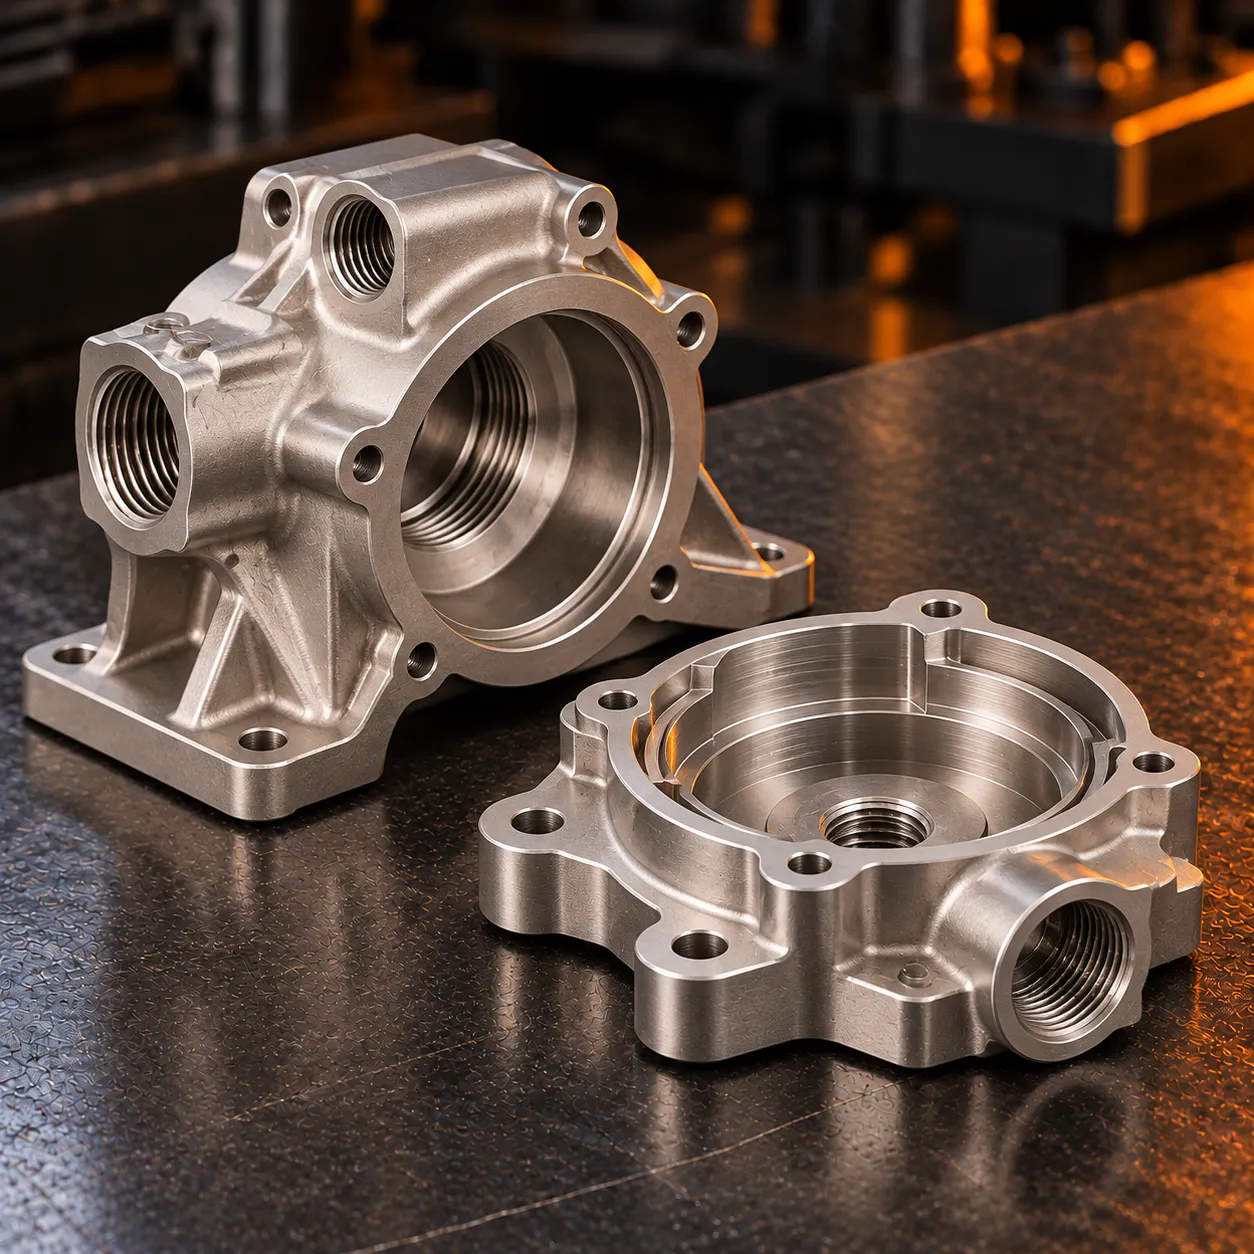
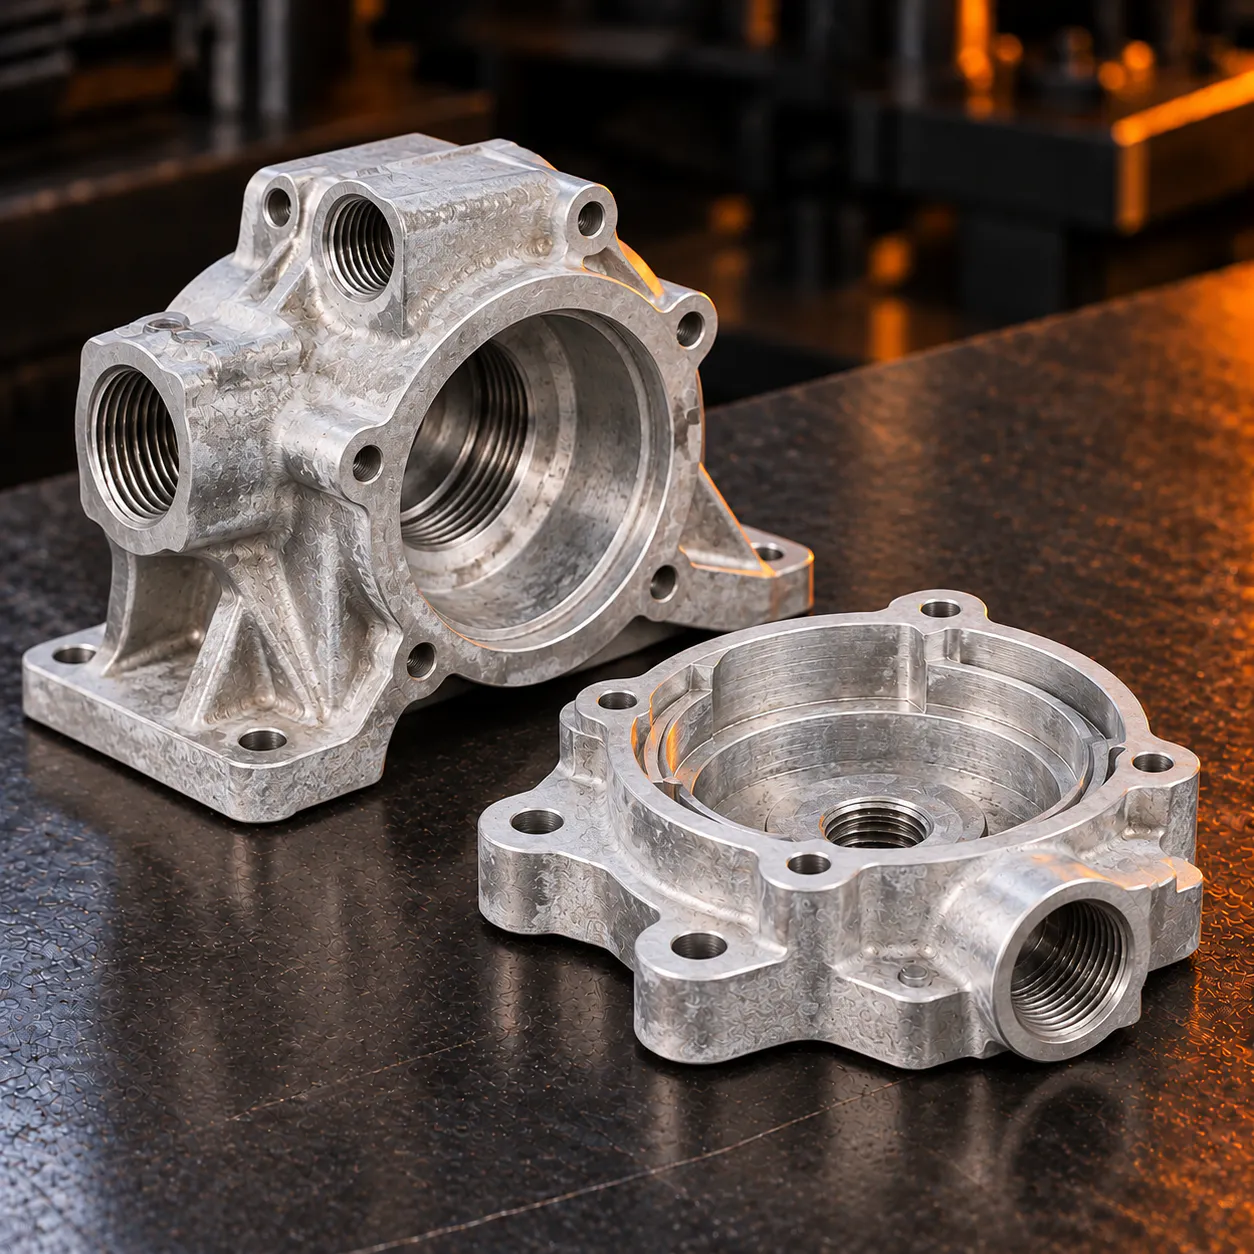 Before
Dull, oxidized housings with threaded ports. Each piece went through a zincate pretreatment and received high phosphorus nickel that reached every port and internal face.
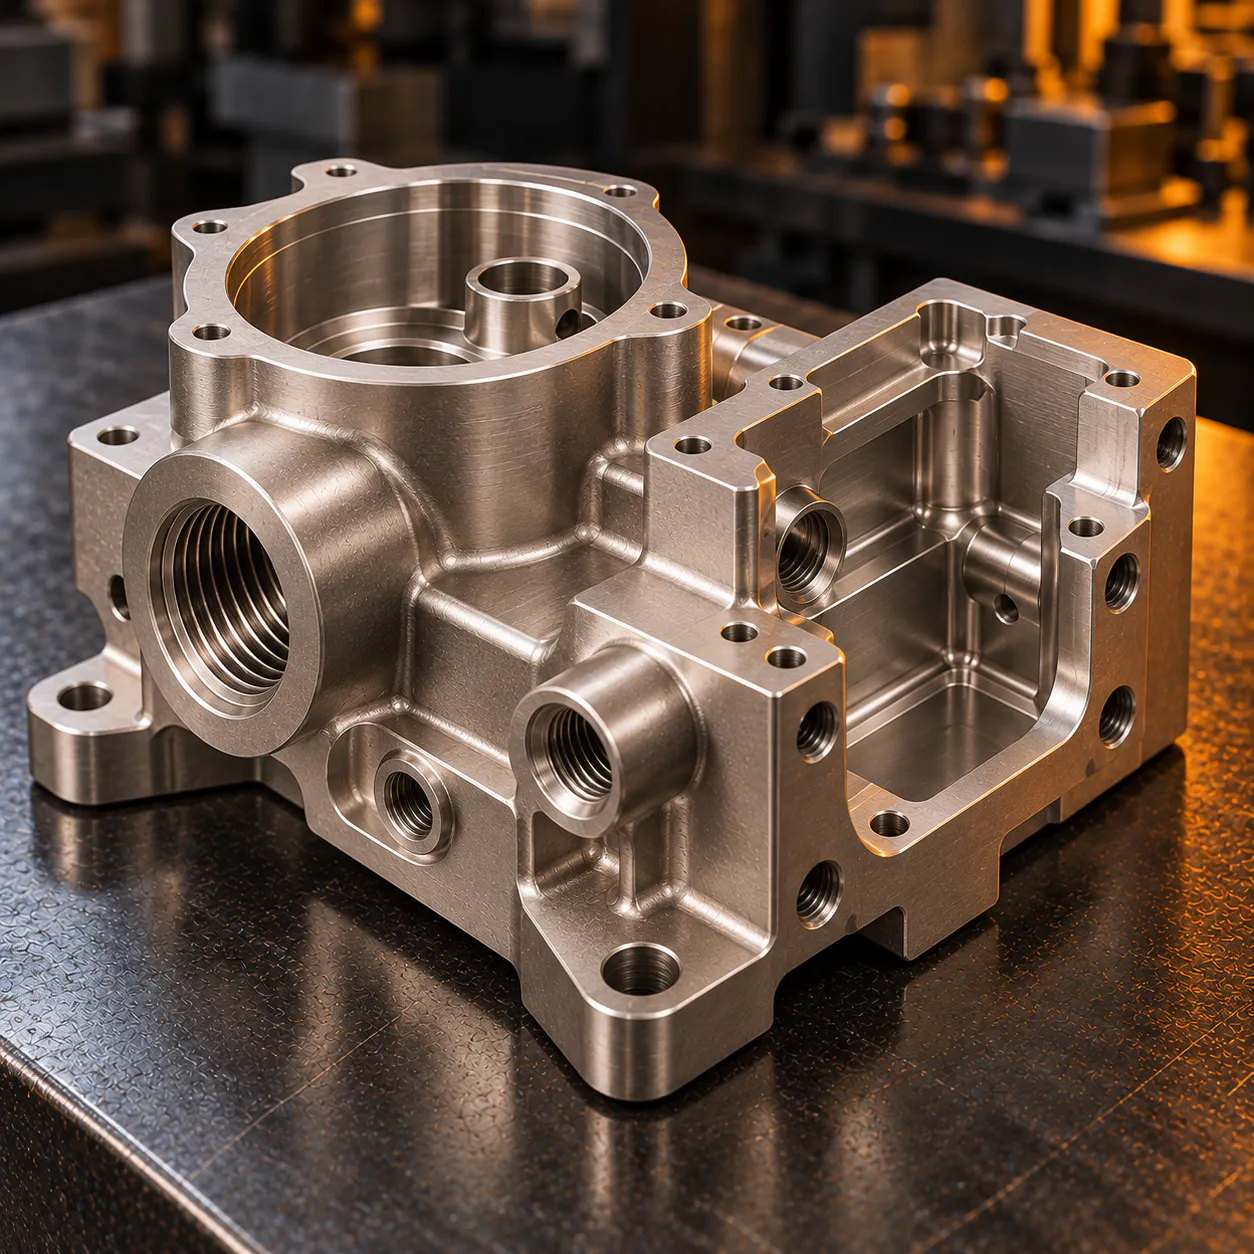
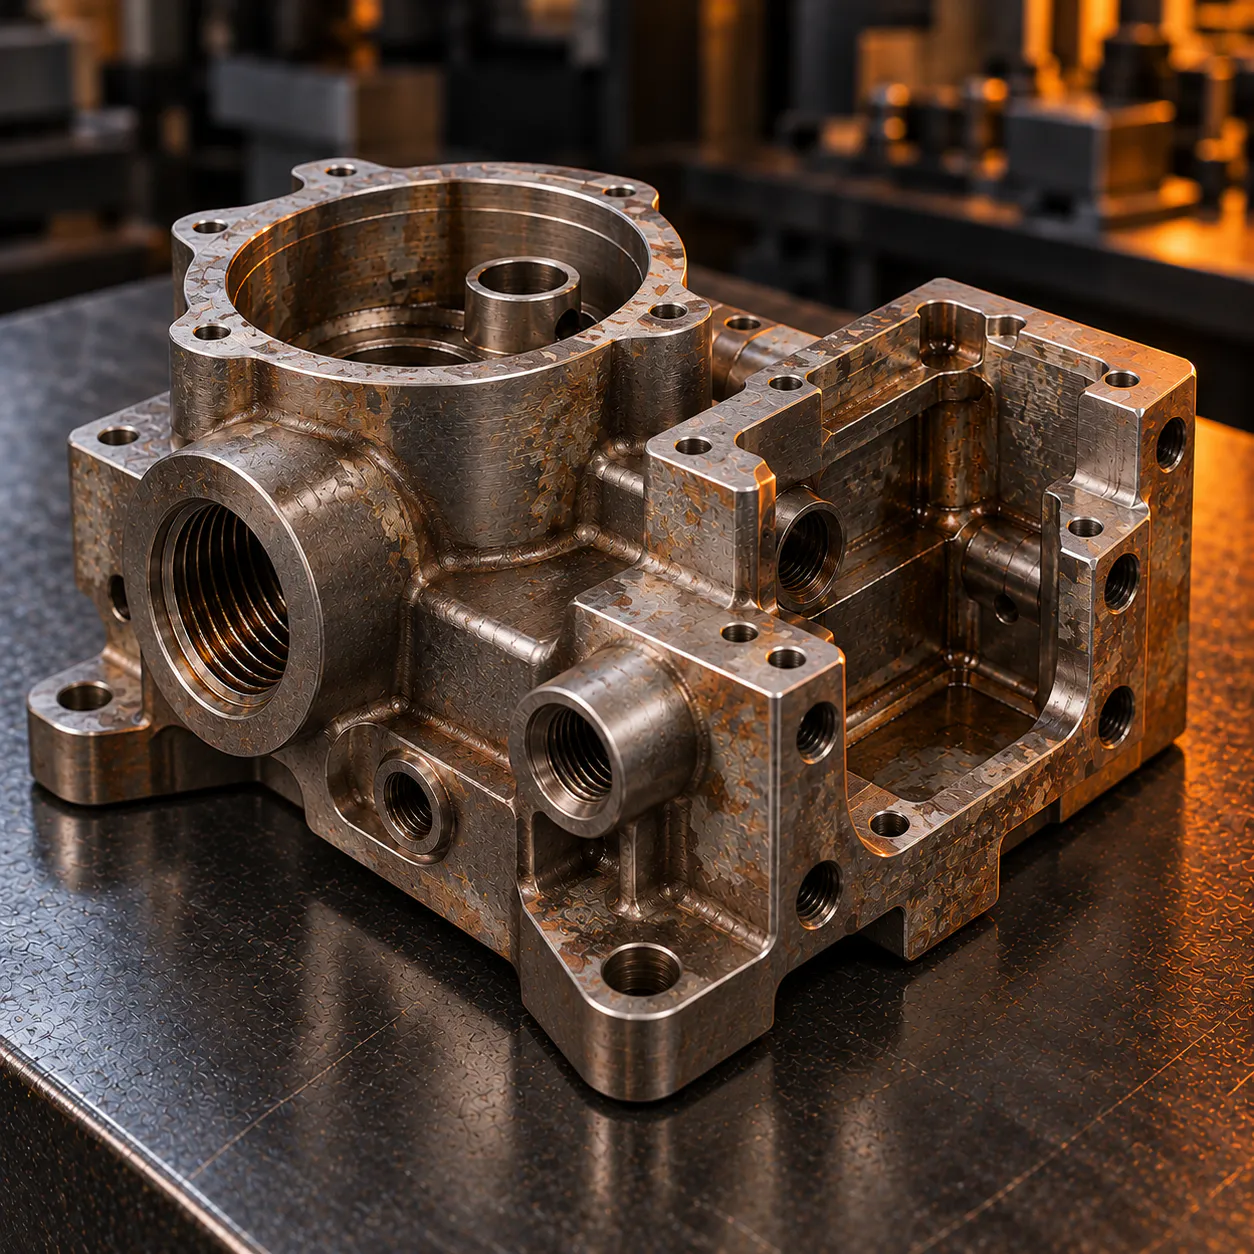 Before
Deep pockets and cross drilled passages that conventional plating could not reach evenly. Electroless nickel coated the inside and the outside at the same thickness.
Over three decades of plating, one shop in Oceanside.
Every part is stripped, prepped, plated and inspected in our own building, and our work comes with a 12 month workmanship guarantee. Send photos and we'll take it from there.
Functional plating only counts if the part works when it goes back into the assembly. That is the standard we inspect to on every order.
Bath chemistry, temperature and nickel content are monitored throughout the run so the deposit stays consistent from the first part to the last.
Steel, stainless and aluminum each follow their own cleaning and activation sequence, which is what keeps the coating bonded.
Coverage and coating thickness are checked against your requirement before parts are released for packing.
Finished parts are separated and packed so threads, sealing faces and machined surfaces arrive exactly as they left the tank.
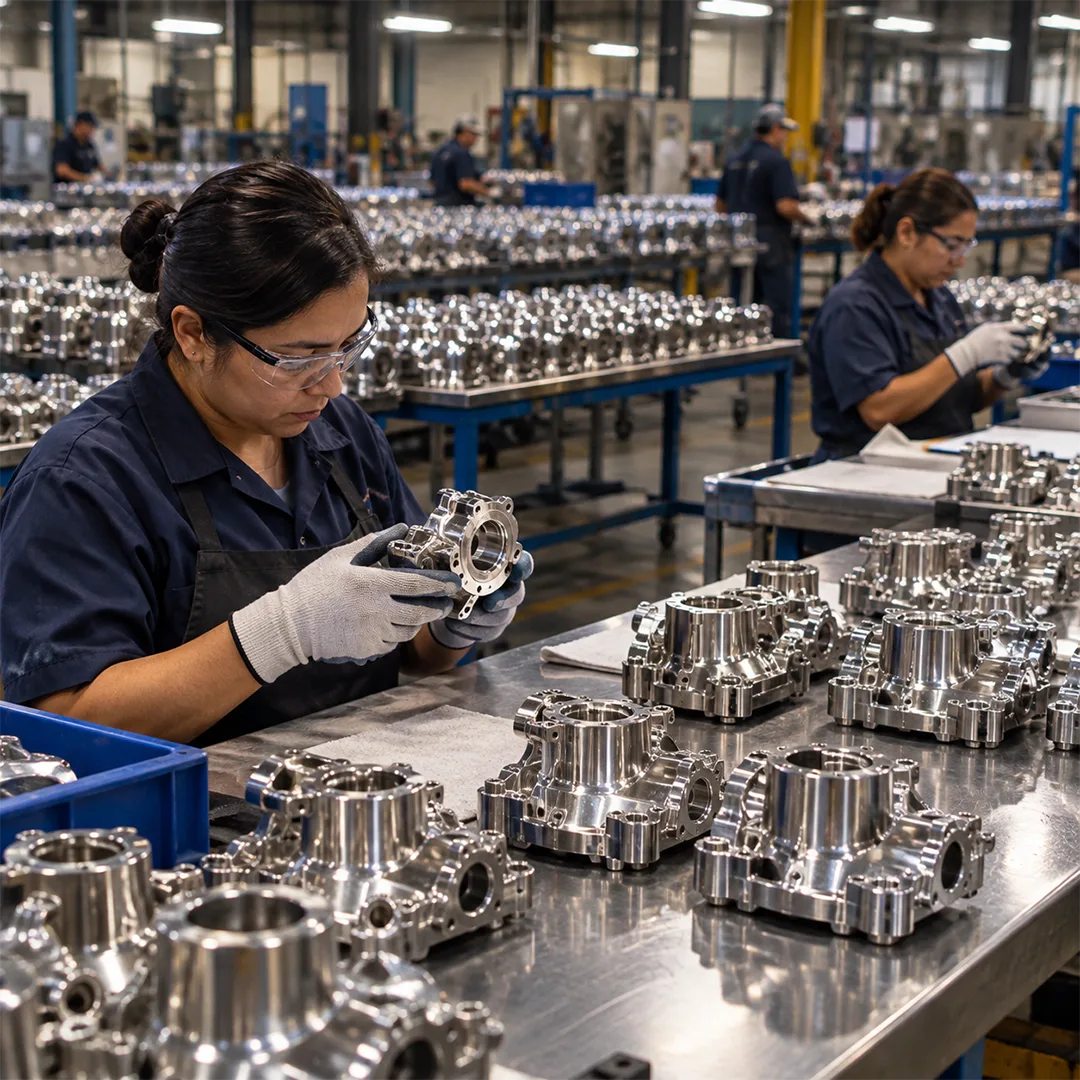
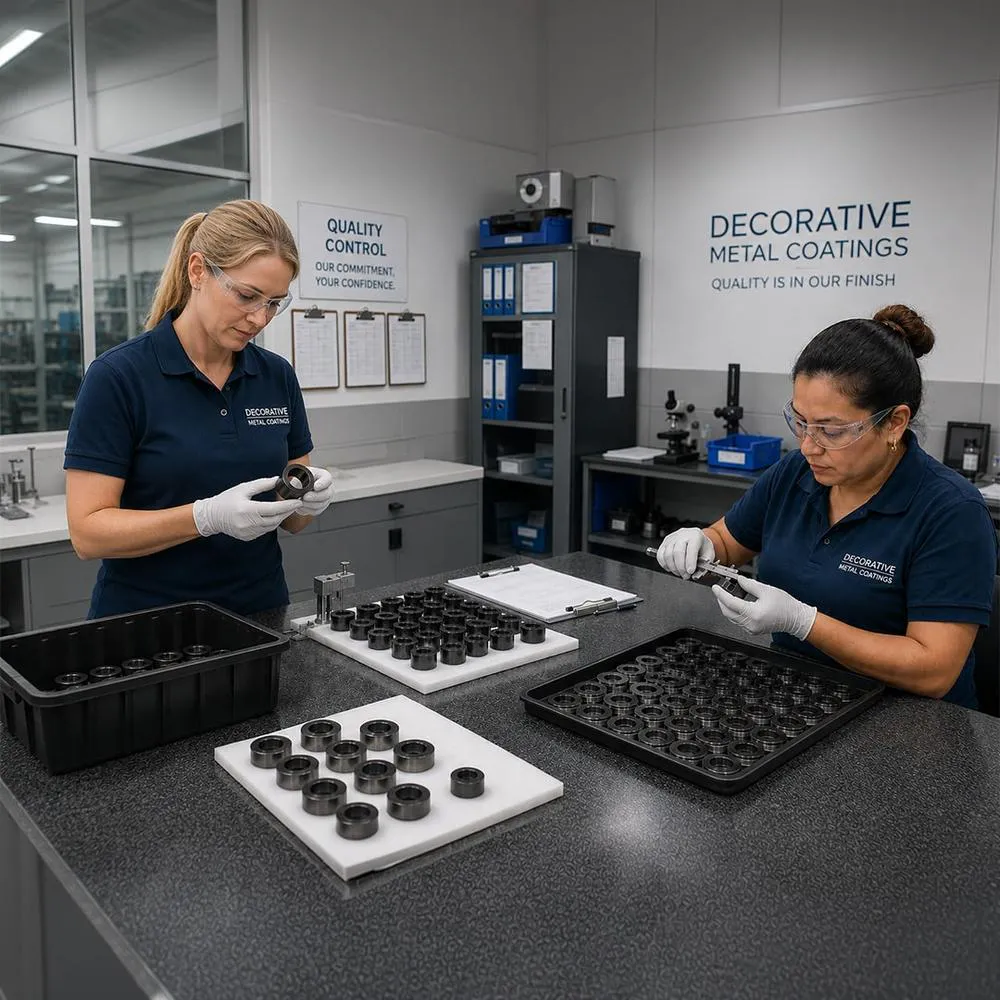
Since 1989 we have plated parts for machine shops, manufacturers, restorers and builders. Decorative work and functional coatings run under the same roof, with the same inspection standard.
Send a photo or drawing and receive a no obligation quote within 24 hours.
Every part leaves our shop backed by our craftsmanship guarantee. If you are not satisfied, we make it right.
Single prototypes or full production runs, shipped to us from any state and returned insured.
Most projects are completed within 3 to 5 weeks. Expedited Orders: 5 to 7 business days. Contact us for availability.
Preserve the deposit through storage and assembly.
Protect the deposit from scratches and dents during assembly. Use suitable fixtures and avoid dragging coated faces across benches or other components. Use the assembly drawing to identify which surfaces should not be clamped or gripped.
The correct maintenance method depends on the fluid, temperature and contact conditions. Confirm cleaning practices against the component specification and any equipment-maker guidance. Follow the approved assembly torque and avoid using impact tools on precision coated threads unless permitted.
Thickness is the other key number. Electroless nickel builds evenly, so the coating adds the same amount to every surface, inside diameters included. On a precision fit, that growth has to be planned for. Let us know the finished dimension you need, and whether any threads, bores or sealing faces should be masked and left bare.
Finally, mention quantity and timing. A single prototype and a recurring production run are scheduled differently, and knowing what is coming next lets us hold the same settings from batch to batch.
Electroless Nickel Gallery
Uniform electroless nickel on machined, threaded and complex parts, from valve bodies and molds to marine fittings and hardware.
Decorative Metal Coatings processes electroless nickel orders at its Oceanside, California facility. Eligible projects from Fort Collins, CO, and elsewhere in the United States may be shipped after the quote and receiving instructions are confirmed. Protect precision surfaces and identify each part number.
Send photos or drawings, the material and the quantity. You receive a written quote and lead time, usually the same business day. Always wait for a quote number before shipping.
Bag or wrap each part separately, cap threads and ports when you can, and keep parts from rubbing against each other. Use plenty of padding on every side of the box.
Declare the real value with the carrier and email us the tracking number so we can log your parts the day they arrive.
Once plating and inspection are complete, we pack the parts in clean materials and ship them back insured, or hold them for pickup.
Every electroless nickel order is cleaned, plated and inspected in our own facility in North County San Diego.
Electroless nickel, chrome and metal finishing in San Diego County since 1989.
DMC's plating operations are based in Oceanside, California. Contact the team for a quote and receiving instructions before arranging shipment from another location.
Other cities appearing in the supplied service-area list include:
Frequently Asked Questions
These answers cover coating chemistry, substrate review, dimensions and practical details that can help define a plating request.
Aluminum may be evaluated, but the exact alloy and surface condition matter because preparation is substrate-specific. Share the grade and any prior finish before suitability is confirmed.
Masking may be possible when certain surfaces must remain free of deposit. Mark those areas on the drawing and explain whether the reason is dimensional fit, electrical contact or joining.
Yes. State the required minimum or range and identify where thickness must be measured. Include the governing specification or test method if one applies.
Documentation requirements should be stated in the quote request. Identify any thickness readings, test reports, certificates or customer forms required for the order.
Yes. The deposit adds material to coated surfaces. Identify bores, threads, mating faces and all critical tolerances, and clarify whether dimensions apply before or after plating.
The shop is open Monday to Friday from 8 AM to 5 PM and Saturday from 9 AM to 2 PM. We're closed on Sunday. Shipments are received Monday to Friday, 8 AM to 4 PM Pacific.
Usually, yes. Send a photo of the piece you want to match, or ship it along with your parts as a sample. We adjust the finish until the new work sits right next to the old.
When the work is done and inspected, we pack your parts in fresh materials and ship them back insured. If you're close to Oceanside, you're welcome to pick them up instead.