

Gloss and Satin Colors
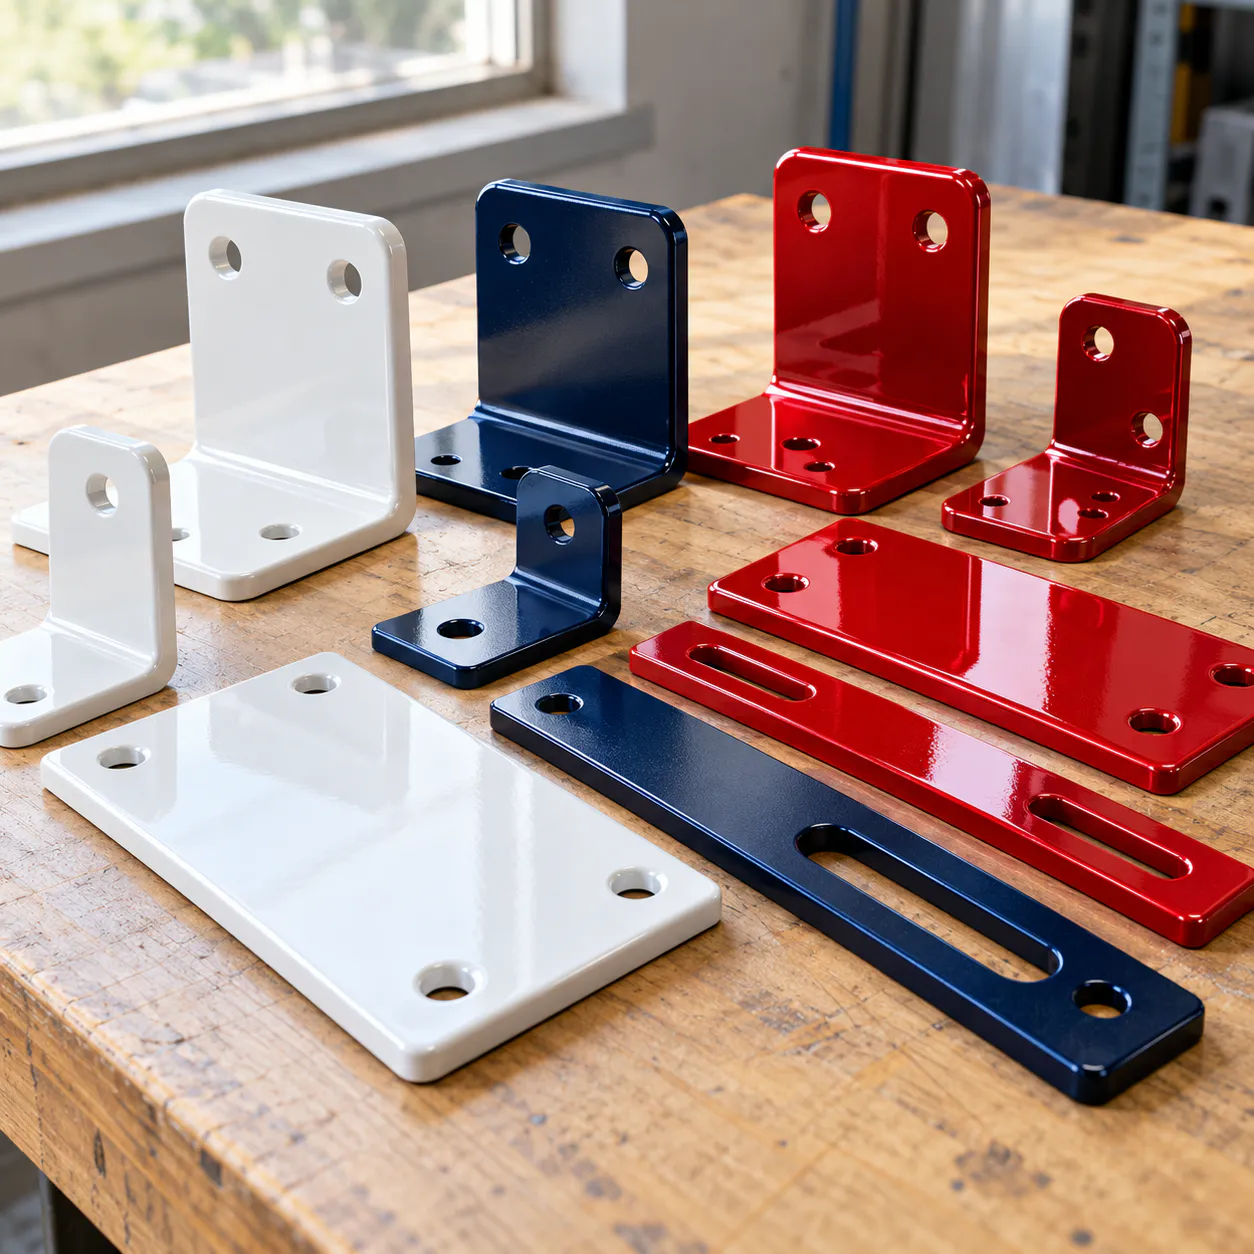
Solid colors with a smooth, even sheen. Gloss gives a deep, wet look, while satin softens reflections and keeps fingerprints from showing on parts people touch.
For projects connected with Indian Wells, California, Decorative Metal Coatings reviews eligible components for powder coating at its Oceanside facility. The first step is to understand the part: its base metal, dimensions, current surface, intended environment and the areas that must remain uncoated. This information helps determine whether the component can tolerate preparation and curing.
Working parts need coating decisions that respect fit and function. Equipment components require a finish plan built around their job. For Indian Wells Projects
Indian Wells projects may include tool housings and equipment components. These parts are not all prepared in the same way. Steel, aluminum, cast iron, stainless steel, galvanized steel, brass, copper and suitable plated parts each require a substrate-specific review. Powder coating is performed in Oceanside, not at a local shop in Indian Wells.
Contact surfaces and tolerances should be marked before processing. Gloss, satin, semi-gloss, matte, flat black, fine texture, wrinkle, hammertone, metallic, candy, clear gloss and clear matte may be considered when suitable. Clear powder may also be considered over polished or plated metal when the complete system is suitable. Primer with a UV-stable topcoat may be evaluated for certain outdoor applications.
Send photographs from several angles, quantity, approximate dimensions, base-metal details and the target color or sheen. Identify threads, bores, bearing seats, ground points and mating surfaces that must stay bare. DMC reviews the information and provides a written quote for approval before shipment.
Being a plating shop first gives us one more advantage. We can polish or plate a part and then seal it under clear powder, or combine powder coated and plated pieces on the same project so every finish comes from the same place and the colors line up.
Gloss, satin, semi-gloss, matte, flat black, fine texture, wrinkle, hammertone, metallic, candy, clear gloss and clear matte may be considered when suitable.
Solid colors with a smooth, even sheen. Gloss gives a deep, wet look, while satin softens reflections and keeps fingerprints from showing on parts people touch.
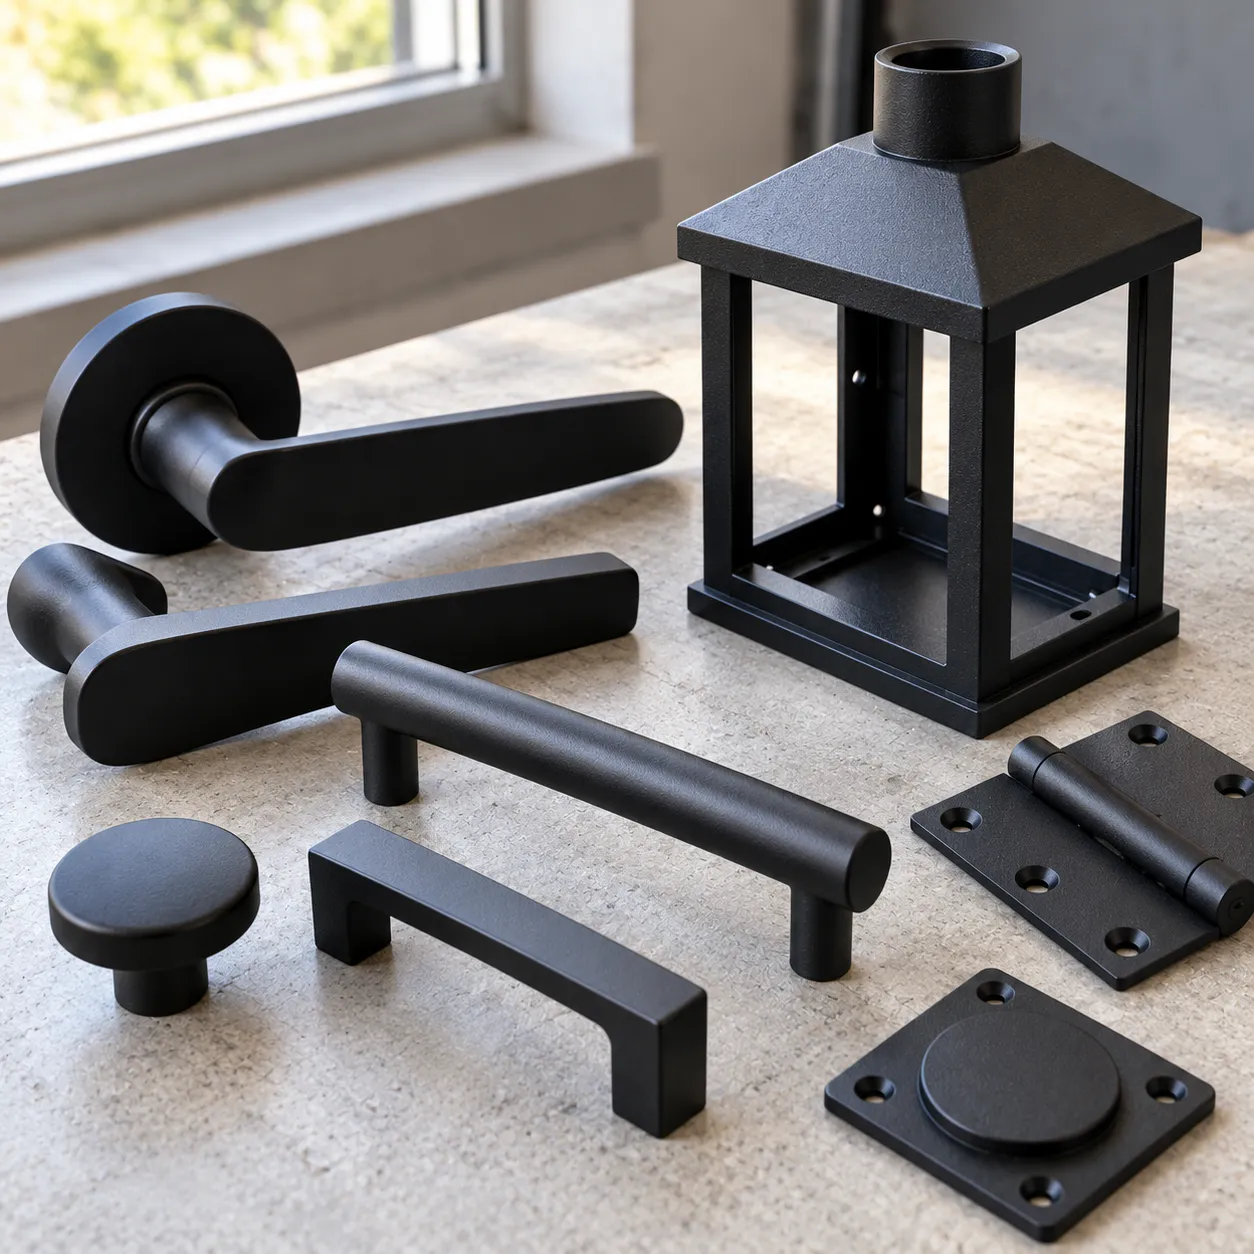
Low sheen finishes with a modern, understated look. Flat black is our most requested color for architectural hardware, light fixtures and product parts.
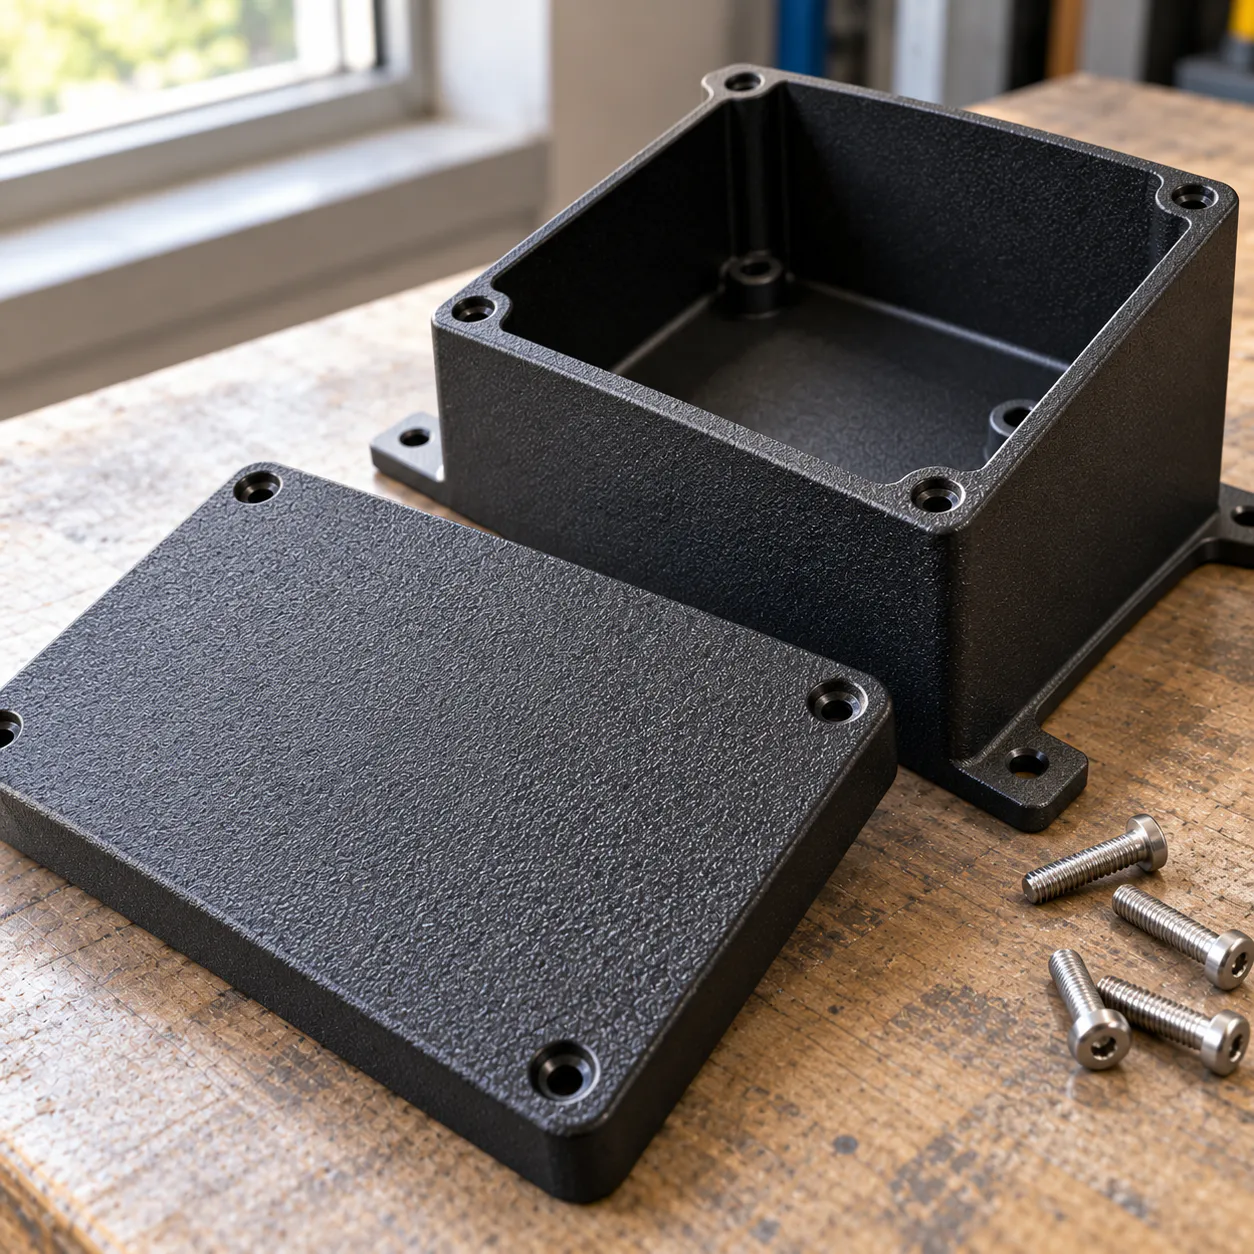
A fine sand or wrinkle texture that hides small casting flaws and handling marks. A practical choice for housings, tool parts and anything that gets gripped.
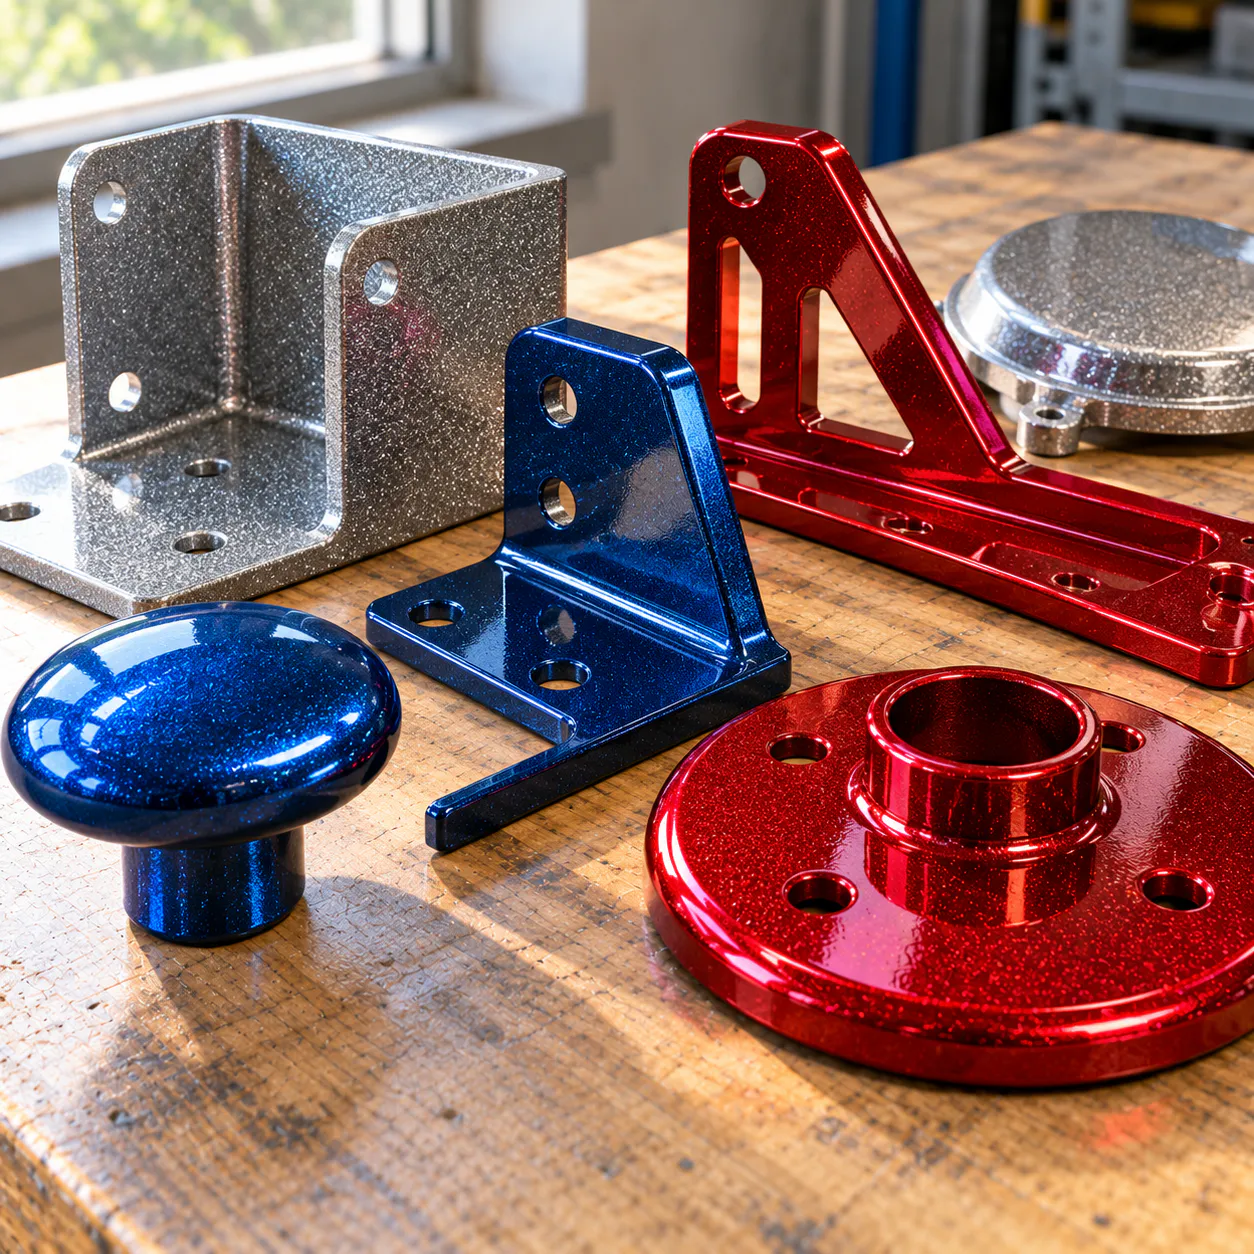
Powders with suspended metallic flake, or a translucent candy color layered over a silver base for depth. Often finished with a clear topcoat for extra protection.
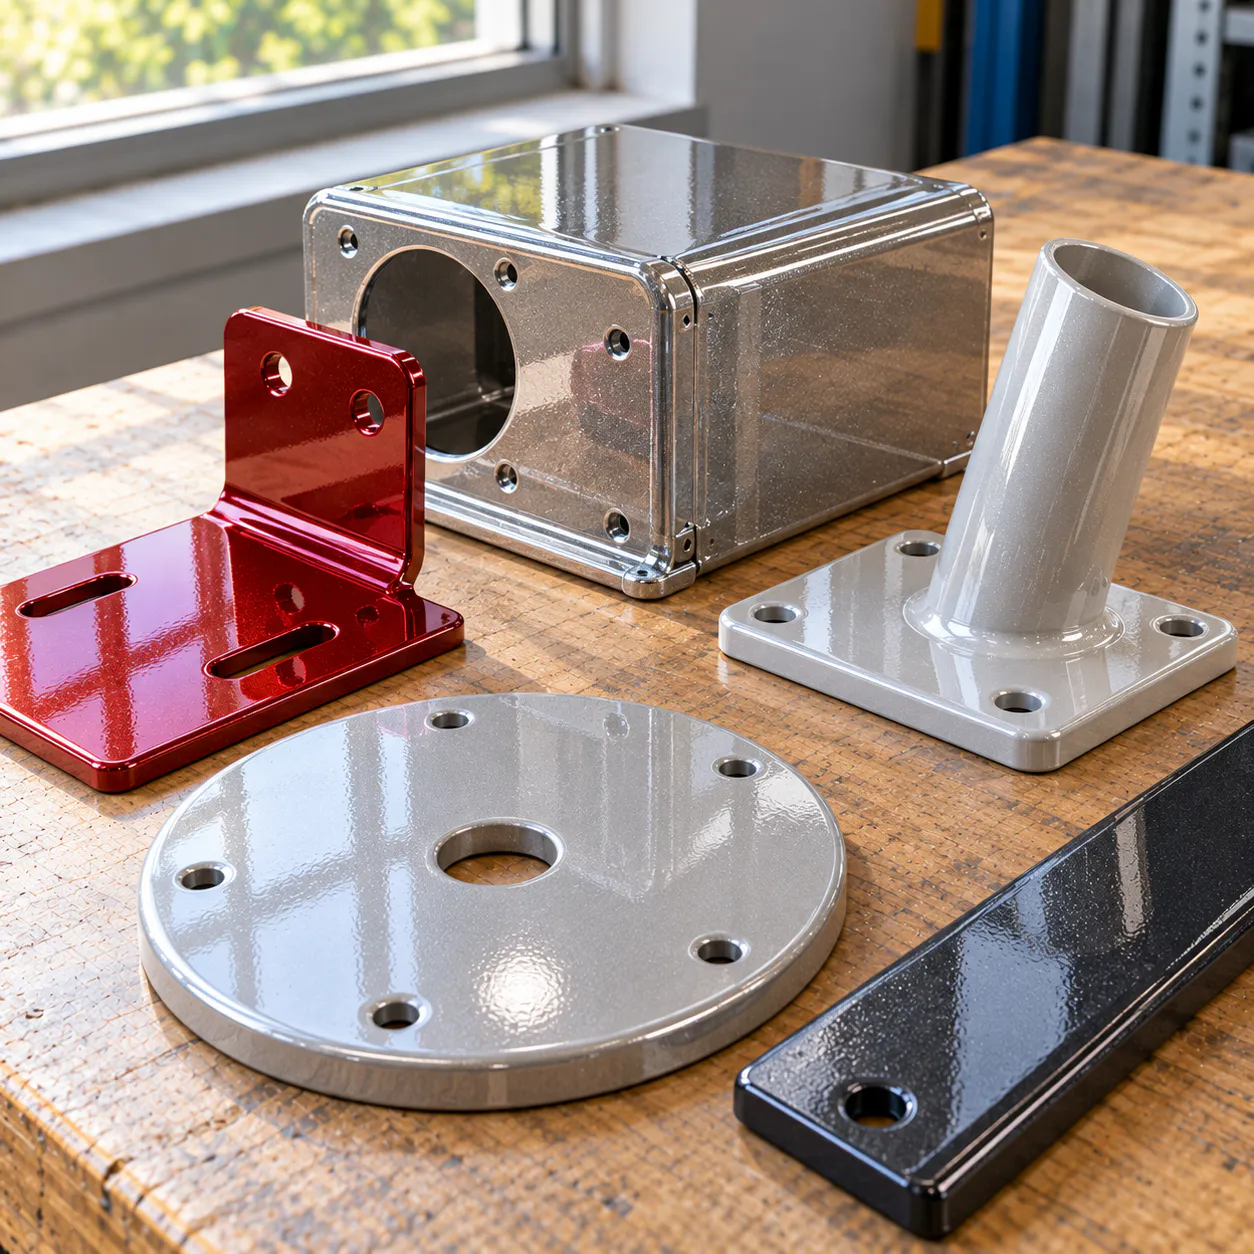
A clear powder layer over polished aluminum, brass, copper or plated parts. It keeps the natural metal look while protecting it from tarnish and fingerprints.
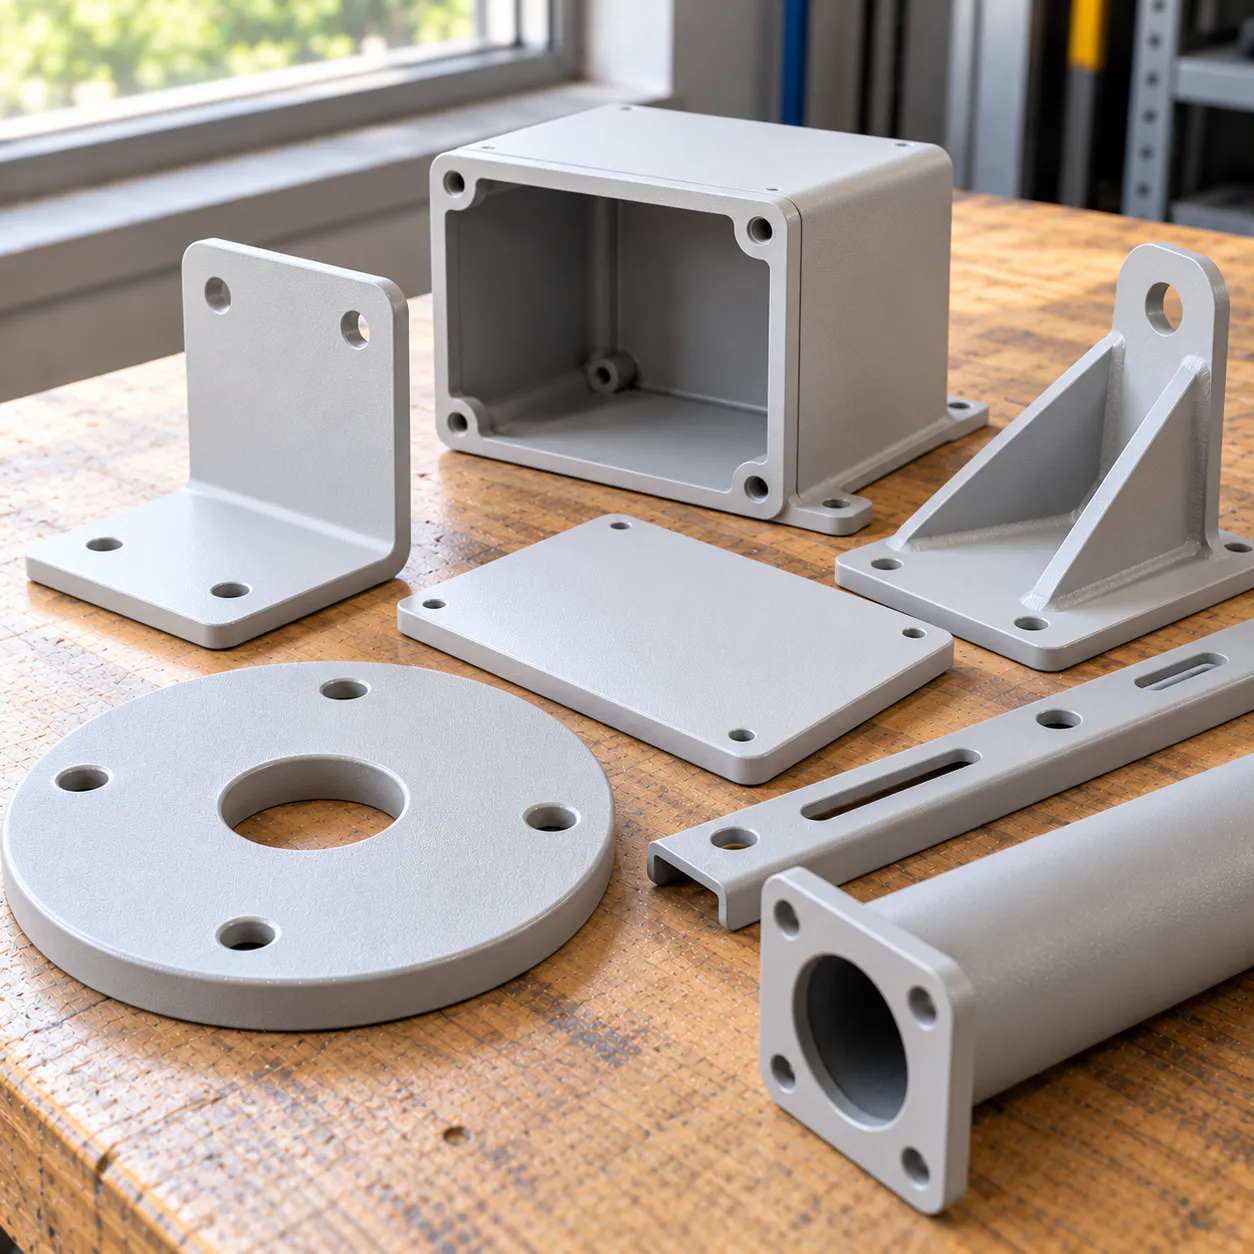
Two coat systems with a corrosion resistant primer under a UV stable topcoat. Built for coastal air, patios and parts that spend their life outside.
Tooling and equipment are reviewed for substrate condition, cleaning, stripping, media blasting and pretreatment as needed. Powder requires a conductive part that can be grounded and tolerate the curing temperature.
Show us the parts, tell us the quantity and the color or sheen you have in mind.
We confirm the base metal, the prep and any masking, then send a written quote within 24 business hours.
Once preparation and masking are complete, powder is applied and heat-cured. Rubber, plastic, glass, gaskets, bearings, seals and electrical components must be removed when they cannot withstand the process. Mark all contact and fit surfaces before work begins.
Old coatings and rust come off, the metal is blasted to a clean profile and pretreated for adhesion.
Powder is applied, cured to the manufacturer schedule, checked for coverage and sheen, then packed.
A quick reference to the powder finishes we apply, the options that go with them and the kinds of parts that come through the shop most often.
Slide the handle across each photo to compare the part as we received it with the same part after powder coating.
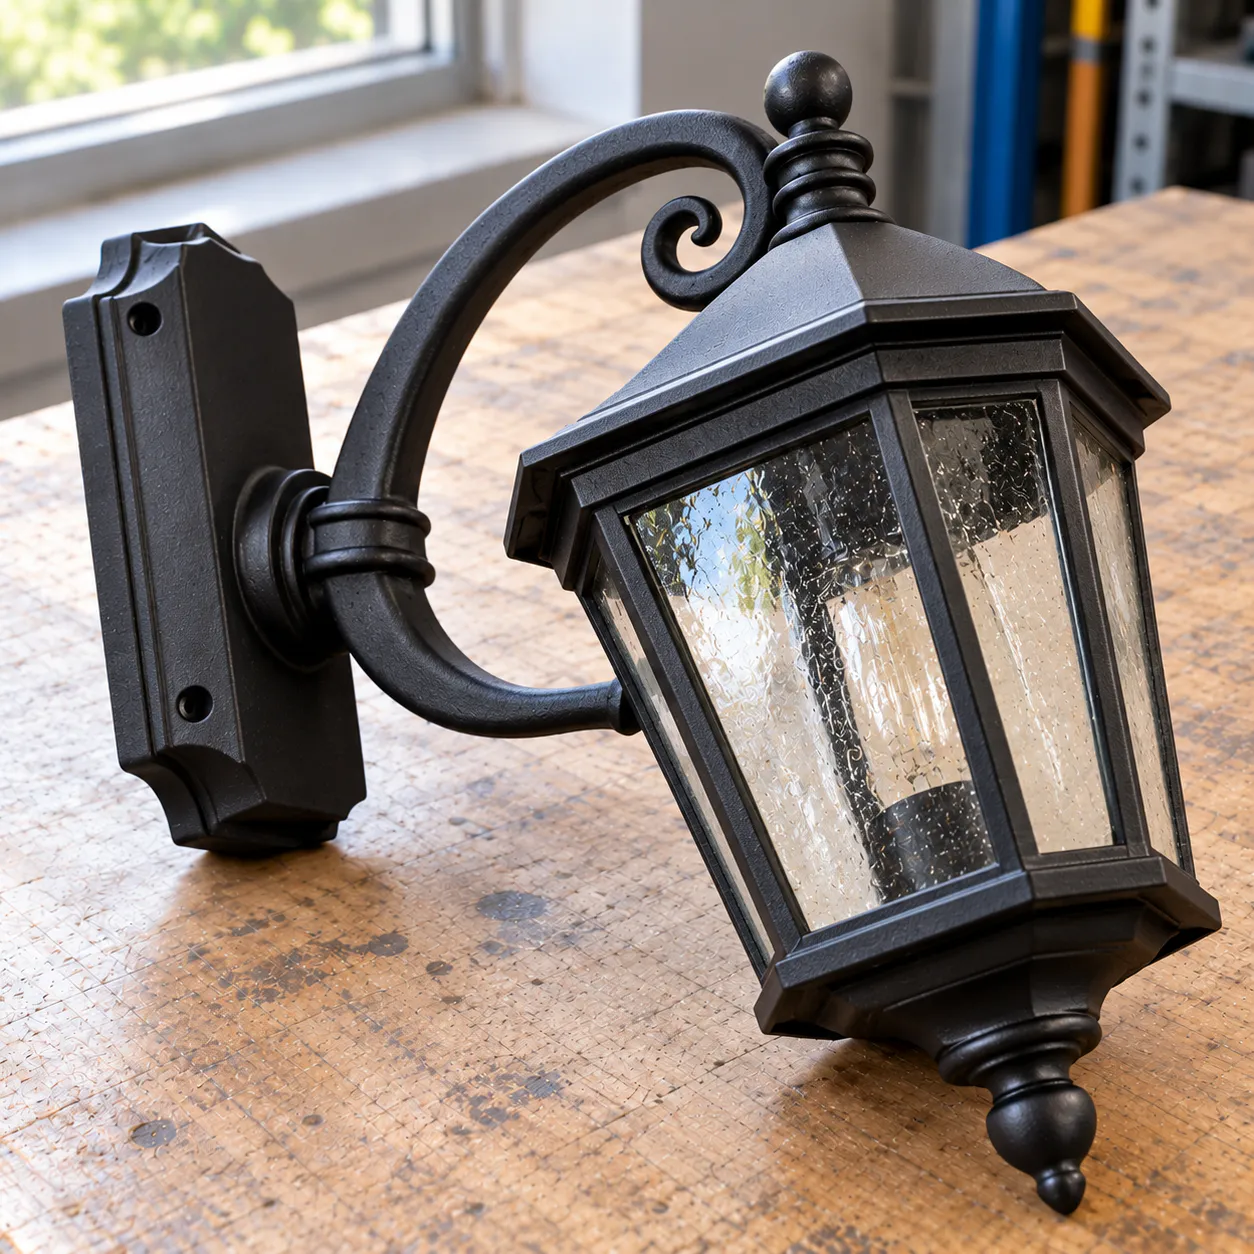
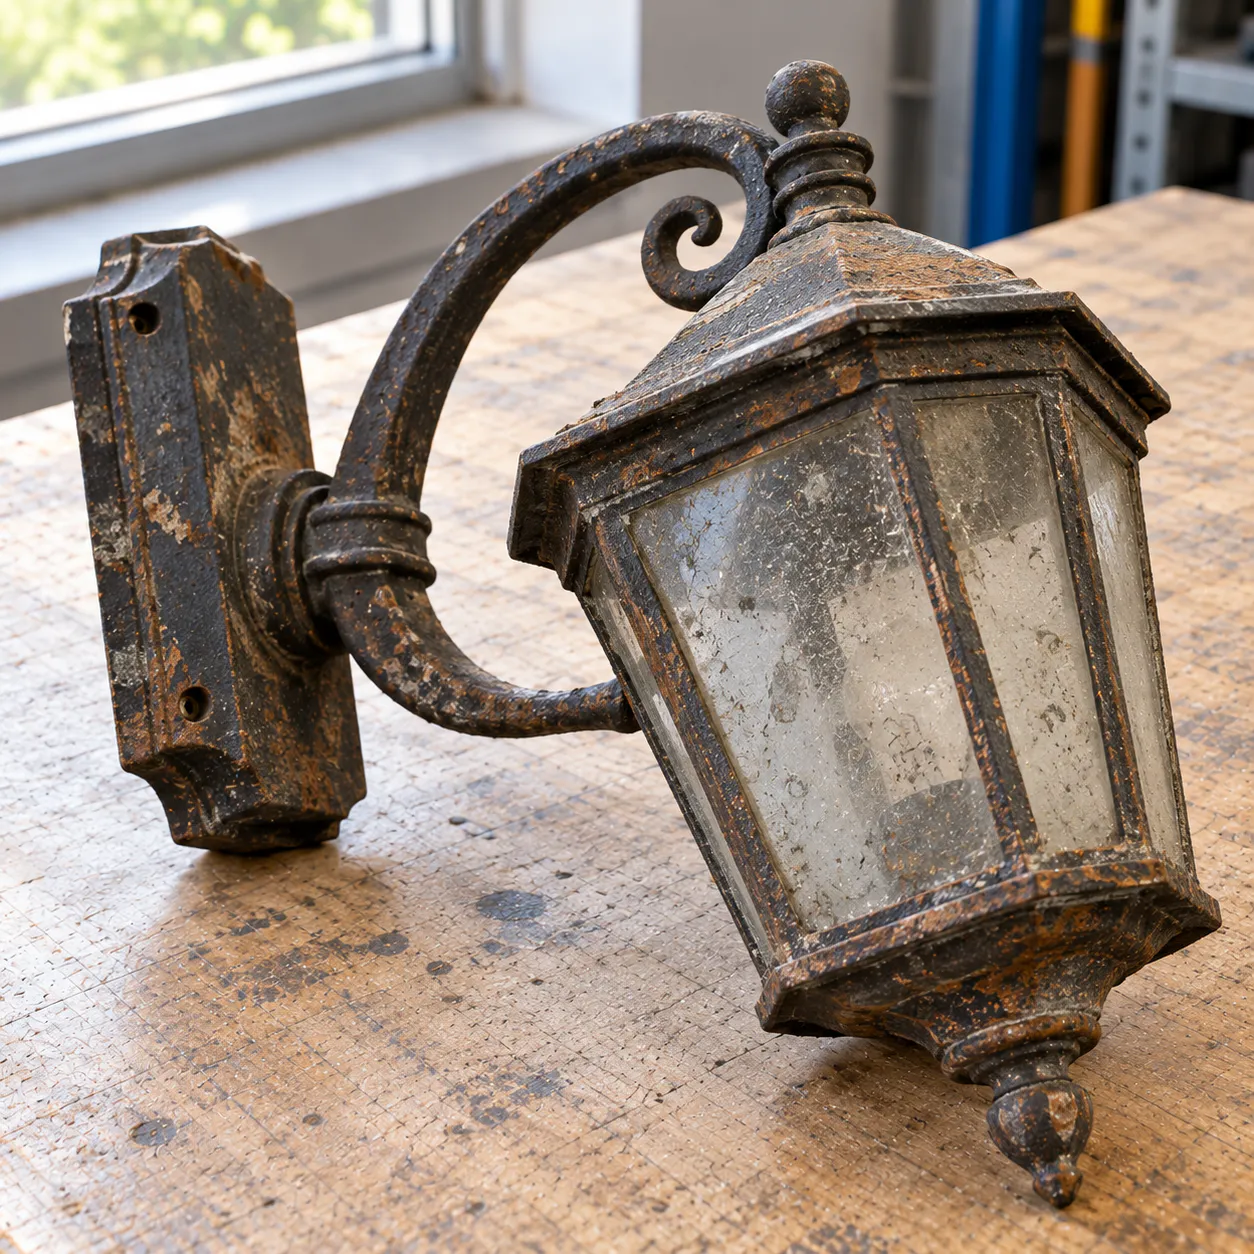 Before
Years of sun had turned the original paint chalky and gray. Stripped, blasted and recoated in a fine textured black that will hold its color on a sunny wall.
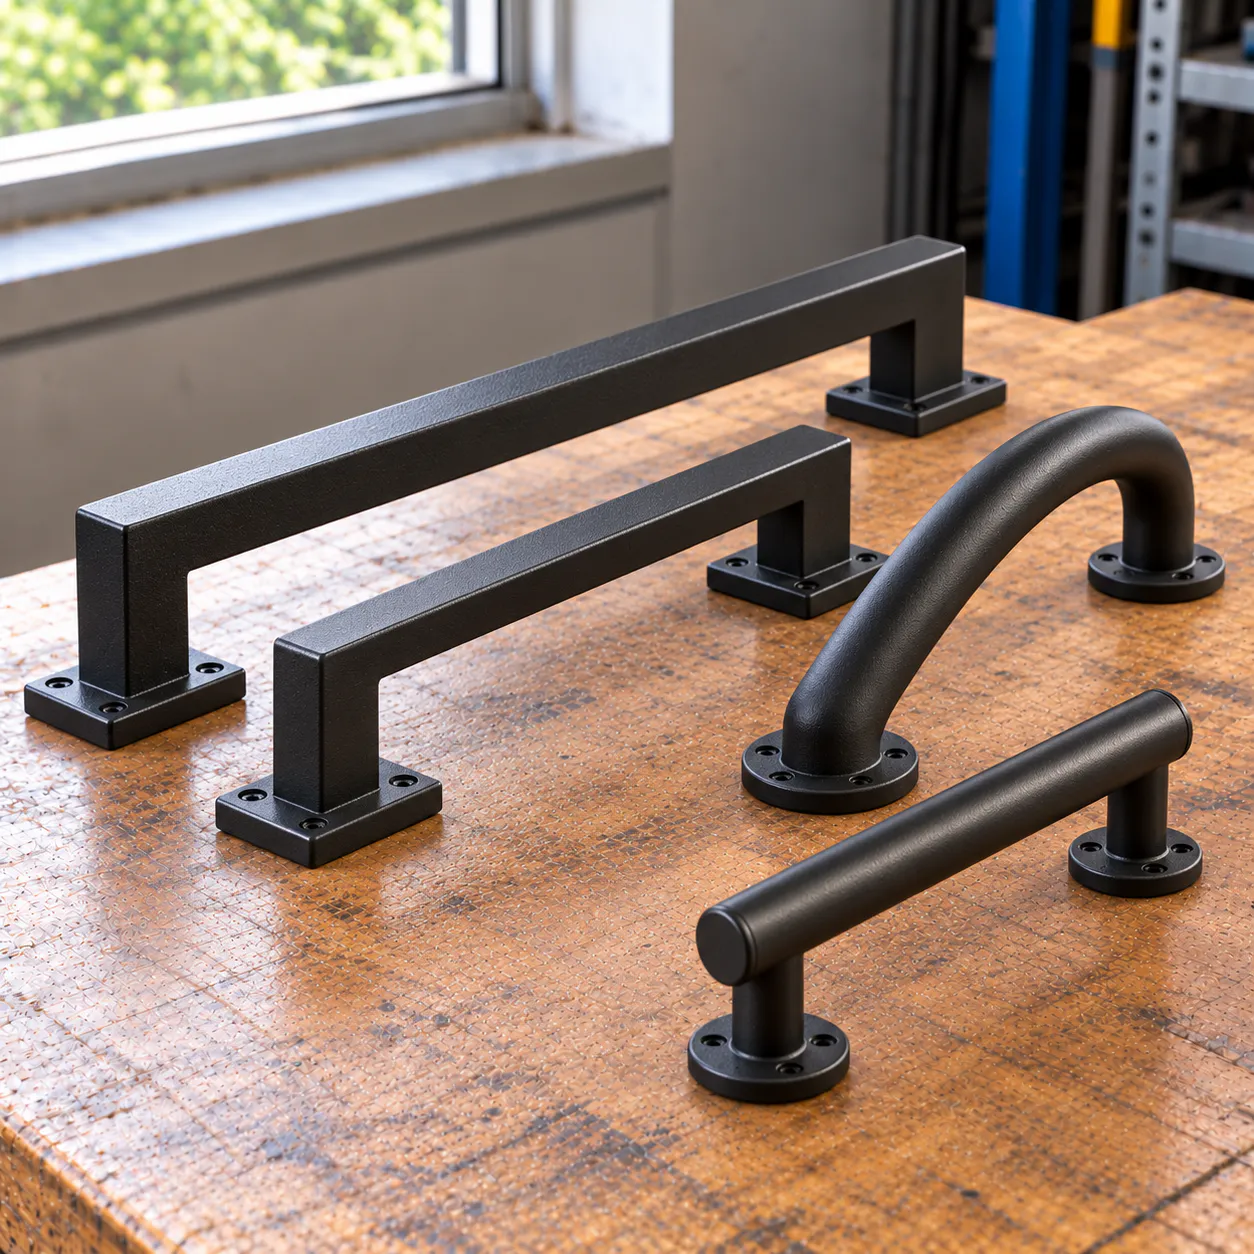
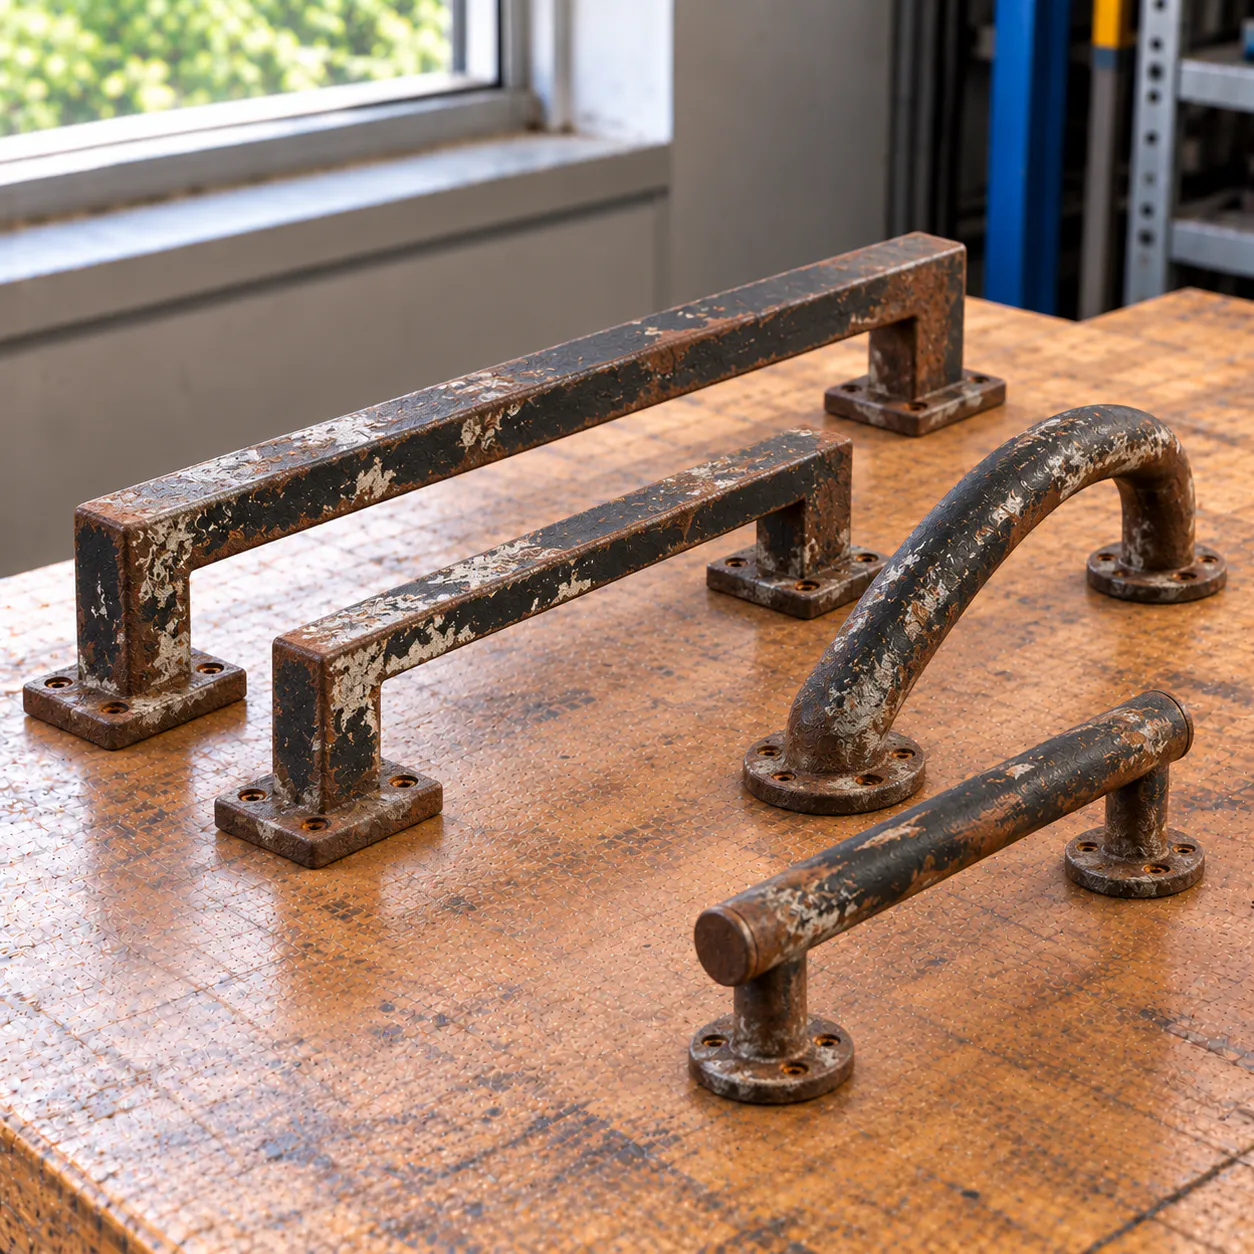 Before
Years of rust, peeling paint and surface corrosion. Stripped down to bare metal, prepared and refinished with a durable matte black coating for a clean, long-lasting finish.
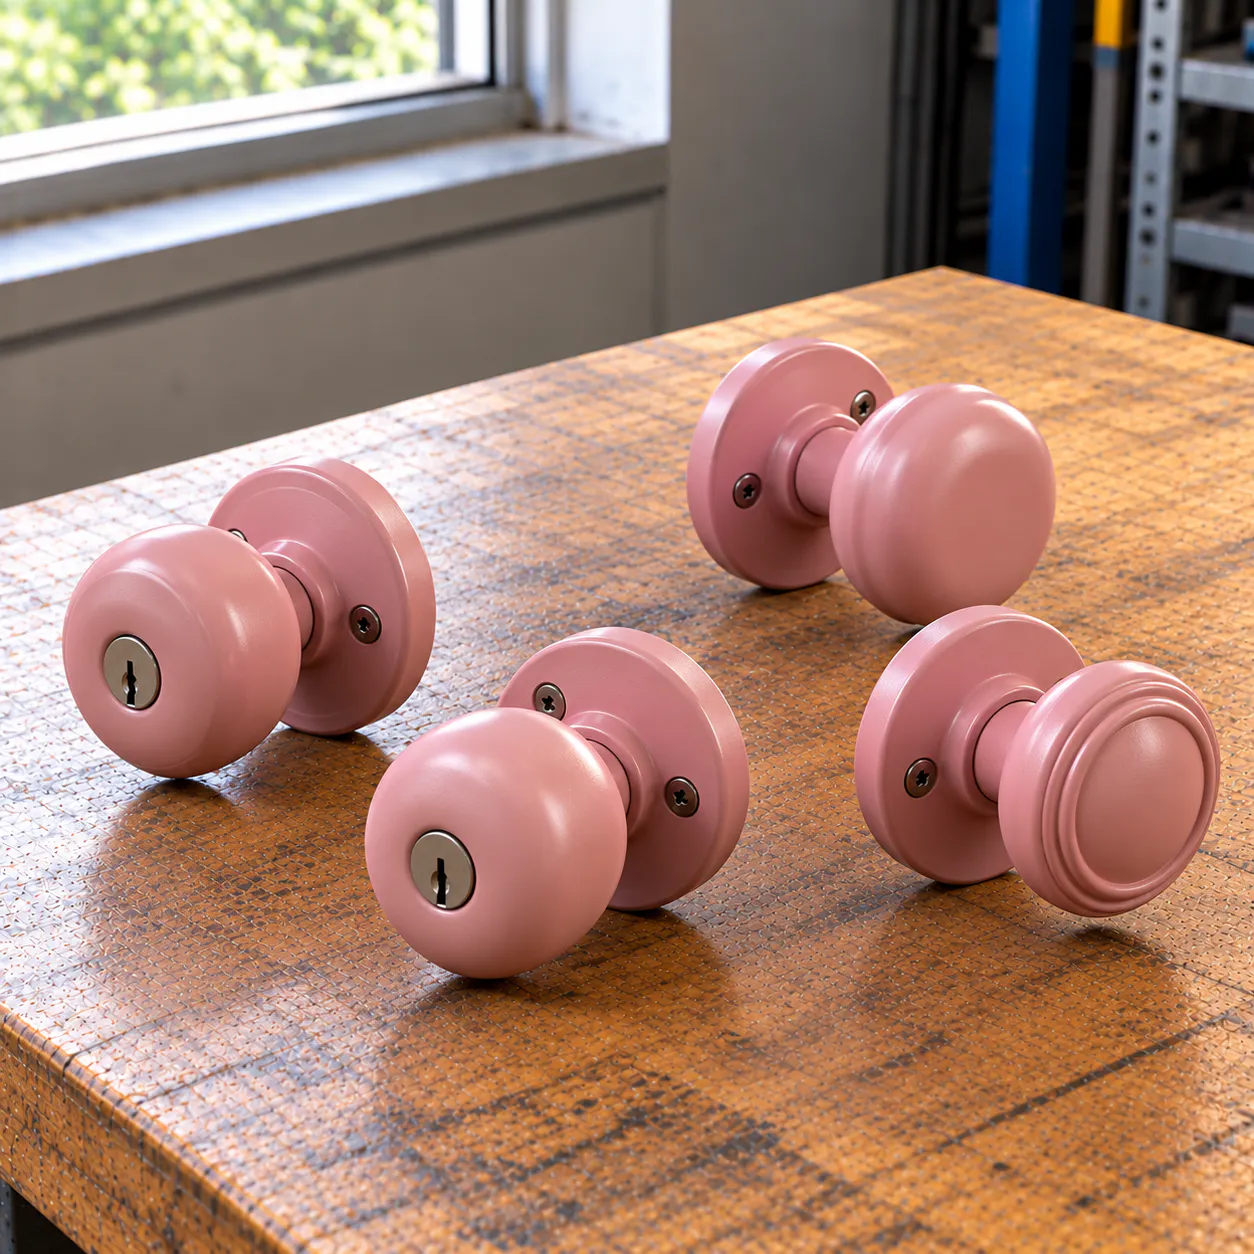
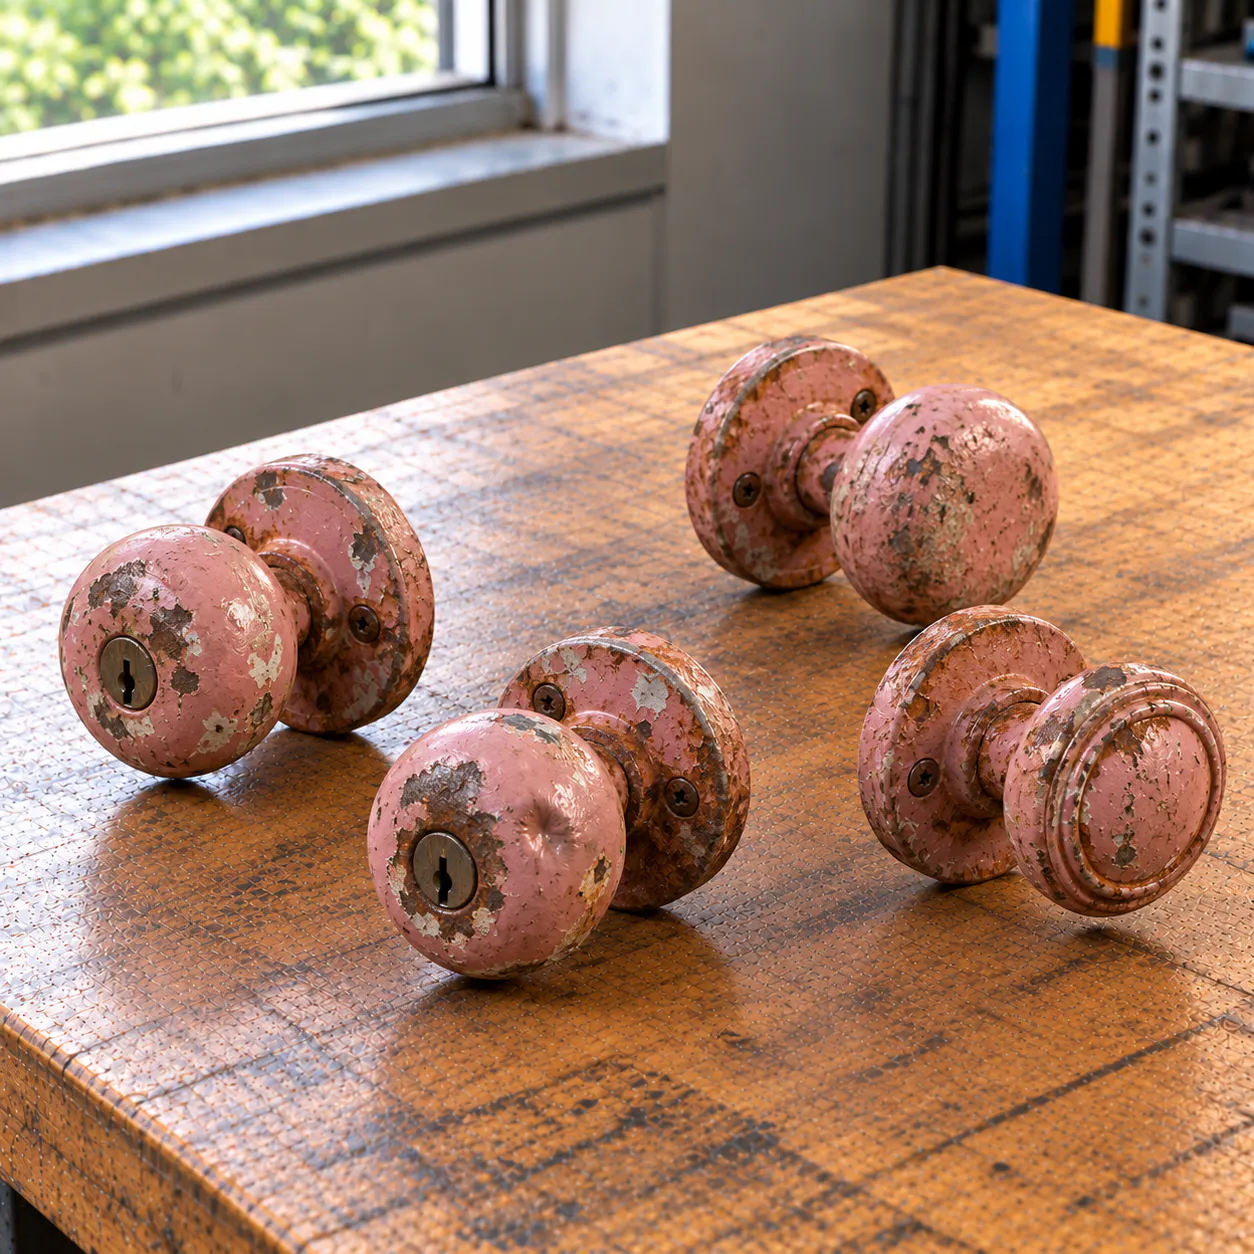 Before
Years of chipped paint, rust and worn finishes. Stripped, repaired and refinished in a soft pink coating to restore the original charm and give each door knob a fresh, durable finish.
Big order or a single knob, same care.
Homeowners send us one faucet. Companies in and out of state send production runs of hundreds or thousands of parts. Both get a written quote and the same inspection before anything ships back.
Powder only bonds to metal that can carry a static charge and survive the cure, and each metal asks for its own cleaning and pretreatment.
The most common metal we coat. Rust and scale are blasted away, then the surface is pretreated so the powder grips and resists creeping corrosion at edges and holes.
Light and naturally corrosion resistant, but it needs a dedicated pretreatment to hold powder long term. Castings are preheated first so trapped gases do not blister the finish.
Porous metal that holds oil and air. We bake it out before coating to drive out what is trapped inside, which is the step that keeps pinholes out of the final color.
Coated when you want color on a part that already resists rust. The smooth surface gets a light blast for profile so the powder has something to grab.
Can be powder coated with the right prep. The zinc layer is cleaned, lightly profiled and preheated to limit outgassing, giving two layers of protection in one part.
Polished or freshly plated parts can be sealed under clear powder. It is where our plating and powder work meet, and few powder shops can offer both.
We run all three kinds of work, so we have no reason to push one over the others. Here is how they compare when you are deciding on a finish.
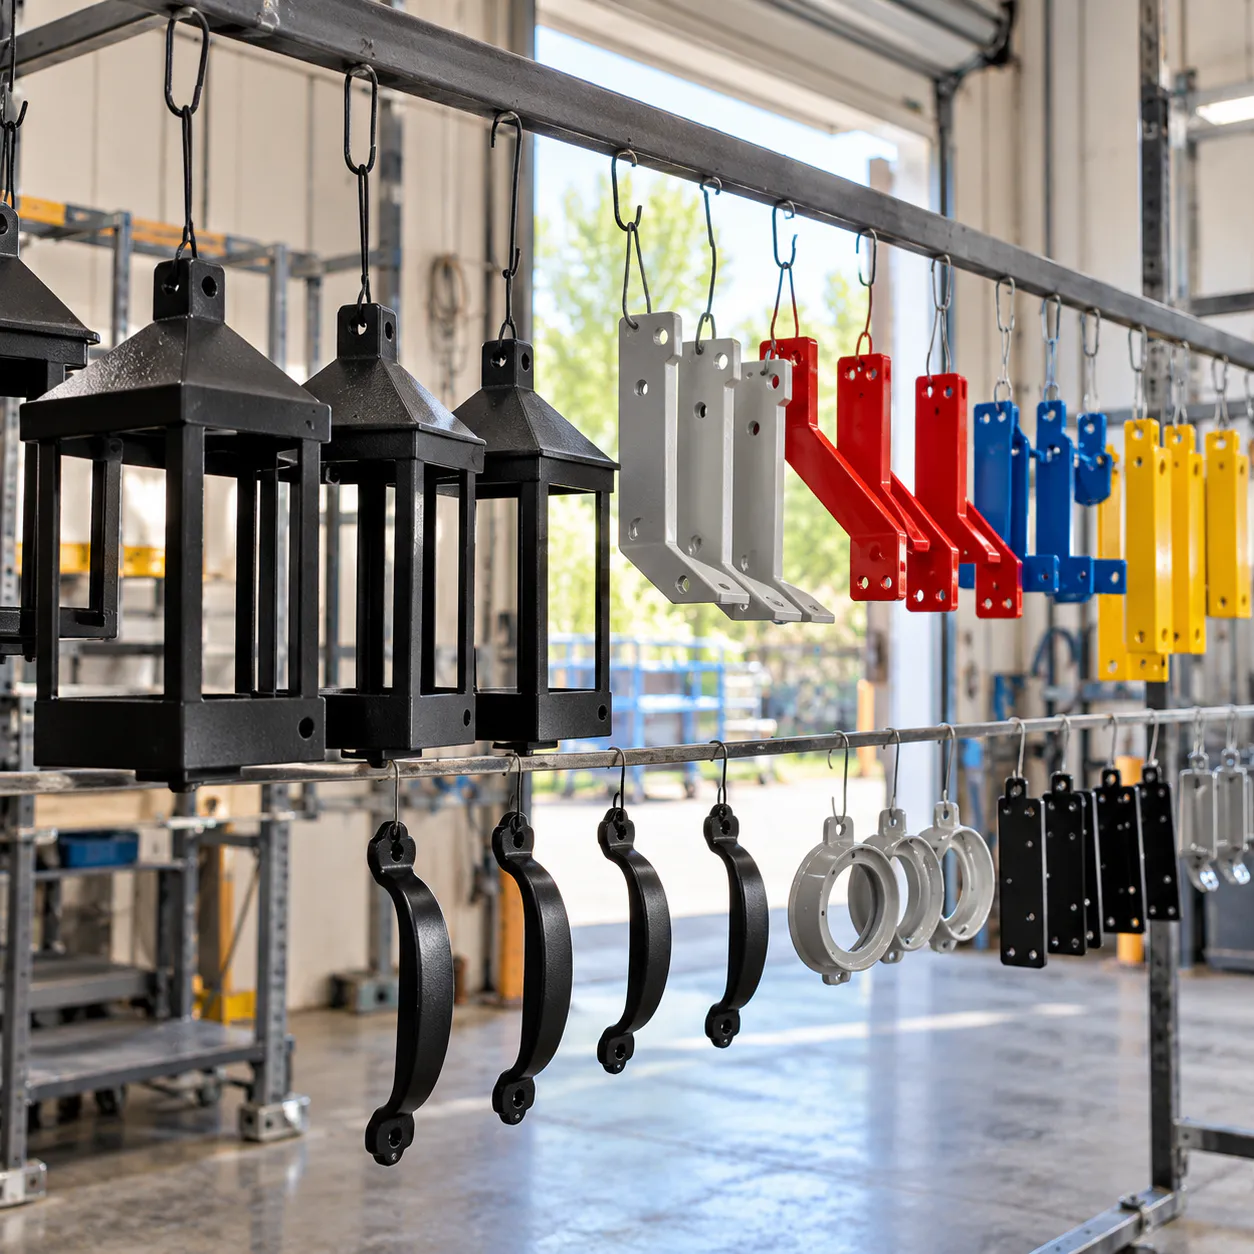
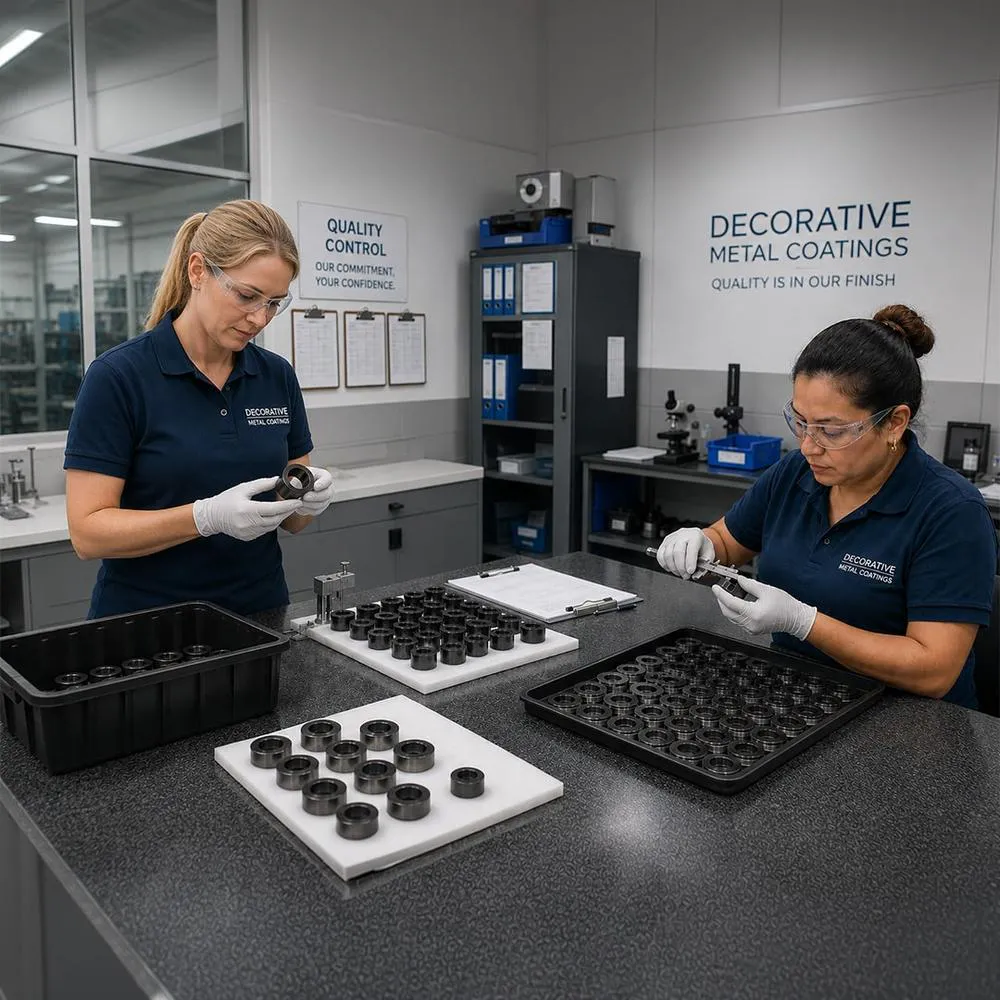
We started as a plating shop in 1989 and added powder coating so our clients could get color and metal finishes from one place. The same attention to prep that our plating work is known for goes into every powder coated part.
Send a photo of your parts and receive a no obligation quote within 24 hours.
Every part leaves our shop backed by our craftsmanship guarantee. If you are not satisfied, we make it right.
A single bracket or a box of production parts, shipped to us from any state and returned insured.
Most projects are completed within 3 to 5 weeks. Expedited Orders: 5 to 7 business days. Contact us for availability.
Applications include hardware, lighting, electronic enclosures, furniture components, marine fittings, tools, equipment parts, prototypes, casino fixtures and hospitality hardware. Suitability is assessed part by part.
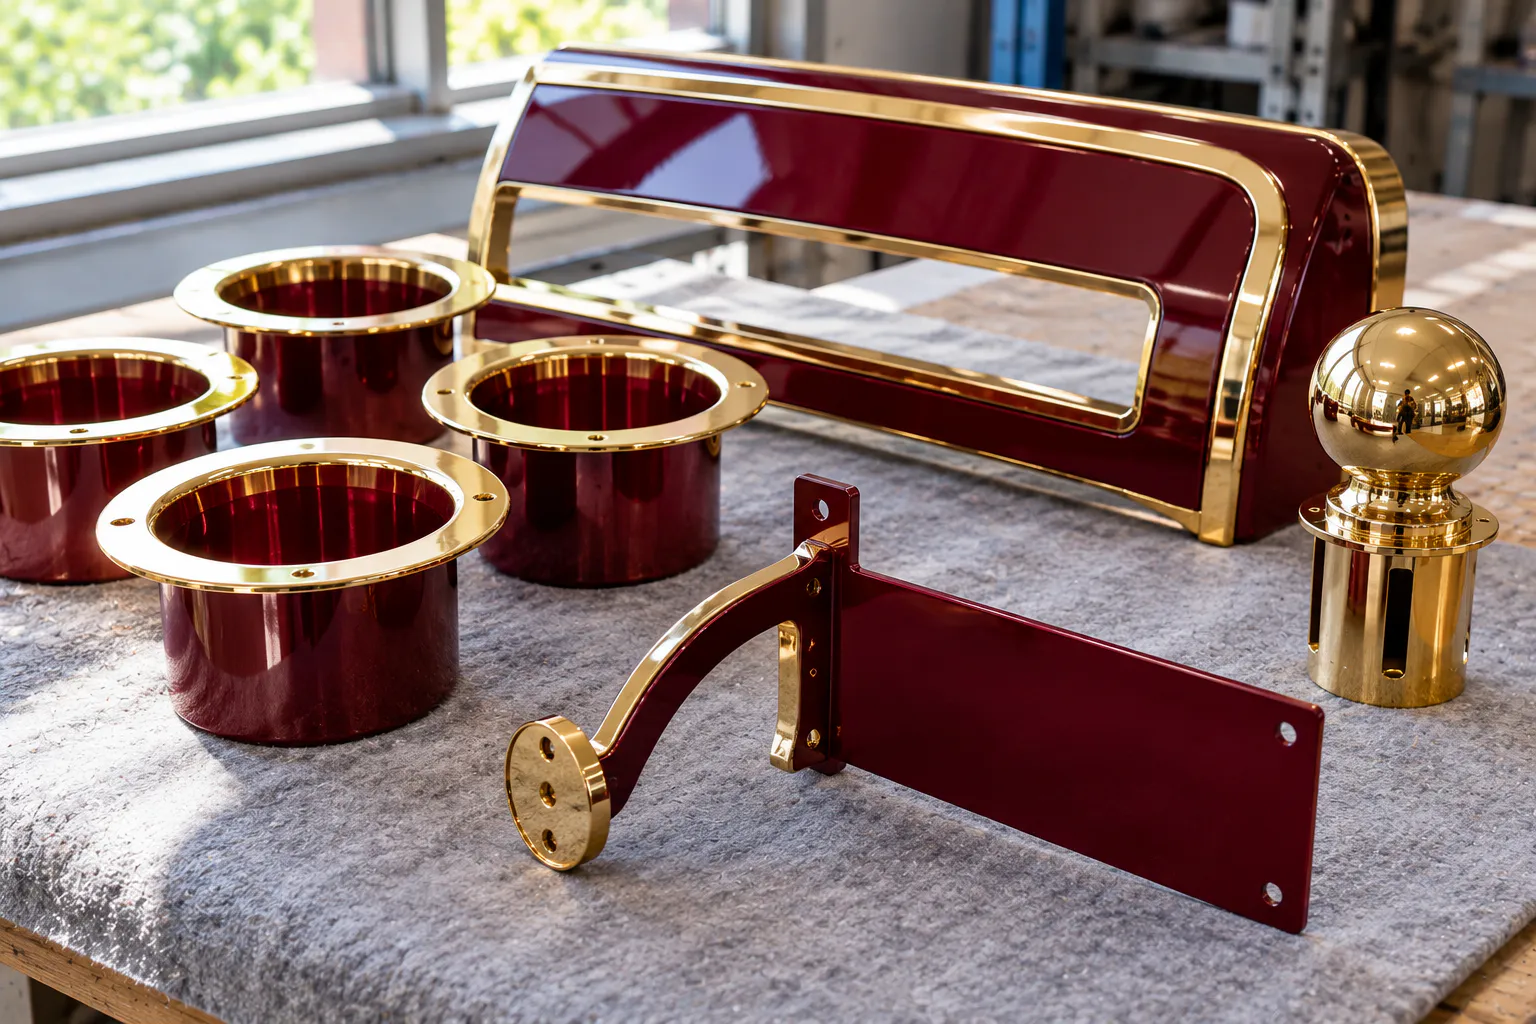
Cup holders, slot cabinet trim, sign brackets, stanchion tops and chair hardware in colors matched to the property. Trusted by casino resorts across North County San Diego to stand up to constant handling and cleaning.
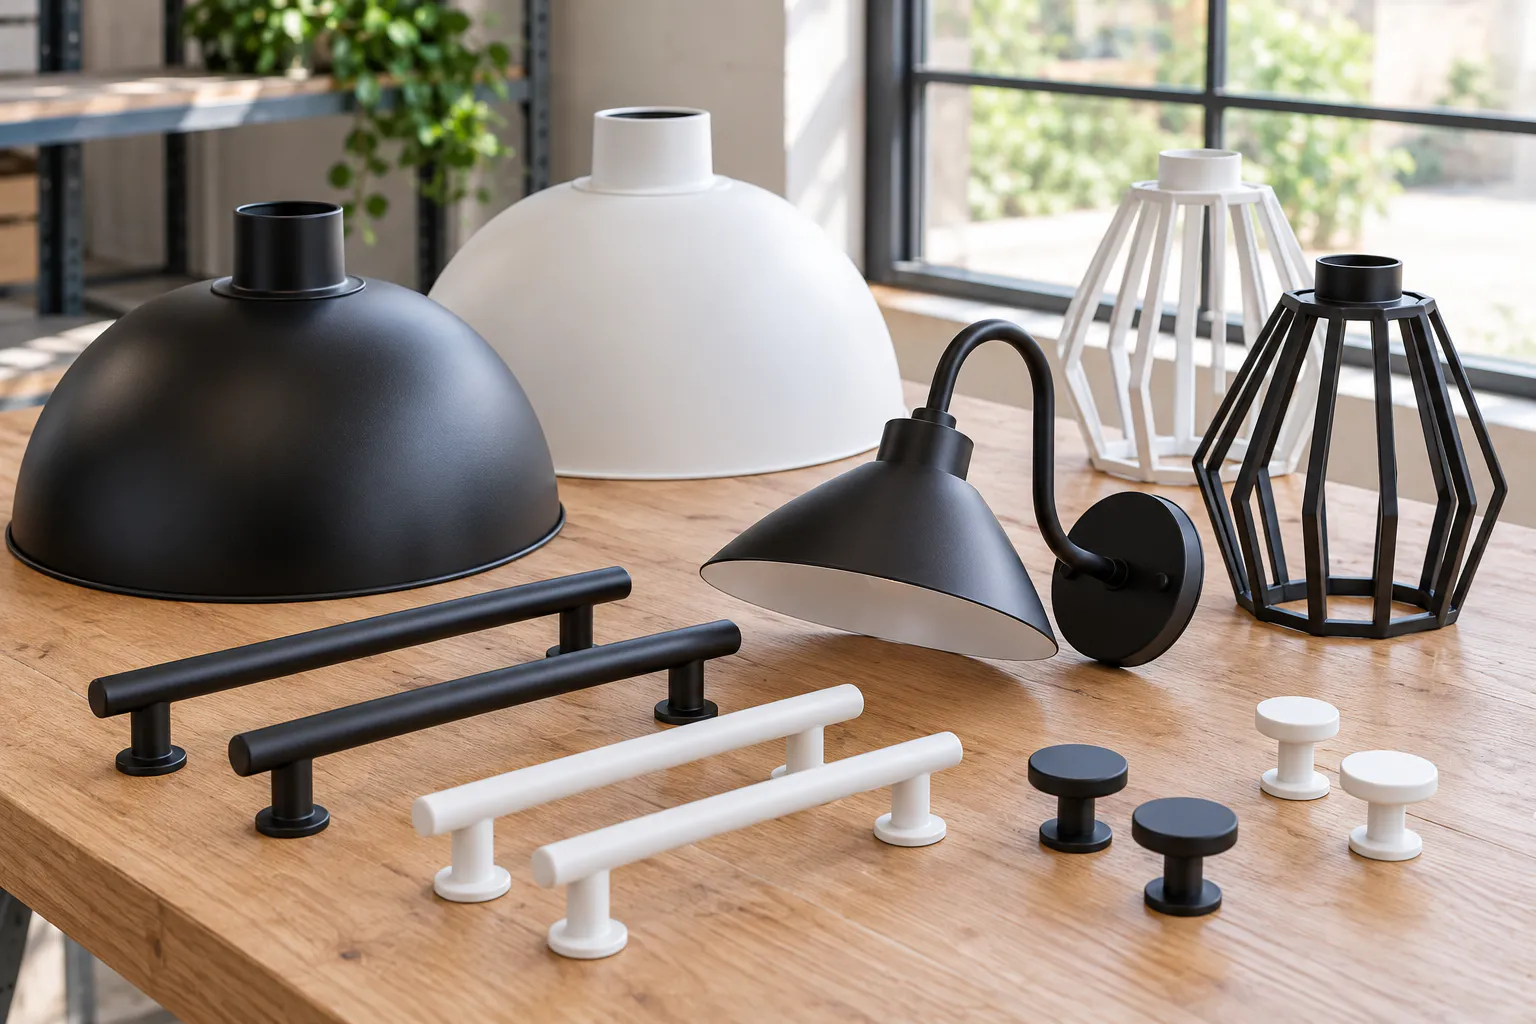
Sconces, pendant shades, lantern bodies, door pulls and hinges coated to match across an entire project.
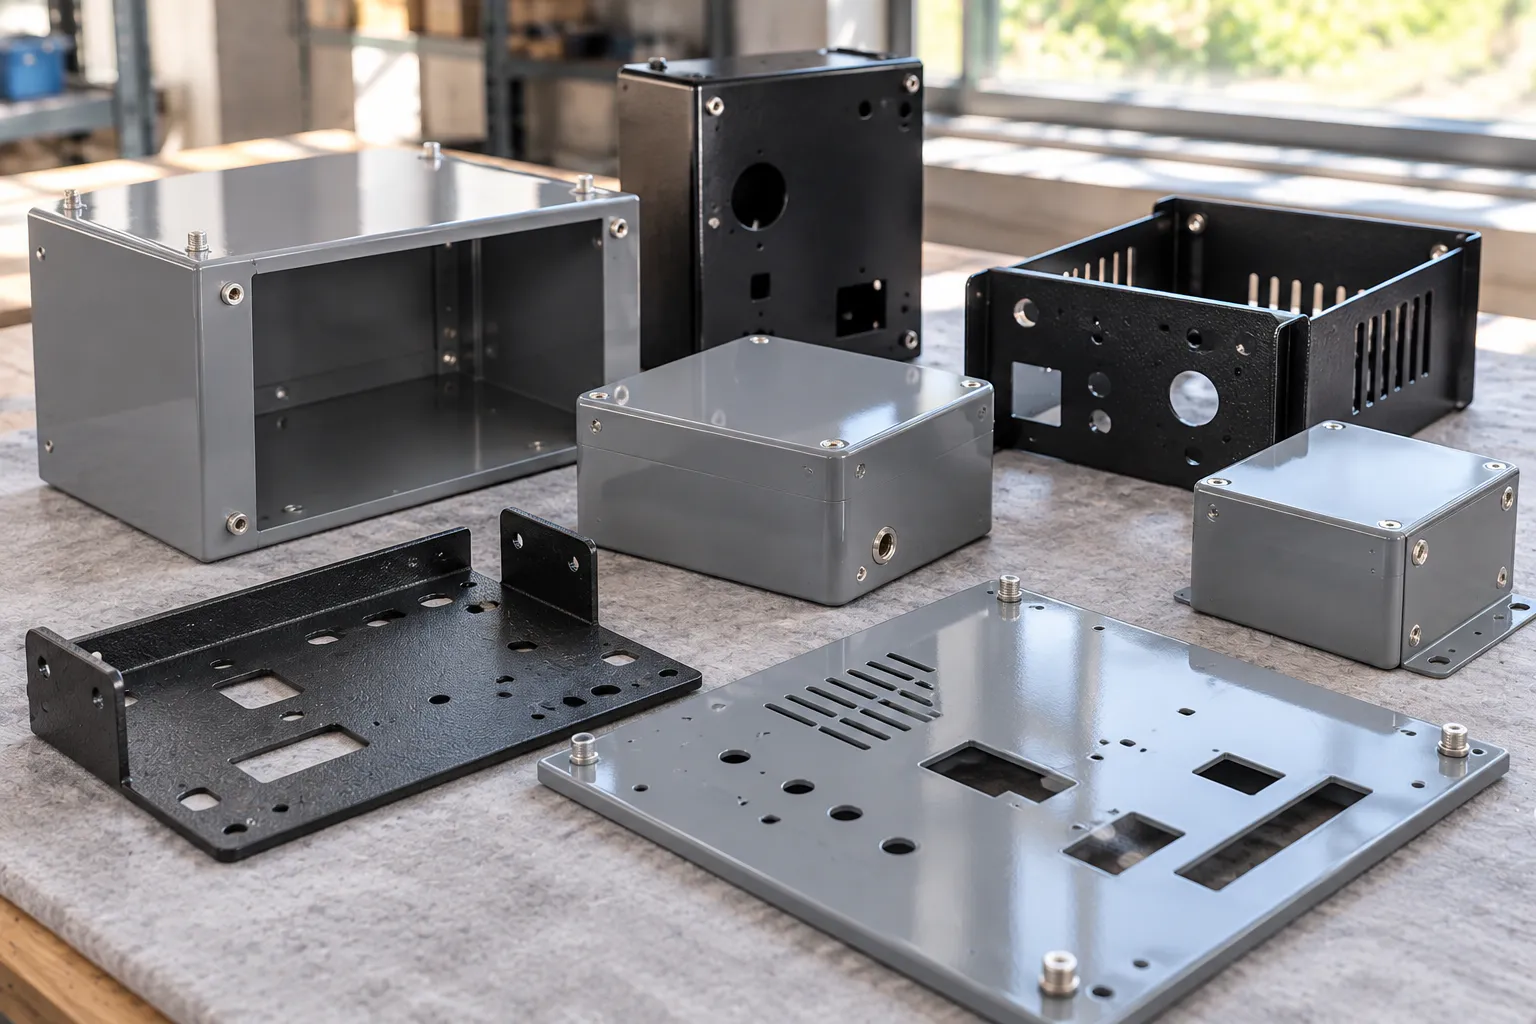
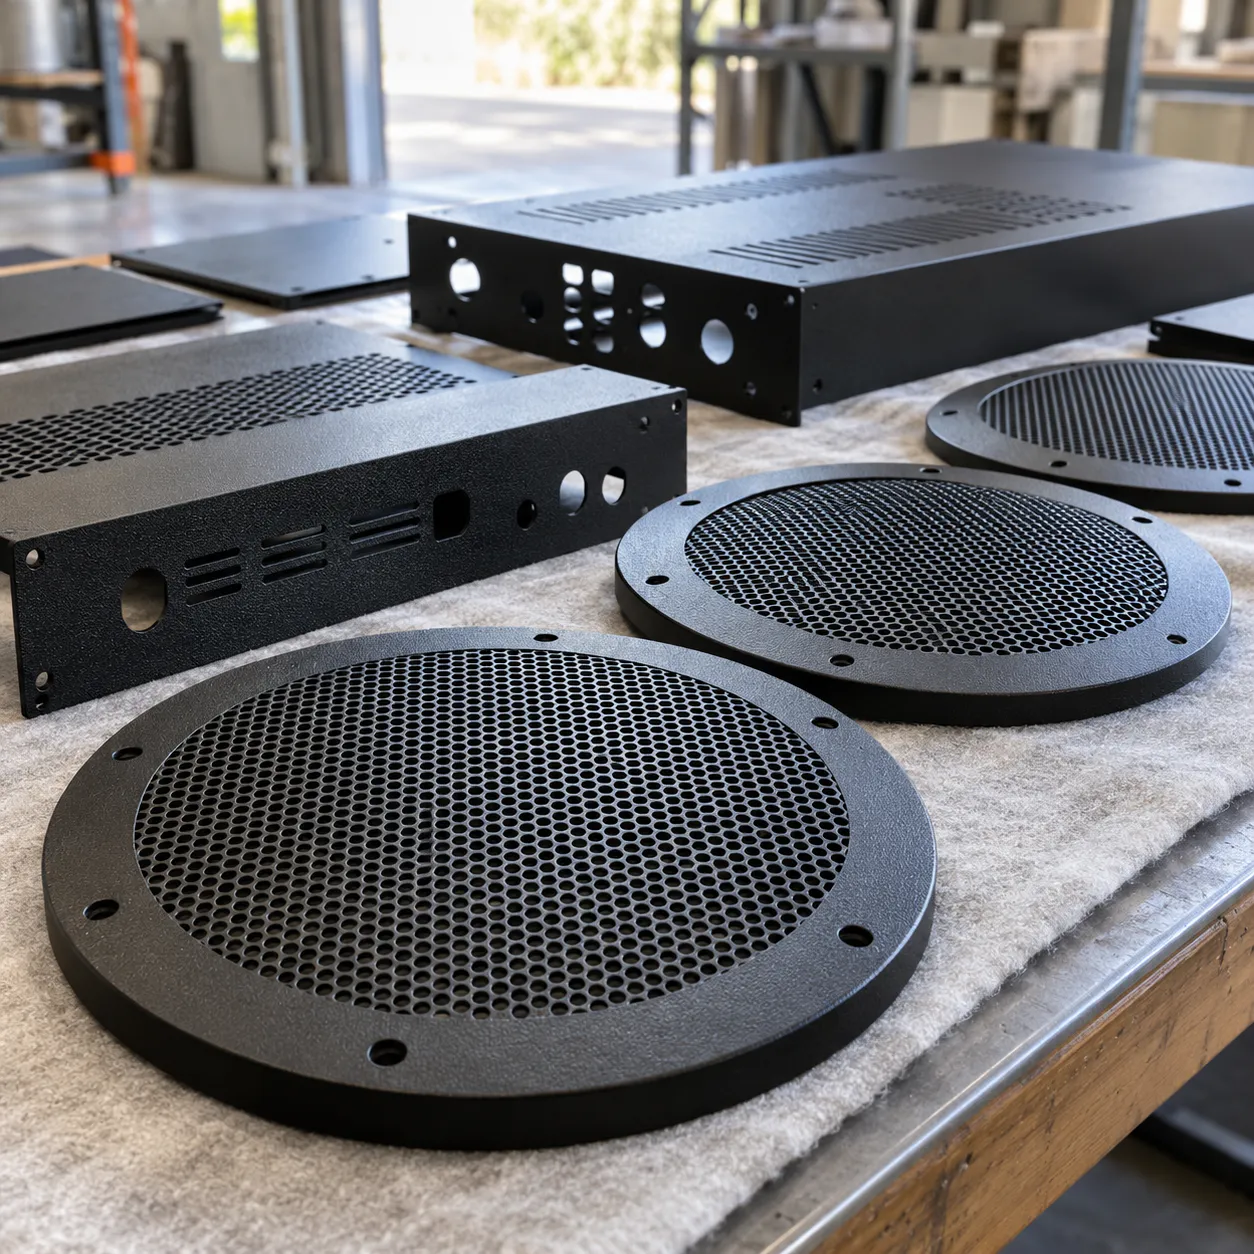
Housings, chassis panels and control boxes with ground points, threads and gasket channels masked.
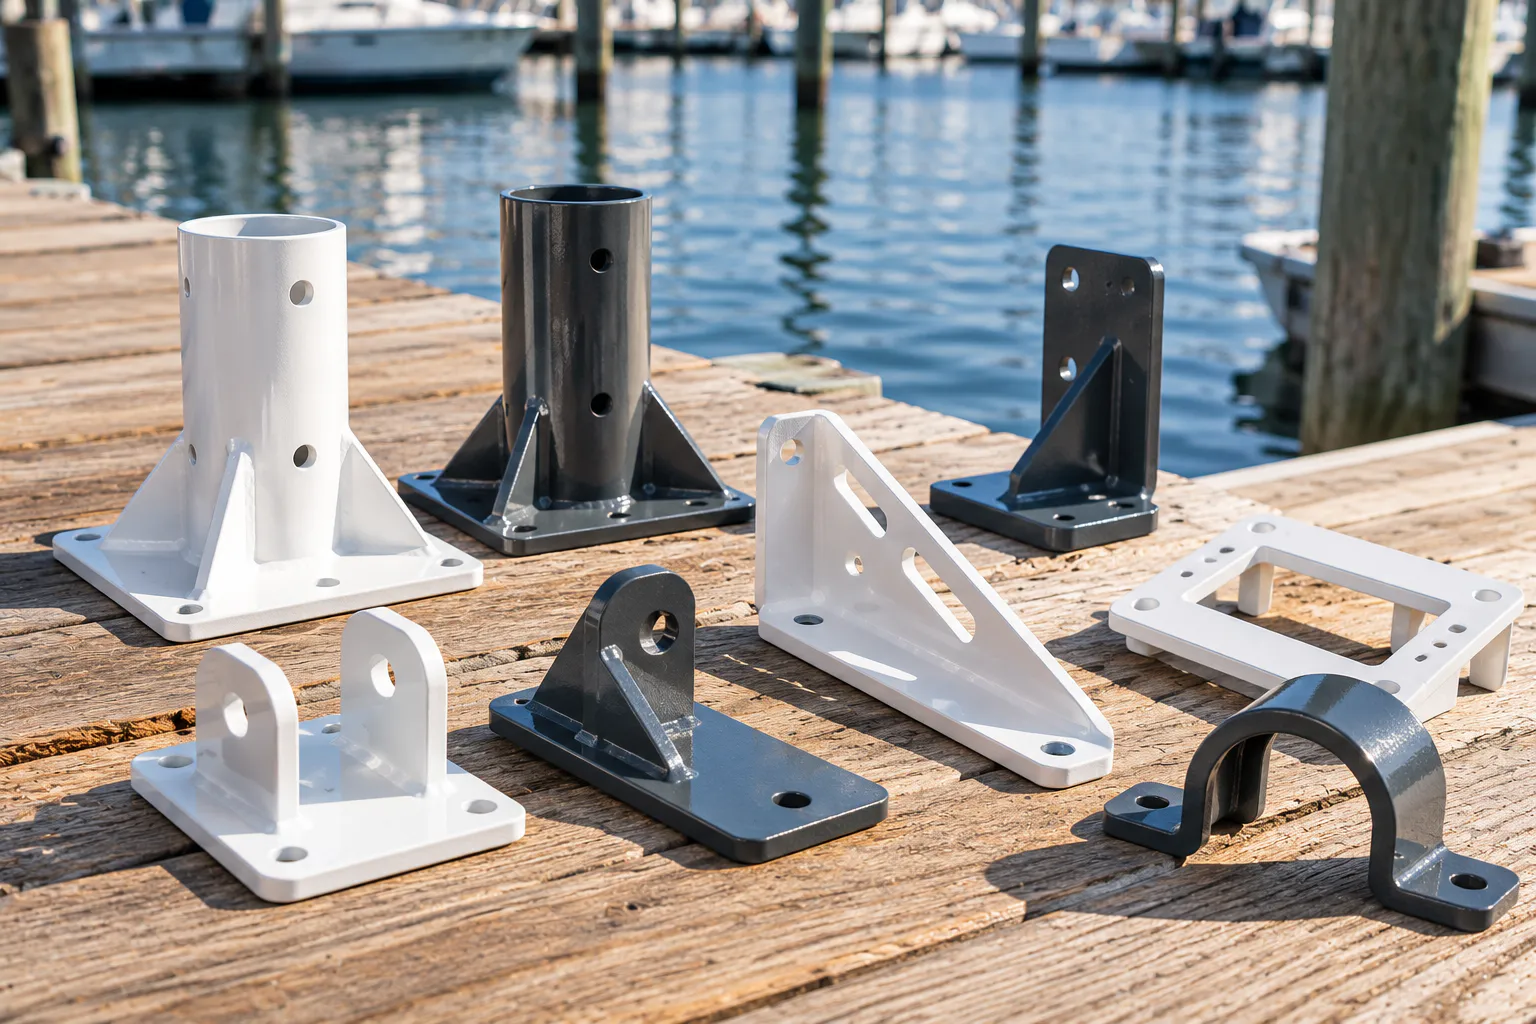
Brackets, mounts and fittings coated over a primer for salt air, harbor spray and constant sun.
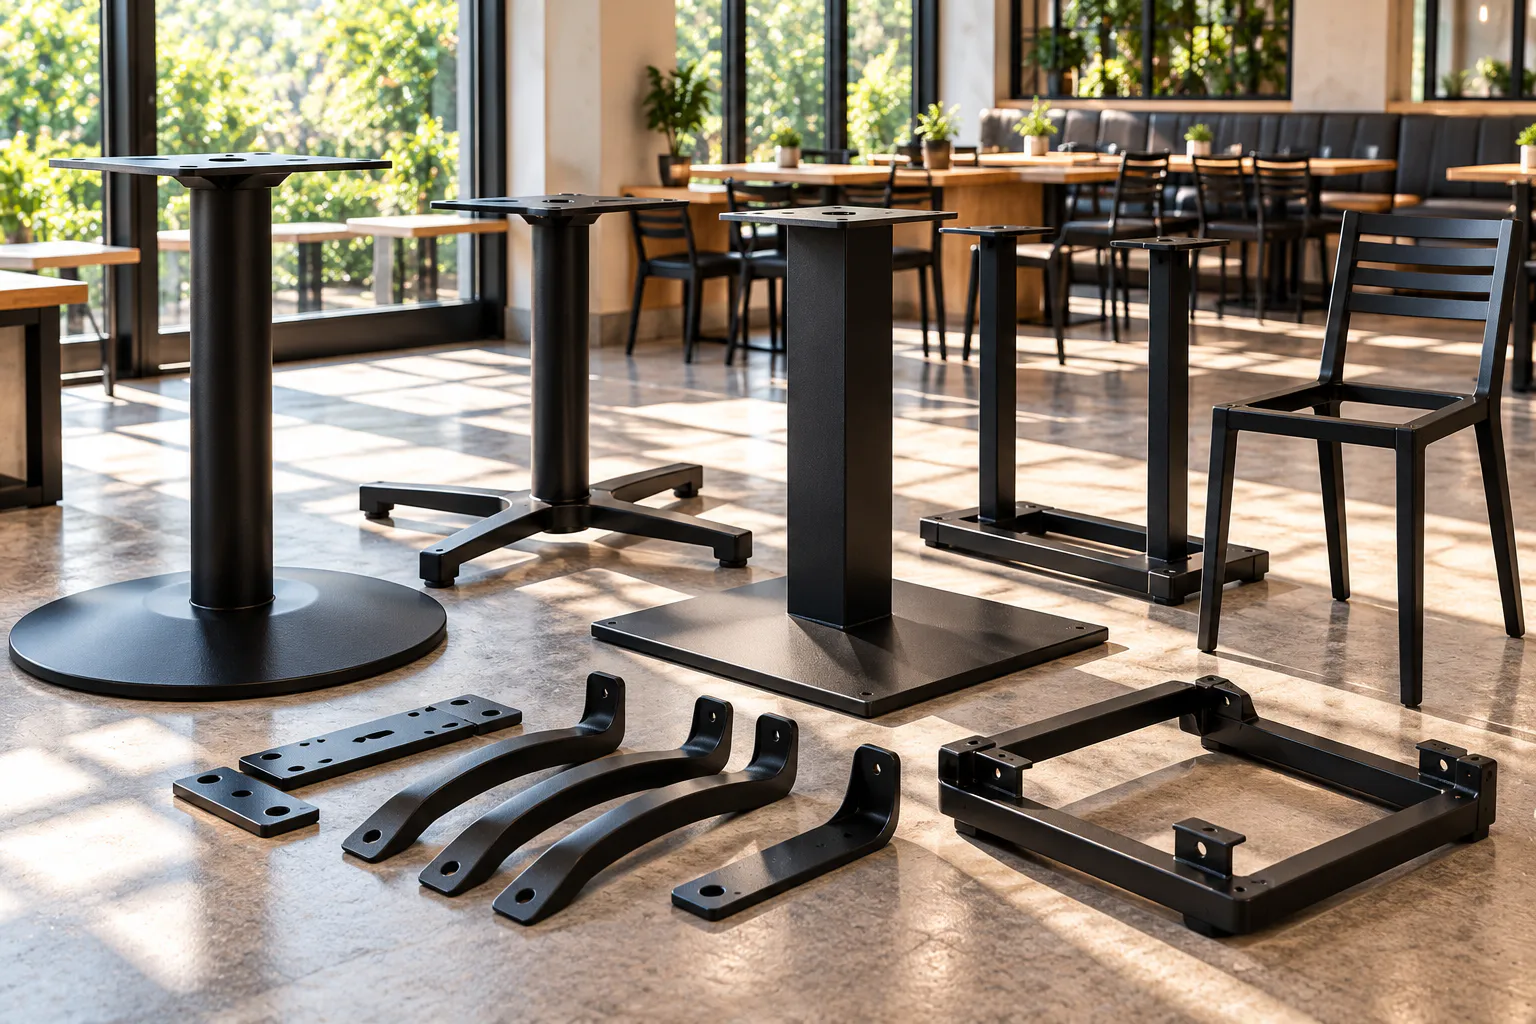
Table bases, chair components, menu holders and shelving hardware for restaurants, hotels and bars.
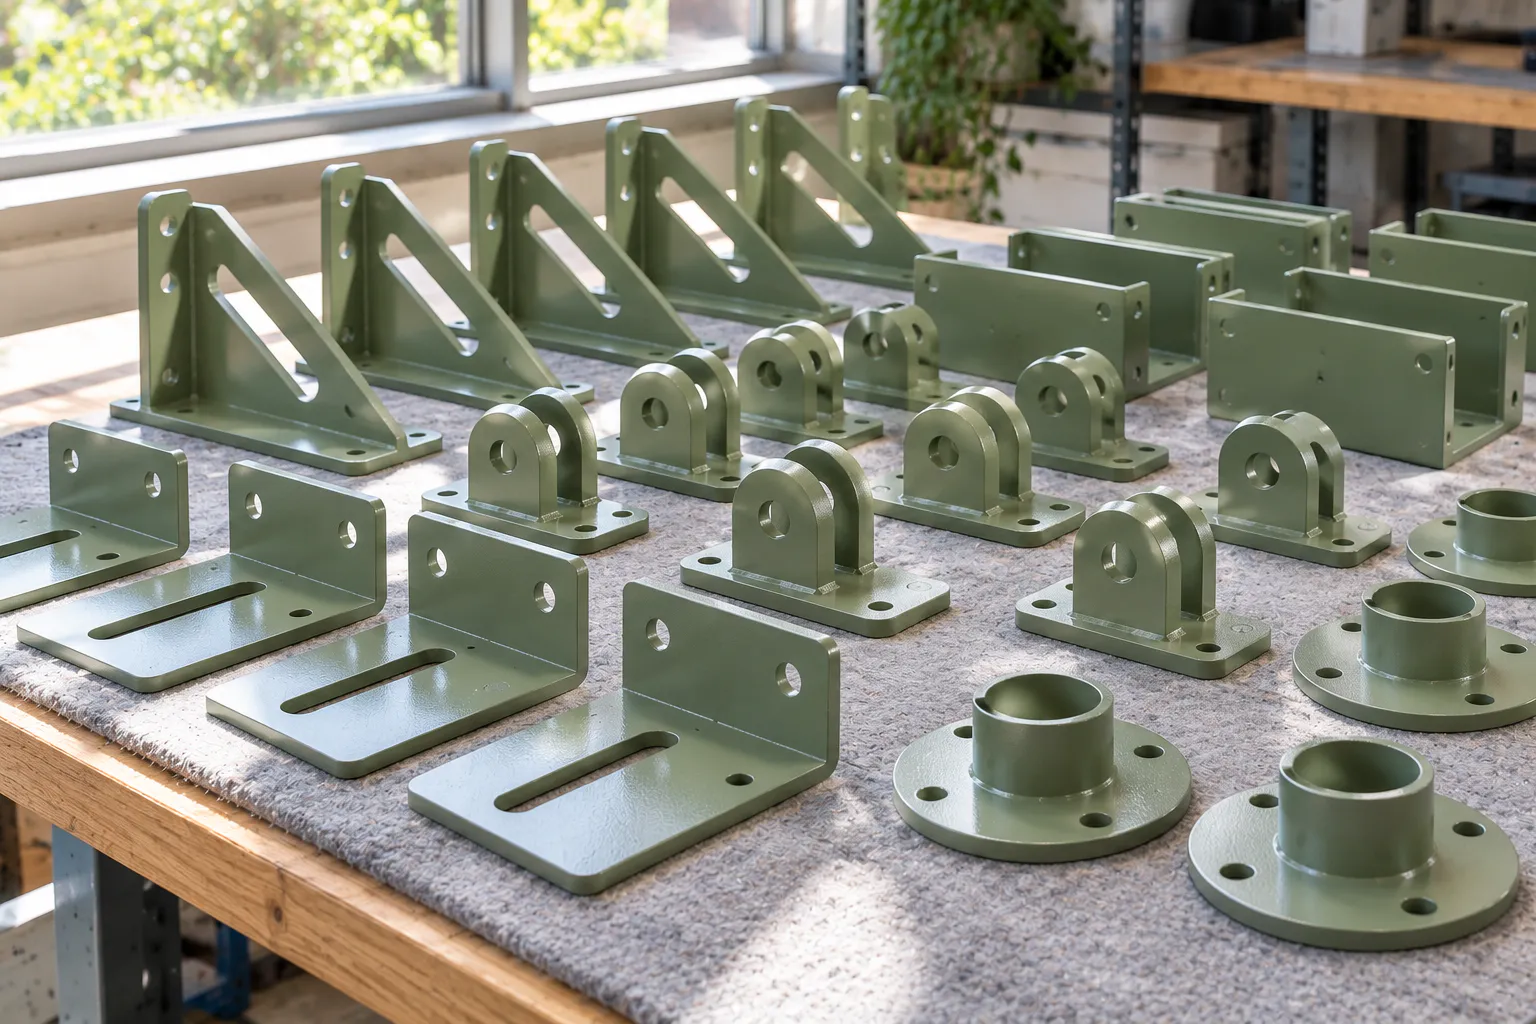
Short runs and prototype parts for designers and small brands that need a production quality finish.
From custom builders to industrial manufacturers, our clients trust us to deliver the same result every time.
Powder coating looks simple from the outside. The difference between a finish that lasts for years and one that flakes in a season comes down to the steps nobody sees.
Old paint, powder and rust are removed completely, never coated over, so the new finish bonds to the metal itself.
Every part is cleaned and pretreated after blasting, the step that keeps rust from creeping under the coating later.
Parts are cured to the powder maker schedule and checked for full coverage, even sheen and correct color.
Finished pieces are wrapped individually so they arrive without rub marks or scuffs from shipping.
Small Steps That Make a Better Finish
Powder is cured with heat, so anything on the part that is not metal has to come off first. Rubber bumpers, plastic caps, gaskets, glass, bearings, seals and electrical parts will not survive the cure. Taking them off before you ship saves labor on our end and keeps those pieces safe.
Think about where the part touches other parts. Threads, bores, bearing seats, ground points and sliding surfaces usually need to stay bare, because even a thin layer of powder can stop a bolt from turning or a lid from closing. Mark those areas with tape or a quick photo note and we will mask or plug them.
Tell us about any repairs. Body filler, epoxy and glue break down in the cure and leave bubbles behind, while welded and brazed areas often need extra blasting. Old parts that lived in oil, such as tool and machine parts, may need an extra bake out before coating.
Finally, send everything that needs to match in the same order. Powder colors vary slightly from batch to batch, so a full set coated together will always line up better than pieces done months apart.
Routine cleaning helps preserve the selected finish
Clean with a soft cloth, warm water and mild dish soap, then dry the surface. Avoid abrasive pads, solvents and paint thinners. On tool housings and equipment components, pay attention to edges and contact points where handling or installation can concentrate wear.
For coastal use, rinse salt residue with fresh water. If a deep chip exposes the substrate, address it promptly. Do not use harsh abrasives to remove stubborn marks.
Near the coast, salt is the main enemy. Rinse outdoor and marine parts with fresh water every few weeks and after storms. A light coat of non abrasive spray wax a couple of times a year adds another layer that sheds water and salt.
If a part takes a deep hit and the coating is broken down to metal, seal the spot quickly with touch up paint so moisture cannot spread underneath. For a full repair, we can strip the part and coat it again to match the rest of the set.
Powder Coating Gallery
Gloss, satin, matte, textured and metallic powder coat on hardware, brackets, enclosures, lighting and small production runs.
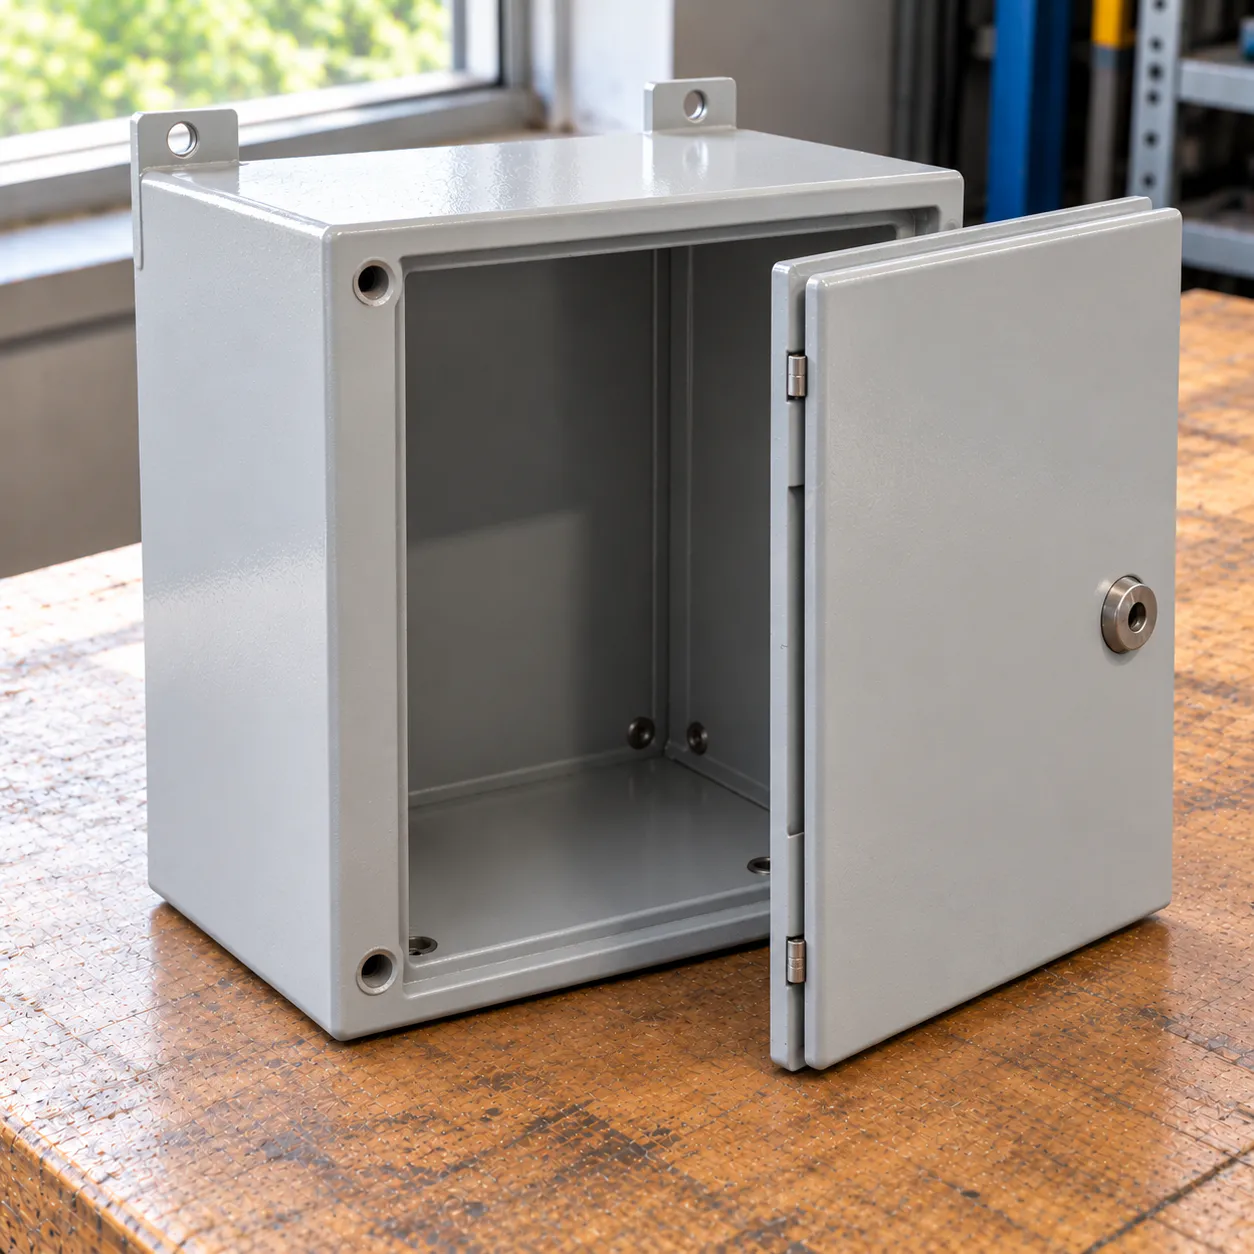
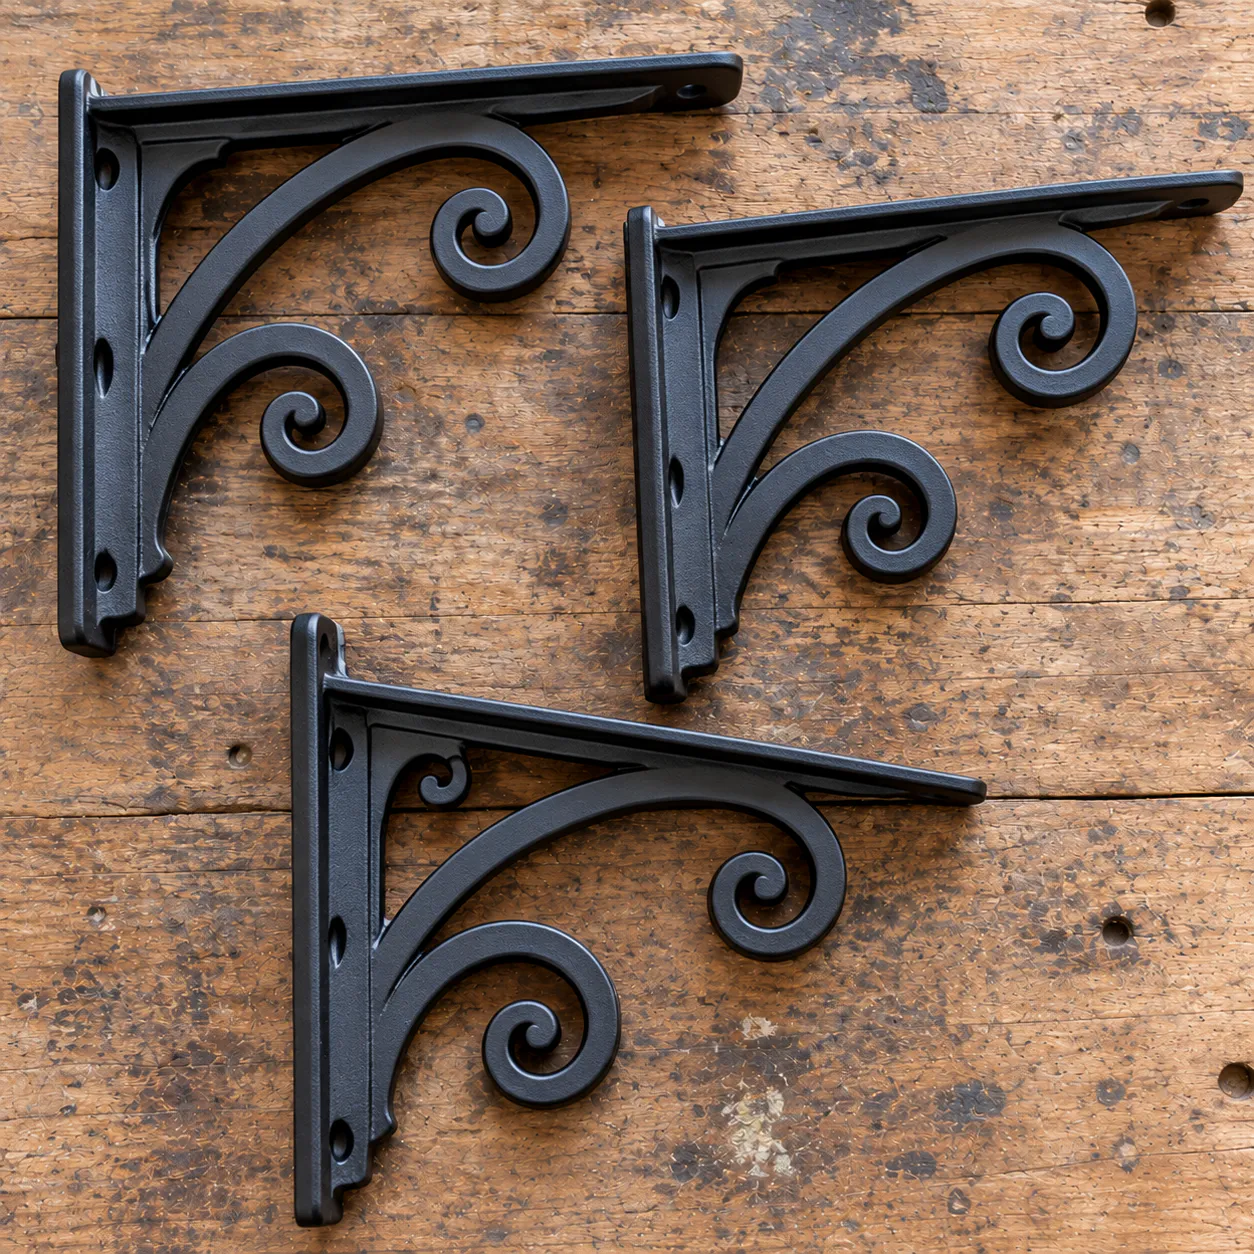
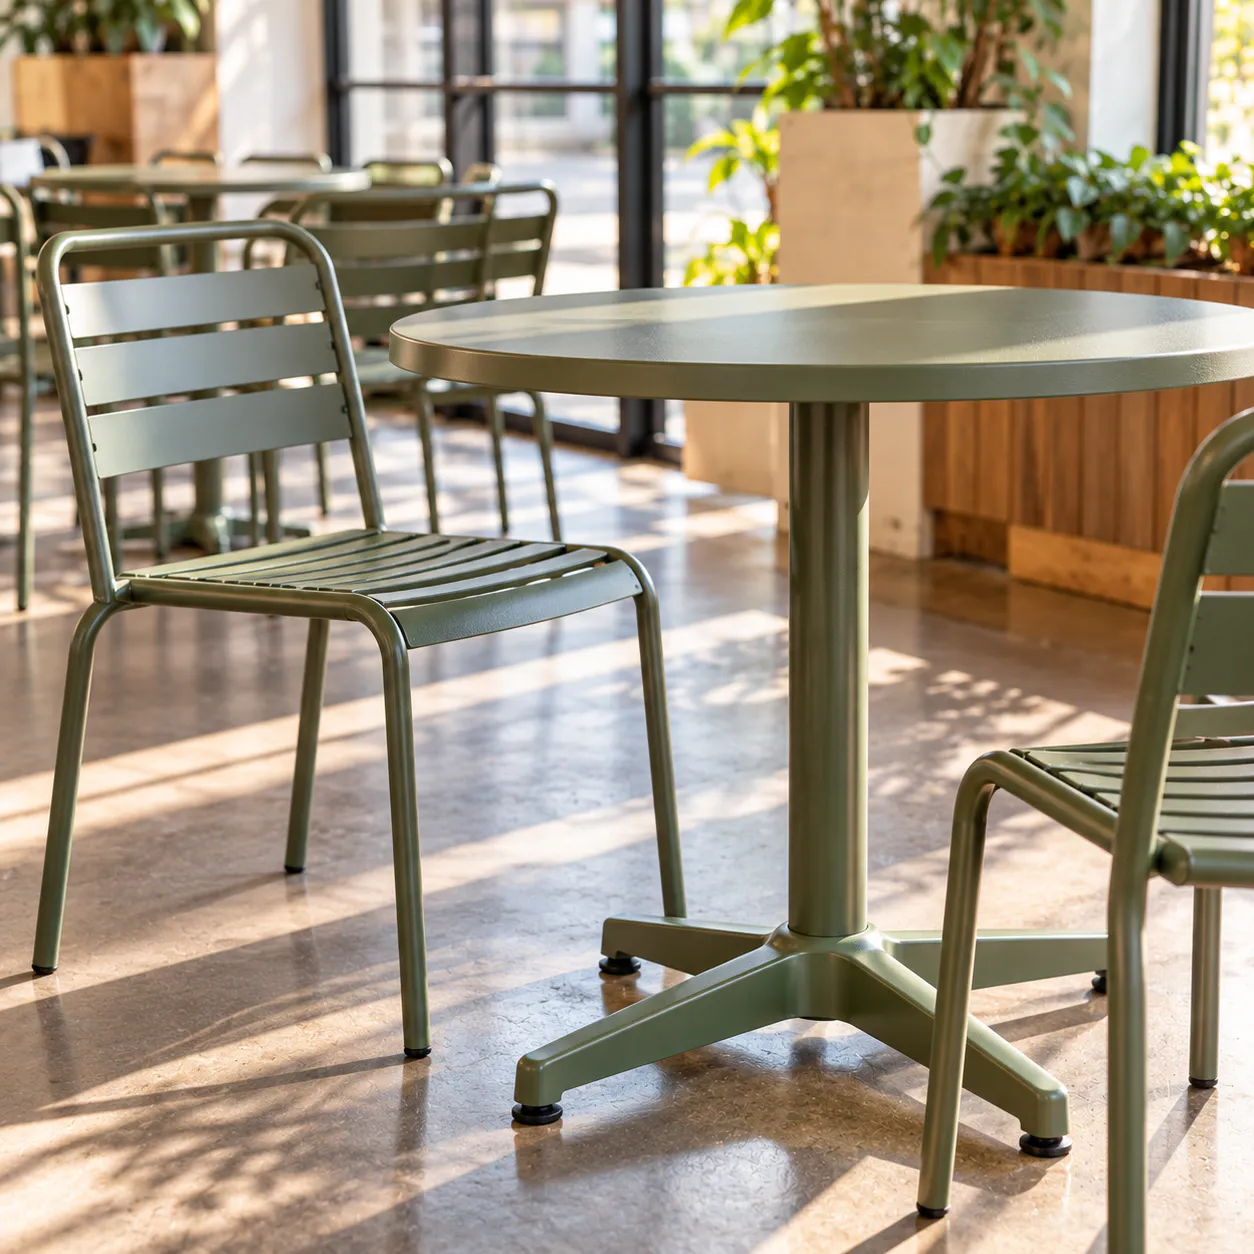
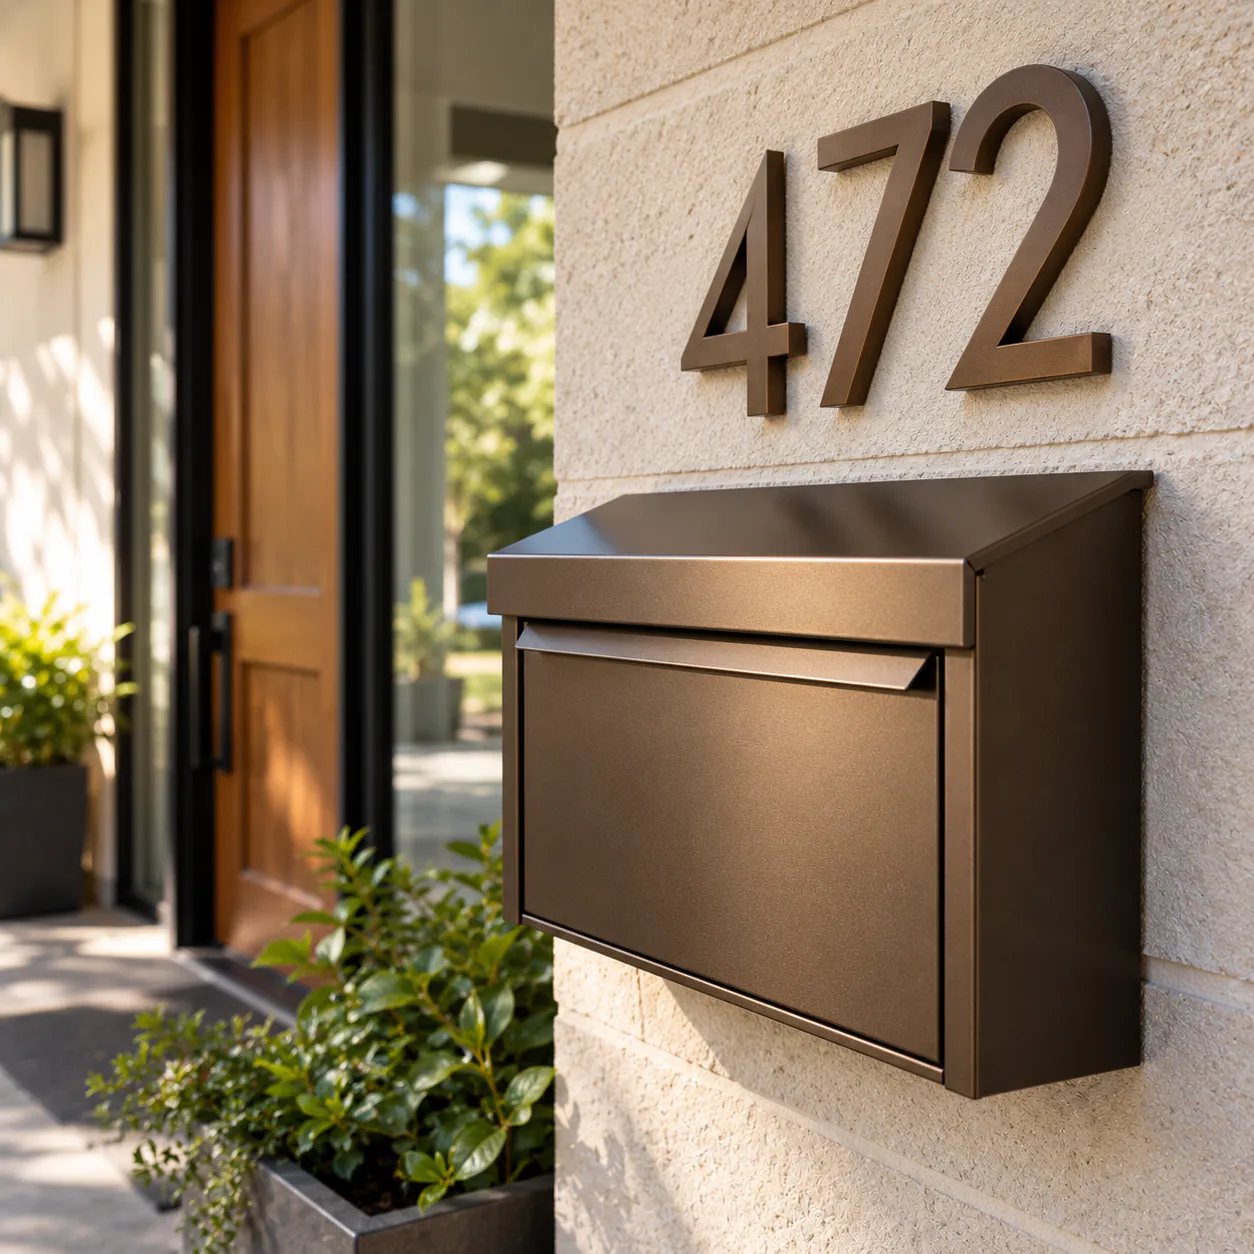
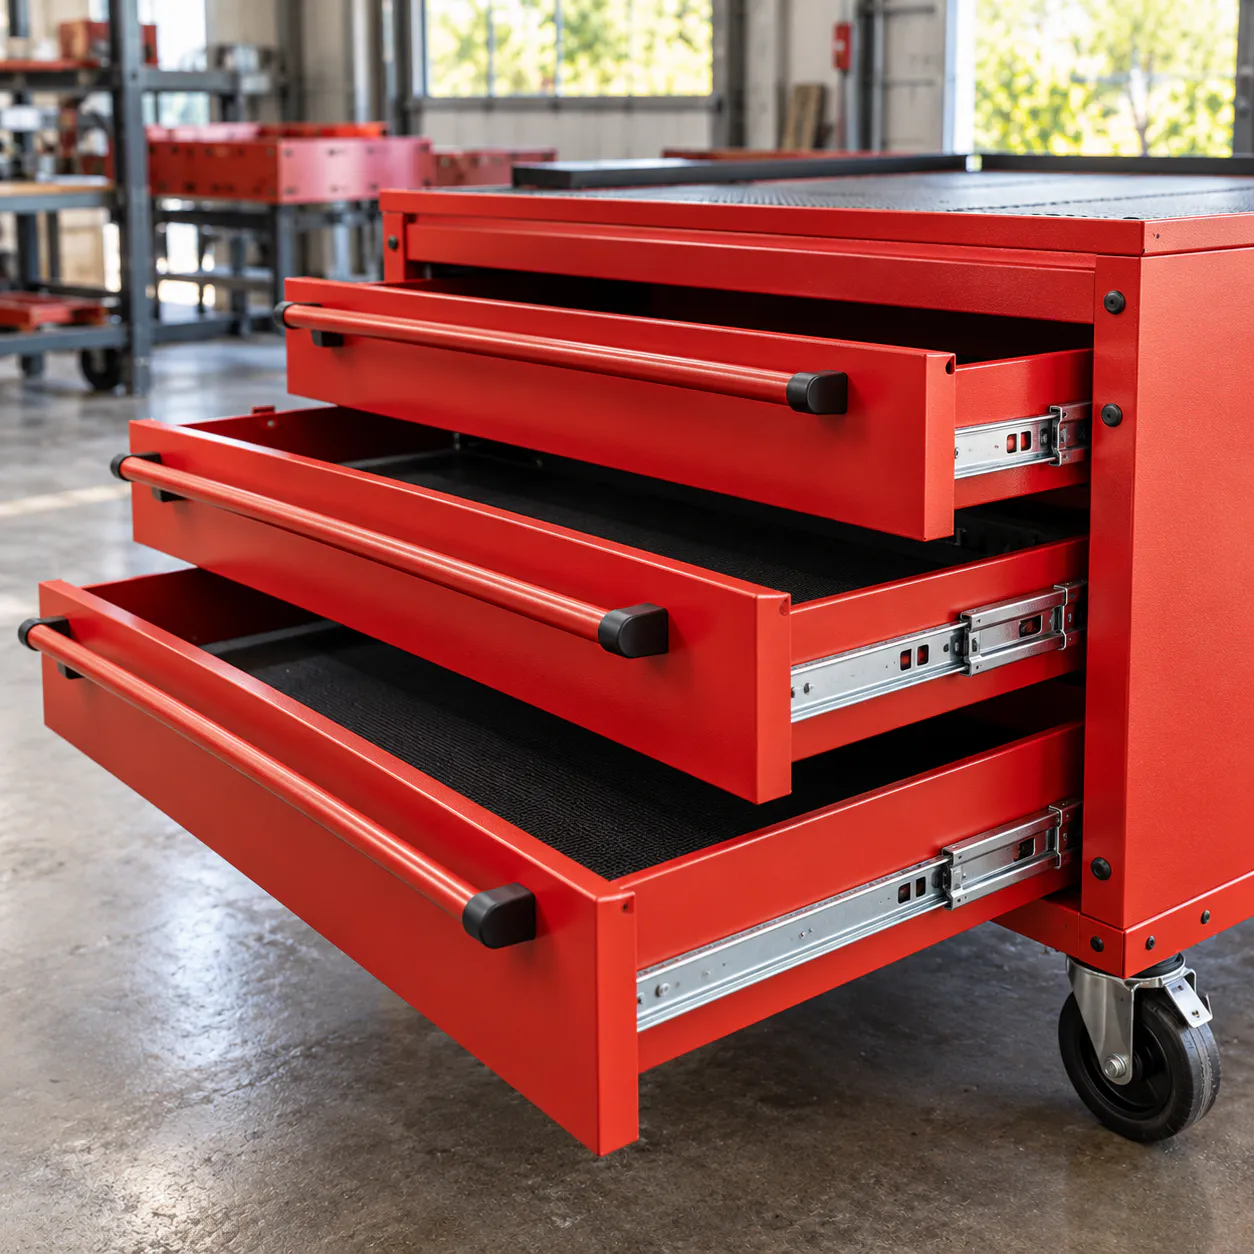
Before shipping from Indian Wells, remove rubber, plastic, glass, gaskets, bearings, seals and electrical parts that cannot go through the coating process. Mark bare areas, wait for the approved quote number, wrap components individually, insure the shipment and provide tracking.
Send photos, quantities and the color you want. We reply with a written quote, prep notes and lead time. Please wait for your quote number before shipping.
Remove rubber, plastic, glass and bearings, then bag any small hardware you want returned. Wrap each part on its own with at least three inches of padding.
Declare the full value with the carrier and email us the tracking number so your parts are logged the day they arrive.
We photograph the finished parts for your approval, wrap each one in fresh packing and ship them back insured.
Every powder coat job is stripped, blasted, coated and cured in our own facility in North County San Diego.
Powder coating, plating and metal finishing in San Diego County since 1989.
DMC does not claim a powder-coating shop in Indian Wells. Eligible projects from Indian Wells and other US locations may be shipped to Oceanside after quote approval and confirmation of shipping instructions.
Other California communities represented in the service-area content include Highland, La Puente, Montclair. All powder coating is performed at the Oceanside facility.
Frequently Asked Questions
These general answers explain the information needed for a project review. Final compatibility depends on the actual part, substrate, geometry and required finish.
Steel, aluminum, cast iron, stainless steel, galvanized steel, brass, copper and some plated parts may be considered. Preparation differs by material, so provide the exact substrate when known.
Yes. Identify threads, bores, bearing seats, ground points and mating surfaces before quoting. Masking or plugging can then be evaluated for the component.
Powder coating is performed at the Oceanside, California facility, not in Indian Wells. Eligible projects may be shipped from any US state after a written quote is approved.
Remove rubber, plastic, glass, gaskets, bearings, seals and electrical components. Mark areas that must remain bare, wait for the quote number, wrap parts individually, insure the shipment and provide tracking.
Use a soft cloth, warm water and mild dish soap, then dry. Avoid solvents, thinners and abrasives. Rinse coastal parts with fresh water and promptly address deep chips.
Send us a few photos of the part from different angles, along with what it is and the finish you want. We look them over and send a written quote, usually within 24 business hours. It's free, and you're under no obligation to go ahead.
Standard orders take 3 to 5 weeks from the day your parts arrive. If you're on a deadline, ask about expedited service. When the schedule allows, we can finish in 5 to 7 business days.
Yes. Our workmanship is covered for 12 months. If something isn't right with the finish we put on, call us and we'll make it right.